

Working Principle and Features of a Stabilizer Powder Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in providing advanced pneumatic conveying solutions for stabilizer powders. This article delves into the working principle and key features of their systems, highlighting how they enhance material handling efficiency and operational safety.
Working Principle of the Pneumatic Conveying System
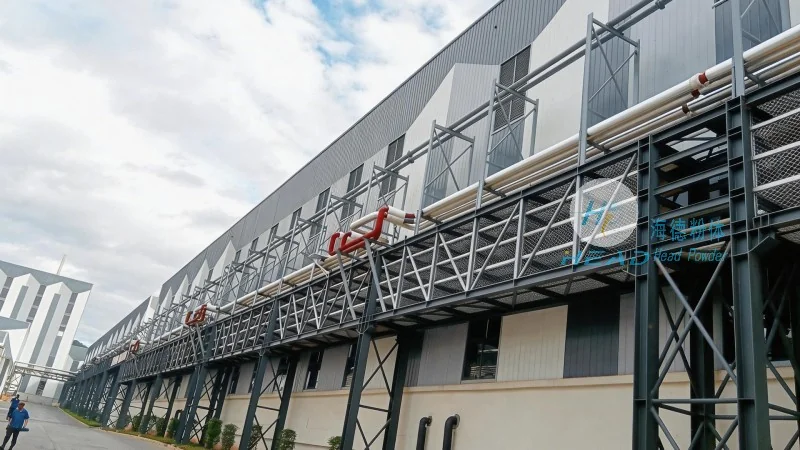
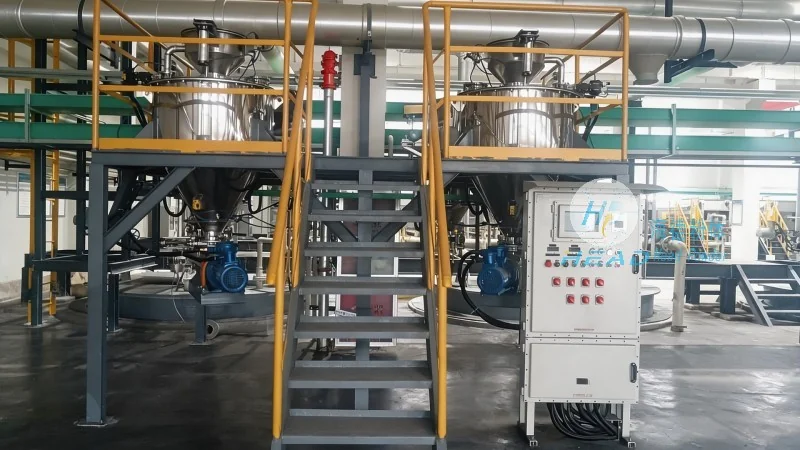
The core of the stabilizer powder pneumatic conveying system lies in its ability to transport bulk powders using compressed air. The system operates by generating a high-velocity air stream within a pipeline, which draws the powder particles into the flow. As the air and powder mixture travels through the system, it passes through various components such as feeders, separators, and filters. The working principle involves several critical steps: first, the powder is fed into the system via a hopper or feeder, then the compressed air is introduced to create a suction or pressure environment. The air flow carries the powder particles along the pipeline, ensuring consistent and controlled movement. The system is designed to maintain optimal air-to-powder ratios to prevent blockages and ensure smooth operation. This mechanism allows for the efficient transfer of stable powder materials from one location to another, eliminating the need for traditional bulk handling methods like trucks or conveyor belts.
Key Features and Advantages
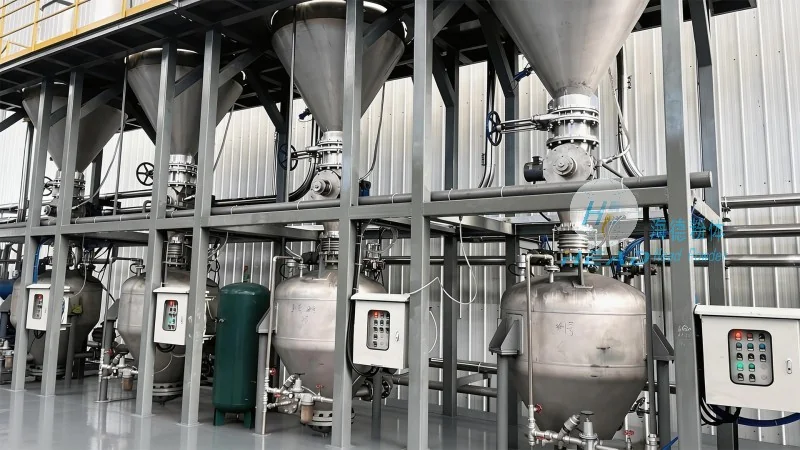
Shandong HeadPowder Engineering Co., Ltd.'s pneumatic conveying systems for stabilizer powders are equipped with several distinctive features that set them apart in the industry. One of the primary advantages is the high efficiency in material transport, which significantly reduces handling time and labor costs. The systems are engineered to minimize powder loss and contamination, ensuring that the product remains in its original state throughout the conveying process. Additionally, the technology offers enhanced safety by eliminating the need for manual handling of bulk powders, which can be hazardous in some applications. The systems are also designed with flexibility in mind, allowing for easy integration into existing production lines and adaptability to different powder types and particle sizes. Another notable feature is the automated control capabilities, which provide real-time monitoring of the conveying process, enabling operators to adjust parameters such as air pressure and flow rate as needed. This level of control not only improves operational efficiency but also contributes to better product quality and consistency. Furthermore, the systems are built with durability and low maintenance in mind, using high-quality materials and components that withstand the rigors of continuous operation. This reduces downtime and maintenance costs, making them a cost-effective solution for long-term use.
Application and Operational Benefits
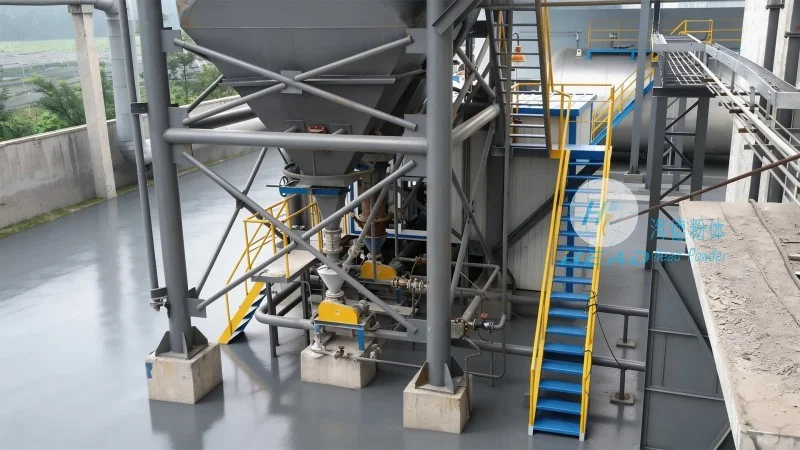
The stabilizer powder pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. are widely used in various industries, including chemical, pharmaceutical, and food processing. In these sectors, the efficient and safe transport of stabilizer powders is crucial for maintaining product quality and meeting regulatory standards. The systems offer several operational benefits, such as improved workflow by streamlining the material handling process, reduced environmental impact by minimizing dust emissions and waste, and enhanced productivity through faster and more reliable delivery of materials. The ability to handle different powder characteristics, such as varying particle sizes and moisture content, makes these systems versatile and suitable for diverse applications. Moreover, the systems contribute to better workplace safety by reducing exposure to dust and other airborne particles, which can be detrimental to employee health. This not only improves the working environment but also helps in complying with occupational safety regulations. Overall, the pneumatic conveying systems provide a comprehensive solution for the transportation of stabilizer powders, combining efficiency, safety, and reliability to meet the demands of modern industrial operations.