

Working Principle and Features of Cobalt Hydroxide Pneumatic Conveying Equipment
Cobalt hydroxide is a critical material in various industrial applications, and the efficient handling of this material is essential for maintaining production efficiency and product quality. The pneumatic conveying equipment designed for cobalt hydroxide plays a vital role in this process, offering a reliable and effective method for material transport. This article will delve into the working principle and key features of such equipment, providing a comprehensive overview for industry professionals.
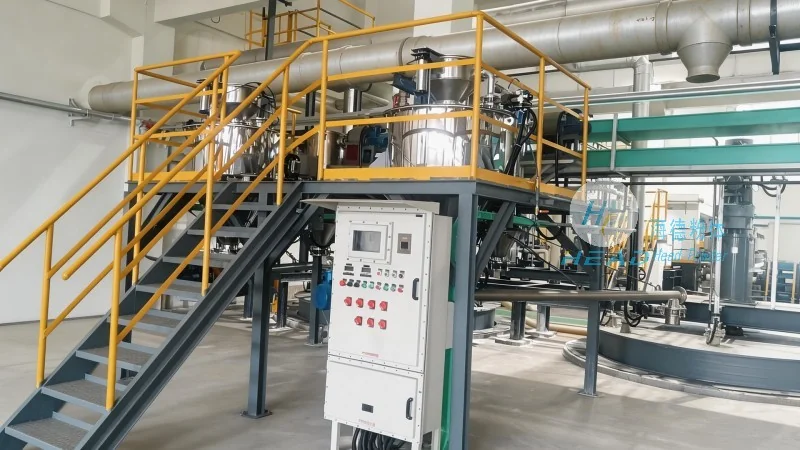
The Working Principle of Cobalt Hydroxide Pneumatic Conveying Systems
The core of cobalt hydroxide pneumatic conveying systems lies in the use of air or gas to transport the material. The process typically involves a series of components that work in concert to ensure smooth material movement. At the heart of the system is a feeding mechanism, which introduces the cobalt hydroxide powder into the conveying line. This is often achieved through a hopper or a rotary valve, which controls the flow rate and prevents material buildup. Once the material is introduced, a high-pressure air or gas stream is generated, usually by a blower or a compressor. This pressurized air creates a vacuum or pressure differential that propels the material particles forward through the pipeline. The conveying line itself is typically made of materials resistant to corrosion and abrasion, such as stainless steel or special plastics, to withstand the abrasive nature of cobalt hydroxide. The system may also include a filter or a cyclone separator at the receiving end to capture any fine particles and return them to the system, ensuring minimal loss and maintaining material purity.
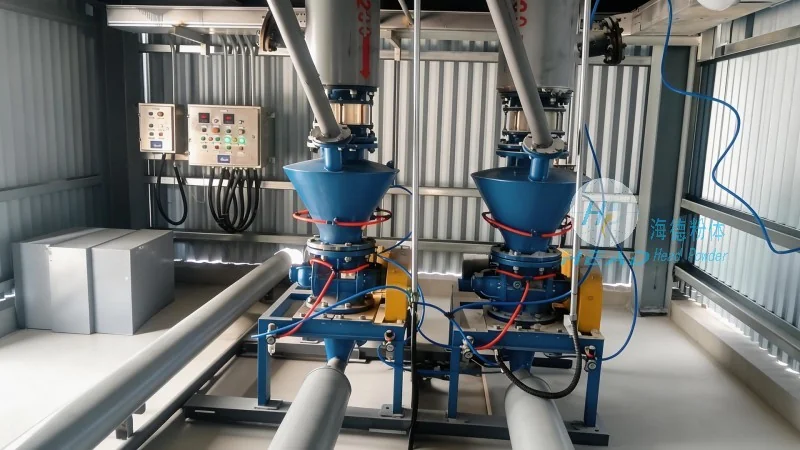
Key Features of Cobalt Hydroxide Pneumatic Conveying Equipment
Several distinct features make cobalt hydroxide pneumatic conveying equipment particularly suitable for this application. First, the equipment offers a closed system, which is crucial for maintaining the purity of the material and preventing contamination from external sources. This is especially important in industries where product quality is paramount, such as pharmaceuticals or electronics manufacturing. Second, the system provides high efficiency in terms of material transport, with the ability to move large quantities of cobalt hydroxide over significant distances with minimal energy consumption compared to traditional methods like bucket elevators or belt conveyors. Third, the equipment is designed for low maintenance, with components that are easy to access and replace, reducing downtime and operational costs. Additionally, the system can be easily integrated with other industrial processes, such as mixing or packaging, allowing for a seamless workflow. The flexibility of the system also allows for adjustments in flow rate and pressure, enabling operators to adapt to changing production needs. Another notable feature is the ability to handle materials with varying particle sizes and moisture content, making it versatile for different cobalt hydroxide formulations.
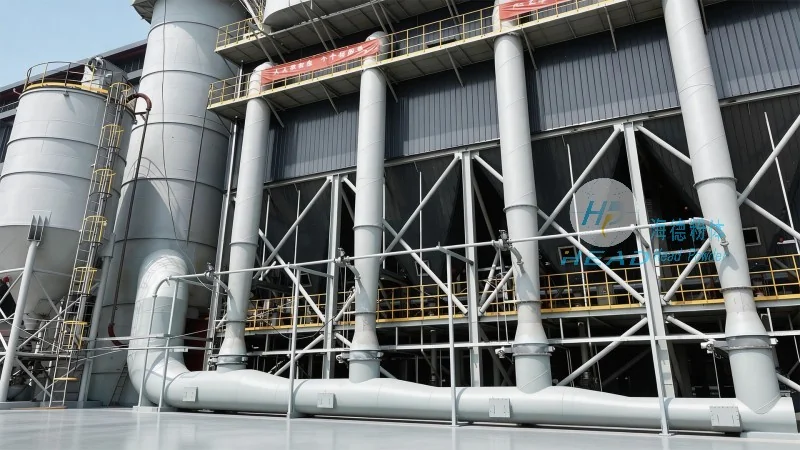
Company Information: Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer in the field of powder handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality solutions for the transport and processing of various powders, including cobalt hydroxide. The company is committed to delivering equipment that meets the stringent requirements of industrial applications, ensuring reliability, efficiency, and durability. With a focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for businesses seeking to optimize their material handling processes. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. This enables the company to develop and produce equipment that adheres to international standards and meets the specific needs of its clients. HeadPowder's team of engineers and technicians continuously researches and develops new technologies to improve the performance and functionality of its products, staying ahead of industry trends and customer expectations.