

Working Principle and Features of High-Pressure Dilute-Phase Pneumatic Conveying Systems
High-pressure dilute-phase pneumatic conveying systems represent a sophisticated and efficient method for transporting bulk materials over long distances or within industrial facilities. These systems are designed to handle a wide range of powders and granular materials, offering a solution that minimizes material degradation and ensures consistent flow. The technology behind these systems combines high-pressure air or gas with a dilute concentration of material particles, enabling smooth and reliable material transport. This approach is particularly valuable in industries such as food processing, pharmaceuticals, chemicals, and mining, where maintaining product integrity and operational efficiency is paramount.
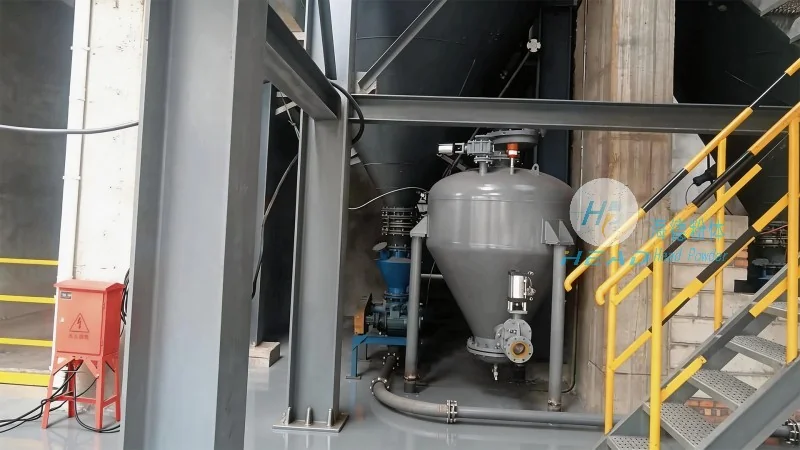
Working Principle of High-Pressure Dilute-Phase Pneumatic Conveying Systems
The core of a high-pressure dilute-phase pneumatic conveying system lies in its ability to generate sufficient air pressure to move material particles through a pipeline. The process typically begins with a material feeder, which introduces the bulk material into the system. This material is then mixed with a high-velocity air stream, creating a dilute suspension of particles in the air. The air, under high pressure, propels the mixture through the conveying line, which may include bends, expansions, or other components to direct the flow. At the discharge end, the air and material are separated, often using a cyclone or other separation equipment, allowing the material to be collected while the air is either recirculated or vented. The entire system is controlled by a series of valves, sensors, and a control panel to ensure optimal performance and safety. The high-pressure aspect of the system ensures that the material is transported efficiently, even over long distances, with minimal pressure loss and consistent flow rates.
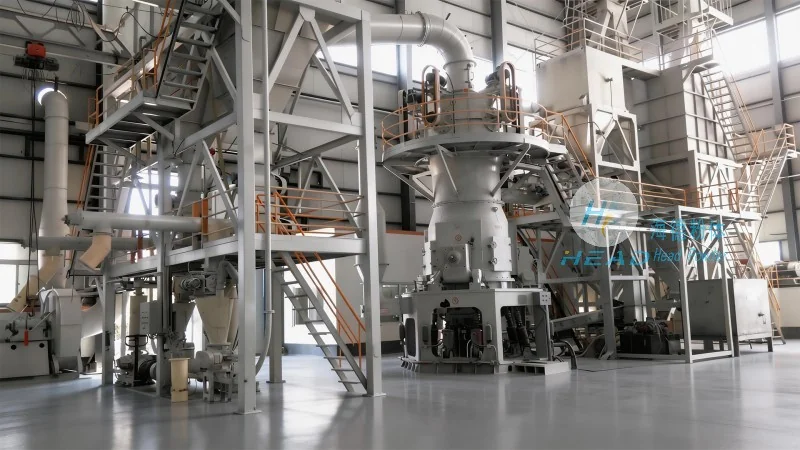
Key Features of High-Pressure Dilute-Phase Pneumatic Conveying Systems
High-pressure dilute-phase pneumatic conveying systems are characterized by several key features that make them suitable for diverse industrial applications. One of the primary features is the ability to handle a wide variety of materials, including fine powders, granules, and even abrasive or corrosive substances. This versatility is achieved through the system's design, which allows for adjustments in air pressure, flow rate, and particle concentration to accommodate different material properties. Another significant feature is the system's efficiency in terms of energy consumption and operational costs. By using high-pressure air, the system minimizes the need for mechanical components like conveyors or elevators, reducing maintenance requirements and operational expenses. Additionally, the system offers excellent material handling capabilities, with the ability to transport materials over long distances with minimal degradation, ensuring that the product quality is maintained throughout the process. The system also provides flexibility in terms of layout, as it can be integrated into existing industrial facilities or designed as a standalone unit, adapting to various spatial constraints and operational needs.
Technical Advantages and Practical Applications
High-pressure dilute-phase pneumatic conveying systems offer several technical advantages that enhance their performance and reliability. One of the key advantages is the ability to maintain a consistent flow rate, which is crucial for processes that require precise material delivery. The system's design allows for precise control over the air pressure and material feed rate, ensuring that the flow remains stable even under varying load conditions. Another advantage is the system's resistance to material buildup and blockages, as the dilute-phase operation reduces the likelihood of clogging in the pipeline. This is particularly important for handling materials with high moisture content or those that tend to agglomerate. In terms of practical applications, these systems are widely used in the food and beverage industry for transporting ingredients like flour, sugar, and spices, where product purity and hygiene are critical. They are also employed in the pharmaceutical industry for handling active pharmaceutical ingredients (APIs) and other sensitive materials, where contamination and degradation must be avoided. Furthermore, in the chemical and mining sectors, high-pressure dilute-phase systems are used to transport powders, granules, and ores, enabling efficient material handling in large-scale production processes.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of high-pressure dilute-phase pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industrial material handling sector. HeadPowder's products are designed to meet the specific needs of various industries, offering customized solutions that enhance operational efficiency and product quality. The company's manufacturing facilities are equipped with advanced technology and stringent quality control measures, ensuring that each system meets the highest standards of performance and reliability. HeadPowder's team of experienced engineers and technicians provides comprehensive support, from system design and installation to maintenance and troubleshooting, helping clients optimize their material handling processes. Based in Shandong, China, HeadPowder leverages its local expertise and resources to deliver efficient and cost-effective solutions to customers worldwide.