

Working Principle and Features of Chocolate Pneumatic Conveying Equipment
Chocolate pneumatic conveying equipment is a specialized system designed to transport chocolate products efficiently and hygienically. Understanding its working principle and key features is crucial for manufacturers seeking to optimize their production processes. This article explores the fundamental mechanisms behind these systems and highlights the advantages they offer in the chocolate industry.
HeadPowder, a leading provider in the field, offers advanced solutions tailored to the unique demands of chocolate processing. Based in Shandong, China, the company combines expertise in engineering and material handling to deliver reliable equipment that meets industry standards. The following sections delve into the operational principles and distinctive characteristics of chocolate pneumatic conveyors.
The Working Principle of Chocolate Pneumatic Conveying Equipment
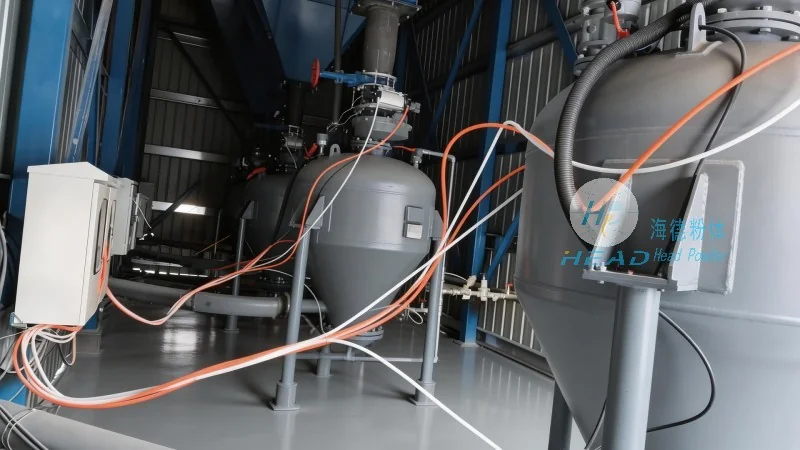
At its core, a chocolate pneumatic conveying system operates by using air pressure to move bulk materials through a pipeline. The process typically involves several key components, including a hopper for material storage, a rotary valve or feeder to control the flow rate, and a series of pipes that transport the chocolate from one location to another. The system can be classified into two main types: dilute phase and dense phase, each with its own operational characteristics.
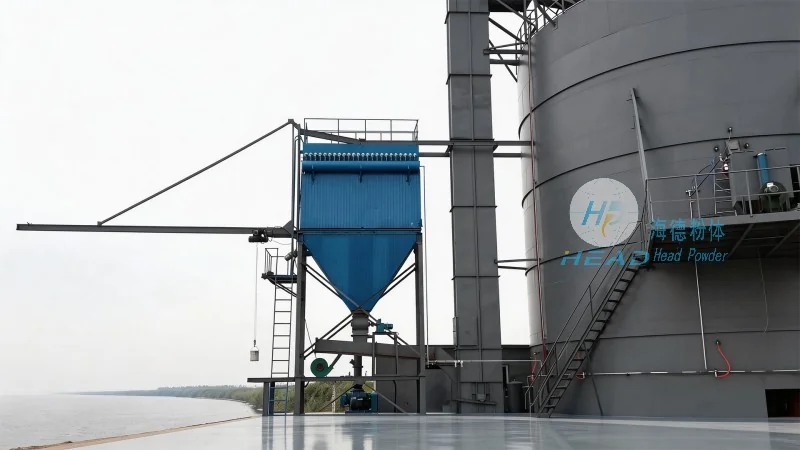
In a dilute phase system, the chocolate is suspended in air as it travels through the pipeline. This method is ideal for short to medium distance transport and requires lower air velocity compared to dense phase systems. The air flow is carefully controlled to ensure the chocolate particles remain in suspension without settling or clogging the pipes. The system often includes a cyclone separator at the receiving end to separate the chocolate from the air, allowing for clean and efficient material collection.
Dense phase pneumatic conveying, on the other hand, uses higher air pressure and lower velocity to move chocolate in a more compact form. This approach minimizes product degradation and is suitable for longer distances or when handling more sensitive materials. The chocolate is transported in a semi-solid state, reducing the risk of breakage or contamination. Both systems rely on precise air pressure regulation and material feed control to maintain consistent performance.
Key Features of Chocolate Pneumatic Conveying Equipment
Several notable features distinguish high-quality chocolate pneumatic conveying equipment, making it an attractive choice for manufacturers. One of the primary advantages is the hygienic design, which is essential in food processing environments. The equipment is constructed from materials such as stainless steel, ensuring compliance with food safety regulations and easy cleaning. This design minimizes the risk of contamination and maintains product integrity throughout the conveying process.
Another significant feature is the flexibility in system configuration. Manufacturers can customize the equipment to suit their specific production needs, including varying pipe lengths, number of branches, and material handling capacities. This adaptability allows for seamless integration into existing production lines without disrupting operations. The systems also offer energy efficiency, as they use compressed air to move materials, reducing the need for additional mechanical components and lowering operational costs.
Operational reliability is a critical feature highlighted by HeadPowder. The equipment is engineered to handle the unique properties of chocolate, such as its viscosity and tendency to stick to surfaces. Advanced sealing mechanisms and anti-clogging features prevent material buildup and ensure continuous operation. Additionally, the systems are equipped with monitoring and control systems that allow operators to track performance in real-time, enabling quick adjustments to maintain optimal conveying conditions.
Conclusion
Chocolate pneumatic conveying equipment, as explained above, combines efficient material transport with hygienic and reliable operation. The working principle, which relies on air pressure to move chocolate through pipelines, offers significant advantages over traditional methods like bucket elevators or belt conveyors. Key features such as hygienic design, flexibility, and energy efficiency make these systems a preferred choice for chocolate manufacturers. HeadPowder, with its expertise and commitment to quality, provides top-tier solutions that enhance production efficiency and product quality. By understanding the working principles and features of these systems, manufacturers can make informed decisions to optimize their chocolate processing operations.