

Inert Gas Circulation Powder Pneumatic Conveying System: Working Principles and Features
The inert gas circulation powder pneumatic conveying system is a specialized industrial equipment designed for the efficient and safe transportation of powders and bulk materials. This system utilizes inert gases, typically nitrogen or carbon dioxide, to create a closed-loop conveying environment, ensuring that the material is handled without exposure to air or other reactive gases. The system is particularly valuable in industries where material contamination, oxidation, or dust explosion risks are concerns, such as pharmaceuticals, food processing, and chemical manufacturing.
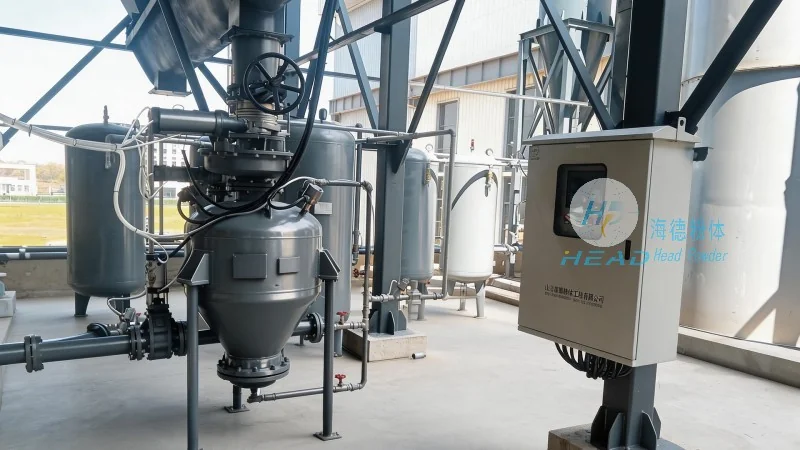
Working Principles of the Inert Gas Circulation System
The core operation of the inert gas circulation powder pneumatic conveying system involves several key components and processes. The system typically consists of a material hopper, a conveying line, a gas circulation unit, and a dust collection or filtration system. The process begins with the material being loaded into the hopper. An inert gas is then introduced into the system, creating a pressurized environment within the conveying line. As the gas flows through the line, it picks up the powder particles and transports them to the destination point, such as a storage silo or processing unit. The gas, now mixed with the powder, is then directed back to the gas circulation unit where it is filtered to remove any fine particles before being recirculated. This closed-loop design minimizes gas consumption and ensures consistent material flow.
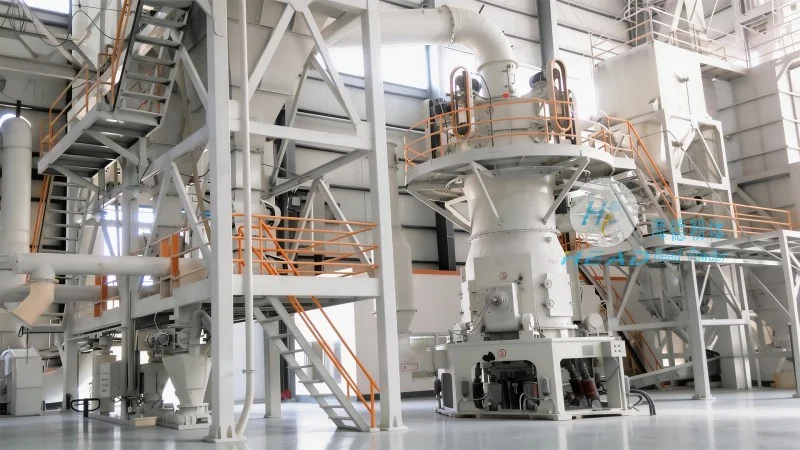
Key Features and Advantages
One of the primary advantages of the inert gas circulation powder pneumatic conveying system is its ability to maintain a controlled environment for sensitive materials. By using inert gases, the system prevents oxidation, moisture absorption, or contamination from ambient air, which is crucial for products like pharmaceutical powders or food-grade ingredients. Additionally, the closed-loop gas system reduces energy consumption compared to traditional pneumatic conveying methods, as the gas is continuously recirculated rather than being vented to the atmosphere. The system also offers high conveying efficiency, with the ability to transport materials over long distances and at high capacities without the need for mechanical components like belts or screws. Another notable feature is the system's flexibility, as it can be adapted to handle a wide range of powder types and sizes, from fine powders to bulk materials. The dust collection and filtration components ensure that the system operates in compliance with environmental regulations, maintaining a clean and safe working environment.
Applications in Industrial Settings
The inert gas circulation powder pneumatic conveying system is widely used across various industries due to its versatility and reliability. In the pharmaceutical industry, it is essential for transporting active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials remain sterile and free from contamination. In food processing, the system is used to handle powders like flour, sugar, and spices, maintaining product quality and safety. The chemical industry also benefits from this technology, particularly when handling reactive or hazardous powders, as the inert gas environment prevents unwanted chemical reactions. Furthermore, the system is suitable for applications in the cement, mining, and agricultural sectors, where bulk materials need to be transported efficiently and safely. The system's ability to handle high volumes and long distances makes it an ideal solution for large-scale industrial operations.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of the inert gas circulation powder pneumatic conveying system, is a leading company in the field of powder handling and processing equipment. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted provider of industrial solutions for various industries. The company is headquartered in Shandong, China, and specializes in designing, manufacturing, and supplying advanced powder conveying systems tailored to the specific needs of its clients. HeadPowder's commitment to customer satisfaction and technical excellence has made it a preferred choice for businesses seeking reliable and efficient powder handling solutions. The company's products are known for their durability, efficiency, and compliance with international standards, ensuring that clients receive high-quality equipment that meets their operational requirements.