

Working Principle and Features of High-Pressure Pulse Powder Pneumatic Conveying System
High-pressure pulse powder pneumatic conveying systems represent a sophisticated technology in material handling, designed to efficiently transport bulk powders over long distances with minimal operational complexity. This system, developed by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, utilizes high-pressure air pulses to move powders through pipelines, offering a reliable solution for various industrial applications.
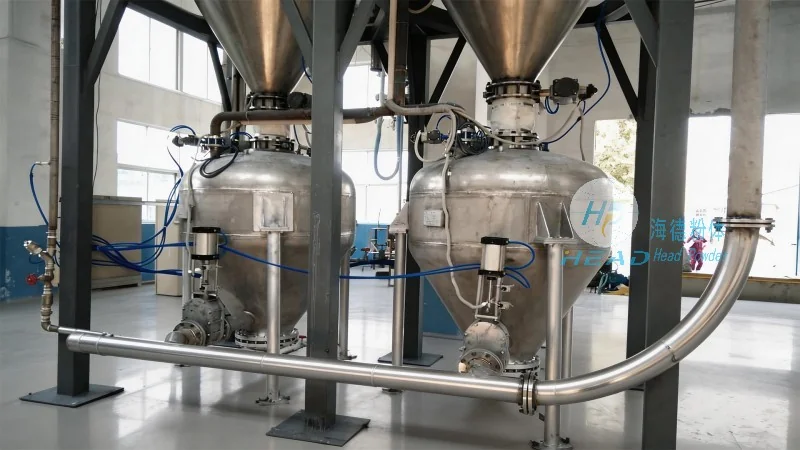
Working Principle of the High-Pressure Pulse Powder Pneumatic Conveying System
The core mechanism of this system involves the generation of high-pressure air pulses that create a dynamic flow within the conveying pipeline. As air is discharged from the pulse generator, it creates a pressure wave that propels the powder particles forward. The system typically includes components such as a pulse valve, air compressor, and pipeline network, all working in tandem to ensure consistent and efficient material transport. The high-pressure air pulses are timed and controlled to maintain a steady flow rate, preventing material buildup and ensuring smooth operation. The design allows for adjustable pulse frequency and pressure, enabling customization based on the specific characteristics of the powder being conveyed, such as particle size, density, and moisture content.
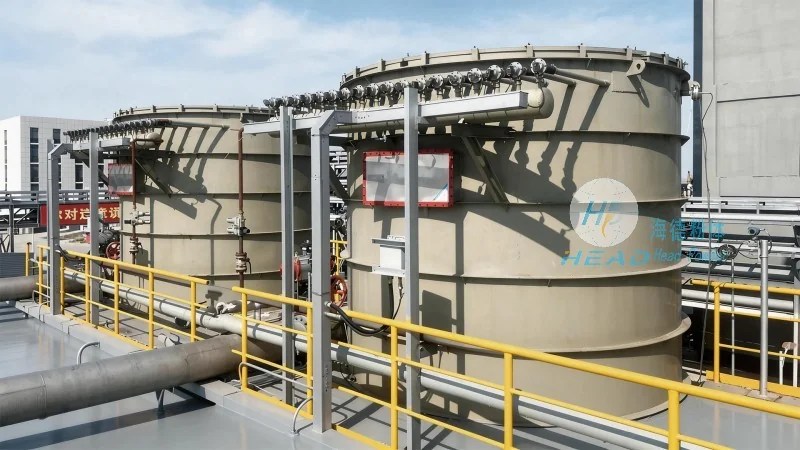
Key Features of the High-Pressure Pulse Powder Pneumatic Conveying System
One of the standout features of this system is its ability to handle a wide range of powder types, from fine powders to bulk materials, with minimal degradation. The high-pressure air pulses ensure that the powder remains suspended and transported without caking or agglomeration, which is critical for maintaining product quality. Additionally, the system is designed for low maintenance, with components that are easy to access and replace, reducing downtime and operational costs. Another key feature is its energy efficiency, as the high-pressure pulses are optimized to use minimal air volume while achieving maximum conveying capacity. The system also offers flexibility in terms of pipeline layout, allowing for complex network configurations to accommodate multiple source and destination points. Furthermore, the system is equipped with safety features, including pressure relief valves and monitoring systems, to prevent over-pressurization and ensure safe operation in industrial environments.
Applications and Benefits in Industrial Settings
High-pressure pulse powder pneumatic conveying systems are widely used in industries such as pharmaceuticals, food processing, chemical manufacturing, and mining. The system's ability to handle sensitive materials without contamination or degradation makes it ideal for applications where product purity is paramount. For example, in pharmaceutical production, the system can transport active pharmaceutical ingredients (APIs) and excipients with precision, ensuring that the final product meets stringent quality standards. In the food industry, it is used to convey ingredients like flour, sugar, and spices, maintaining their freshness and preventing cross-contamination. The system also offers significant benefits in terms of space efficiency, as it eliminates the need for traditional bulk handling equipment like conveyor belts and elevators, which require large floor space. This makes it particularly suitable for facilities with limited space or complex layouts. Moreover, the system's ability to transport materials over long distances without intermediate storage reduces inventory costs and improves production throughput. The low maintenance requirements and energy efficiency further contribute to cost savings, making it a cost-effective solution for long-term industrial use.
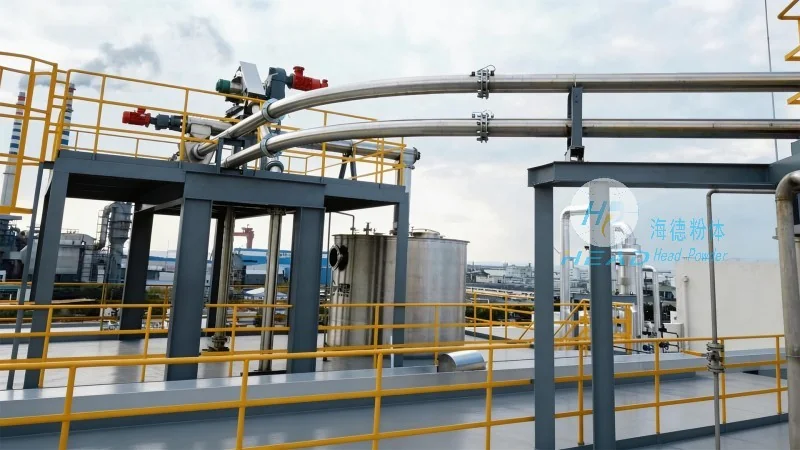
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, specializes in the design, manufacturing, and installation of high-pressure pulse powder pneumatic conveying systems. The company's expertise in material handling technology ensures that each system is tailored to meet the specific needs of its clients, providing reliable and efficient solutions for bulk powder transport. By leveraging advanced engineering and quality control processes, HeadPowder delivers systems that are durable, efficient, and compliant with industry standards. The company's commitment to innovation and customer satisfaction has established it as a trusted partner in the material handling industry, helping businesses optimize their operations and improve productivity. With a focus on providing customized solutions and exceptional service, HeadPowder continues to be a leader in the development of high-pressure pulse powder pneumatic conveying systems.