

Working Principle and Features of Chocolate Powder Pneumatic Conveying Systems
Chocolate powder is a critical ingredient in the food industry, widely used in confectionery, bakery, and beverage production. Efficient and reliable handling of this fine powder is essential to maintain product quality and operational efficiency. Pneumatic conveying systems have emerged as a preferred solution for transporting chocolate powder due to their ability to handle delicate materials while ensuring hygienic and controlled processes. This article explores the working principle and key features of chocolate powder pneumatic conveying lines, highlighting how they enhance production workflows.
Working Principle of Chocolate Powder Pneumatic Conveying Systems
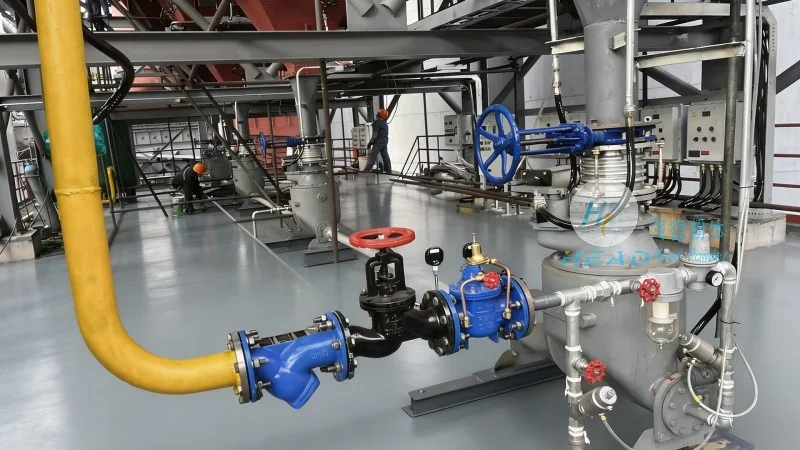
The core mechanism of chocolate powder pneumatic conveying involves the use of compressed air to transport powder particles through a network of pipes. There are primarily two types of pneumatic conveying systems: positive pressure and negative pressure. In positive pressure systems, air is forced into the conveying line, carrying the powder from the source to the destination. This method is suitable for short to medium distance transport and is often used in applications where the powder needs to be delivered to multiple points. Negative pressure systems, on the other hand, create a vacuum in the line, drawing the powder from the source and moving it towards the collection point. This approach is ideal for longer distances and when the powder must be transported from multiple sources to a central location.
Within these systems, the chocolate powder is typically fed into the conveying line via a hopper or a rotary valve. The air flow is controlled by a blower or a vacuum pump, ensuring consistent particle movement. The design of the pipeline, including bends, elbows, and filters, is crucial to prevent powder buildup and maintain system efficiency. Filters are essential to capture any fine particles that may escape, protecting downstream equipment and ensuring product purity. The entire process is often automated, with sensors monitoring air pressure, flow rate, and powder level to maintain optimal performance.
Key Features and Advantages of Chocolate Powder Pneumatic Conveying Lines
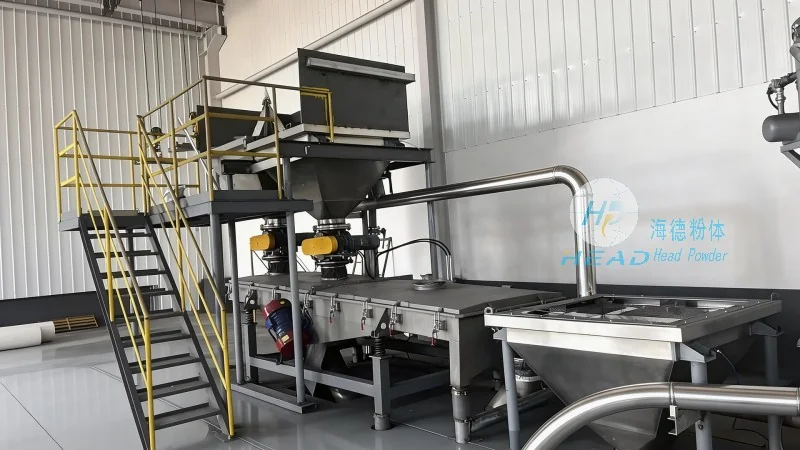
Chocolate powder pneumatic conveying lines offer several distinct advantages that make them a preferred choice in the food industry. One of the most significant features is their hygienic design. The systems are constructed from materials that meet food-grade standards, such as stainless steel, which prevents contamination and ensures easy cleaning. This is particularly important in chocolate production, where product quality and safety are paramount. The enclosed pipeline system also minimizes dust exposure, improving workplace safety and reducing the risk of product contamination from external sources.
Another key feature is the high efficiency and flexibility of these systems. Pneumatic conveying allows for the transport of chocolate powder over long distances without the need for multiple transfer points, reducing the risk of material degradation and loss. The ability to adjust air pressure and flow rate enables precise control over the conveying process, ensuring consistent product quality. Additionally, these systems can handle a wide range of powder characteristics, including different particle sizes, moisture content, and flowability, making them versatile for various chocolate production applications.
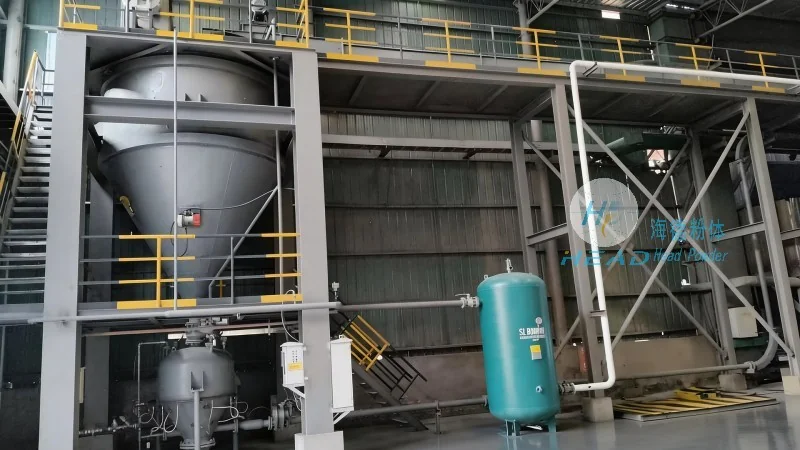
Operational reliability is another critical feature. The use of automated controls and monitoring systems ensures that the conveying process runs smoothly, with minimal downtime. Regular maintenance, such as cleaning filters and checking air pressure, is essential to maintain system performance. The robust construction of the pipeline and components ensures that the system can withstand the demands of continuous production, providing long-term reliability.
Applications in Chocolate Production
Chocolate powder pneumatic conveying systems are widely used in various stages of chocolate production. In the initial stages, these systems are used to transport raw cocoa powder from storage silos to processing equipment. During the production process, they help move intermediate products, such as melted chocolate or cocoa butter, between different processing units. In the final stages, the systems are employed to deliver finished chocolate powder to packaging lines or storage areas. The flexibility of pneumatic conveying allows manufacturers to adapt the system to different production requirements, whether it's for small-scale batches or large-scale industrial operations.
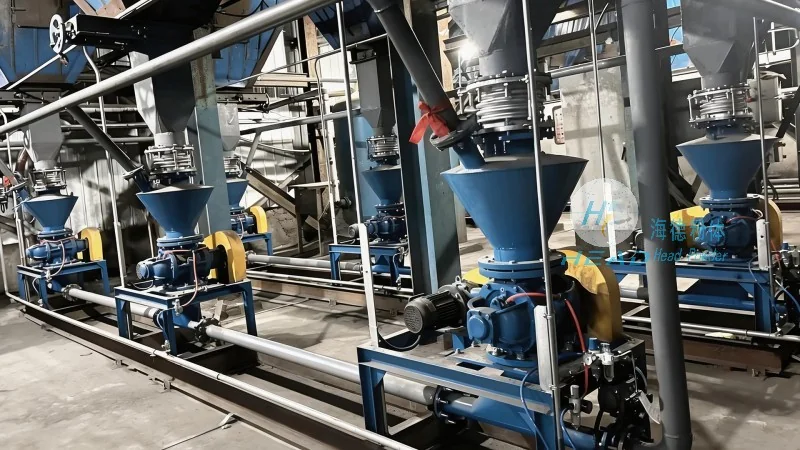
For example, in a confectionery factory, a pneumatic conveying line may be used to transport chocolate powder from a hopper to a mixing machine, ensuring that the powder is added uniformly and without any segregation. In a bakery, the system can be used to move chocolate powder from a storage tank to a mixing bowl, maintaining the consistency of the final product. The ability to handle fine powders without causing clumping or agglomeration is a significant advantage, as it preserves the texture and quality of the chocolate.
Conclusion
Chocolate powder pneumatic conveying systems are an essential component of modern chocolate production, offering efficient, hygienic, and reliable transport solutions. By understanding the working principle and key features of these systems, manufacturers can optimize their production processes, improve product quality, and enhance operational efficiency. As the demand for high-quality chocolate products continues to grow, the importance of effective powder handling systems like pneumatic conveying will only increase. Companies like Shandong HeadPowder Engineering Co., Ltd., with their expertise in designing and manufacturing such systems, play a crucial role in supporting the needs of the food industry.