

Principle and Working Scene Characteristics of Rotary Lobe Blower Material Pneumatic Conveying
Rotary lobe blowers are a type of positive displacement blower widely used in industrial applications for material handling and pneumatic conveying. These devices operate by using two lobed rotors that rotate in opposite directions within a housing, creating a series of air pockets that move material through a pipeline. The process of material pneumatic conveying, facilitated by such blowers, involves transporting bulk materials like powders, granules, and fine particles using air or other gases as the conveying medium. This method offers advantages such as high efficiency, low maintenance, and the ability to handle a wide range of materials, making it a preferred choice in various industries. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in developing and supplying advanced rotary lobe blower systems tailored to meet the diverse needs of industrial sectors.
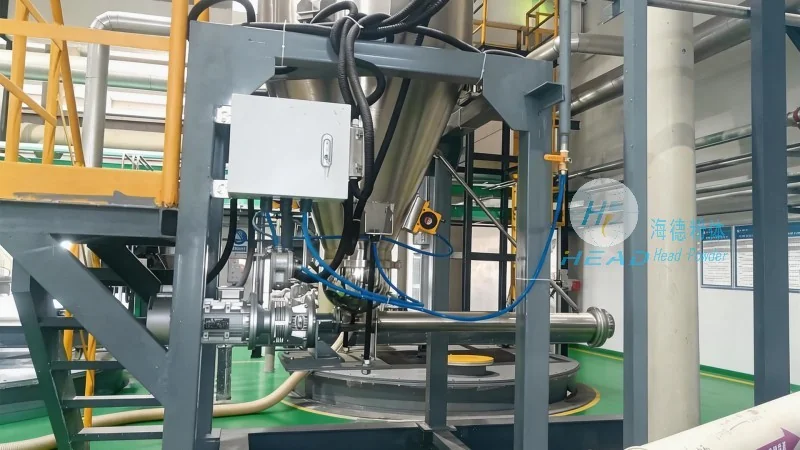
The Working Principle of Rotary Lobe Blower for Material Conveying
The core principle of rotary lobe blowers in material pneumatic conveying is based on the positive displacement mechanism. As the lobed rotors rotate, they trap air or gas in the cavities formed between the rotors and the housing. The rotation of the rotors then forces this trapped air/gas through the system, creating a pressure differential that propels the material forward. The speed and capacity of the blower can be adjusted to match the specific requirements of the material being conveyed, ensuring optimal performance. The design of the blower, including the number of lobes, rotor speed, and housing dimensions, is crucial in determining the efficiency and suitability for different material types and conveying distances.
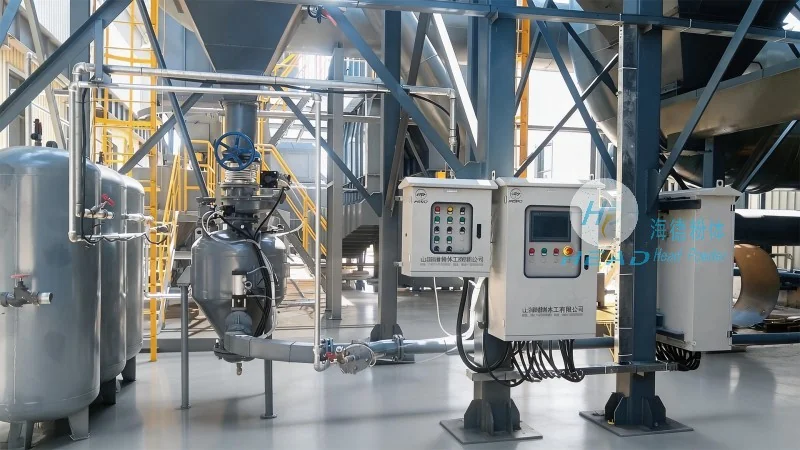
Key Working Scene Characteristics of Rotary Lobe Blower Material Conveying
Rotary lobe blowers are employed in diverse working scenarios, each with distinct characteristics that highlight their versatility. In manufacturing plants, these blowers are commonly used for conveying raw materials to processing units, such as transporting powders from storage silos to mixing equipment. In the food and pharmaceutical industries, where hygiene and material purity are critical, rotary lobe blowers are preferred due to their ability to handle sensitive materials without contamination. Additionally, in mining and construction sectors, they are used for transporting bulk materials like coal, sand, and gravel over long distances, leveraging their high pressure and flow capacity. The adaptability of rotary lobe blowers to different working environments makes them a reliable solution for material handling in various industrial applications.
Applications and Performance in Different Industries
Rotary lobe blowers with material pneumatic conveying capabilities are utilized across multiple industries, each benefiting from the specific attributes of the technology. In the chemical industry, they are essential for conveying powders and granules in processes like mixing, drying, and packaging. The ability of these blowers to handle abrasive materials without wear and tear is particularly valuable in such applications. In the agricultural sector, they are used for transporting grains and other agricultural products from storage to processing facilities, ensuring efficient and clean handling. The performance of rotary lobe blowers, measured by factors like pressure, flow rate, and power consumption, is tailored to meet the demands of each industry, ensuring optimal material transfer and operational efficiency.
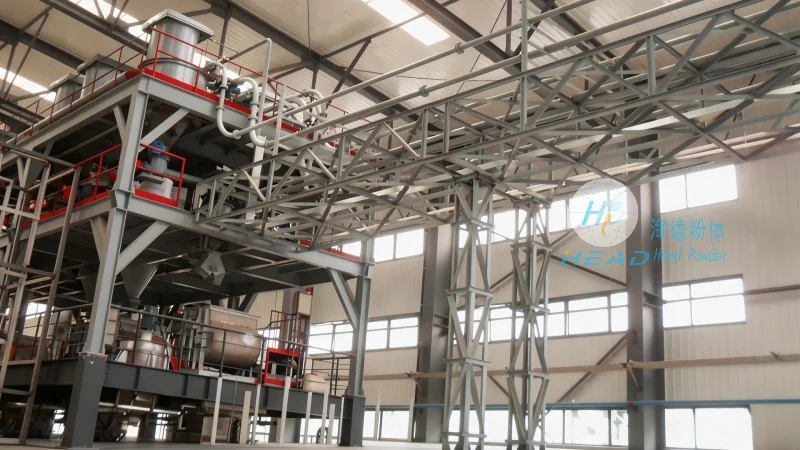
Advantages and Considerations in Material Pneumatic Conveying
When implementing rotary lobe blower material conveying systems, several advantages and considerations must be taken into account. The primary benefits include high conveying efficiency, reduced labor costs, and the ability to handle materials in a dust-free environment, which is crucial in industries like food and pharmaceuticals. However, challenges such as system design, material compatibility, and maintenance requirements need to be addressed. For instance, the choice of blower type (e.g., single-stage vs. multi-stage) and the selection of appropriate pipeline materials are critical to prevent material degradation or equipment damage. Regular maintenance, including rotor inspection and bearing replacement, is essential to ensure the longevity and performance of the system. By carefully evaluating these factors, industries can maximize the benefits of rotary lobe blower material conveying while minimizing potential issues.