

Operation Process and Working Principle of Multi-functional Powder Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of advanced powder conveying systems. These systems are engineered to handle a wide range of powder materials with precision and efficiency, catering to industries such as pharmaceuticals, chemicals, food processing, and more. The company's commitment to innovation ensures that each system is tailored to meet specific operational requirements, enhancing productivity and reliability in material handling processes.
Key Features of the Multi-functional Powder Conveying System
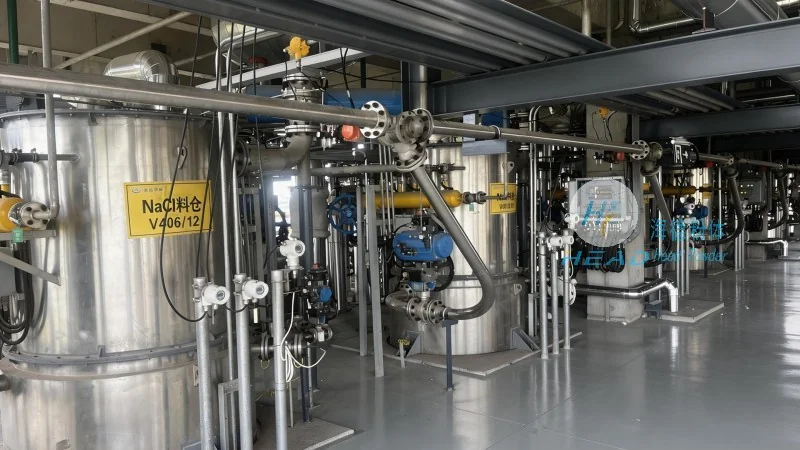
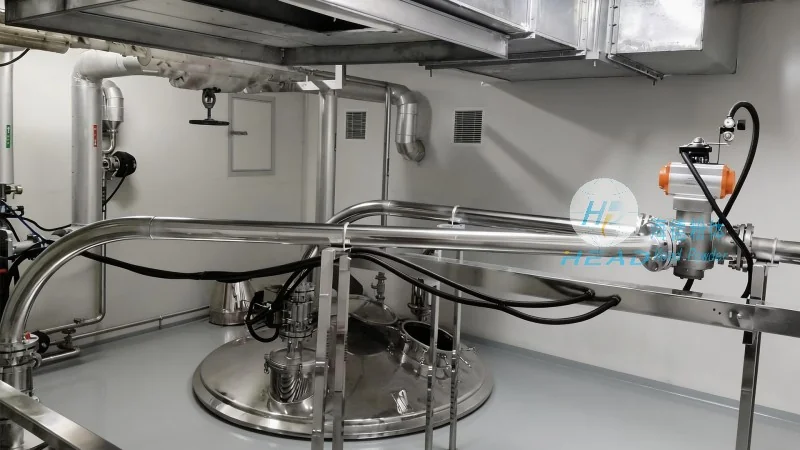
The multi-functional powder conveying system from Shandong HeadPowder Engineering Co., Ltd. is equipped with several advanced features that set it apart in the market. These include adjustable conveying speeds, temperature control options, and customizable material handling configurations. The system is designed to accommodate various powder types, from fine powders to bulk materials, ensuring consistent performance under different operational conditions. Additionally, the equipment incorporates robust safety mechanisms and easy maintenance features, reducing downtime and operational costs for users.
Operation Process and Working Principle
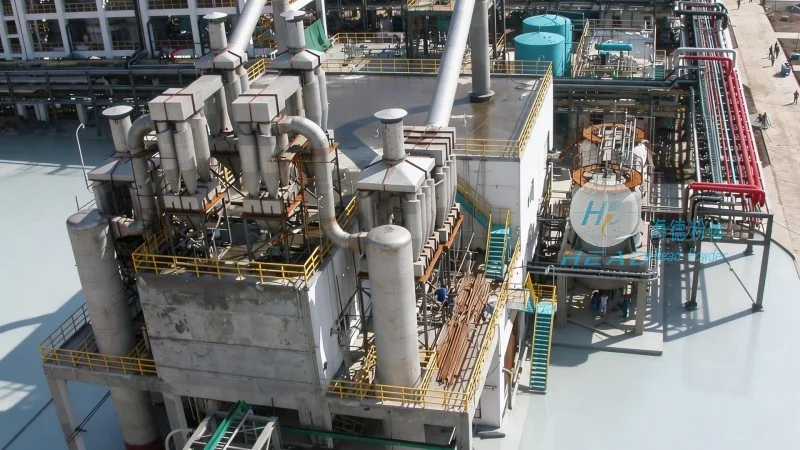
The operation of the multi-functional powder conveying system involves a series of coordinated steps that ensure smooth material transfer. The process begins with the loading of the powder into the hopper, where the material is stored before being fed into the conveying mechanism. The system uses a combination of positive displacement and pneumatic conveying technologies to transport the powder through the pipeline. The conveying speed is controlled by a variable frequency drive, allowing for precise adjustment based on the material's characteristics and the required throughput. The system also includes a filtration and cleaning mechanism to maintain air quality and prevent material buildup in the system. The working principle relies on the creation of a pressure differential between the inlet and outlet of the conveying line, which propels the powder forward. This method ensures efficient and low-loss material transfer, minimizing product degradation and waste.
Benefits and Applications
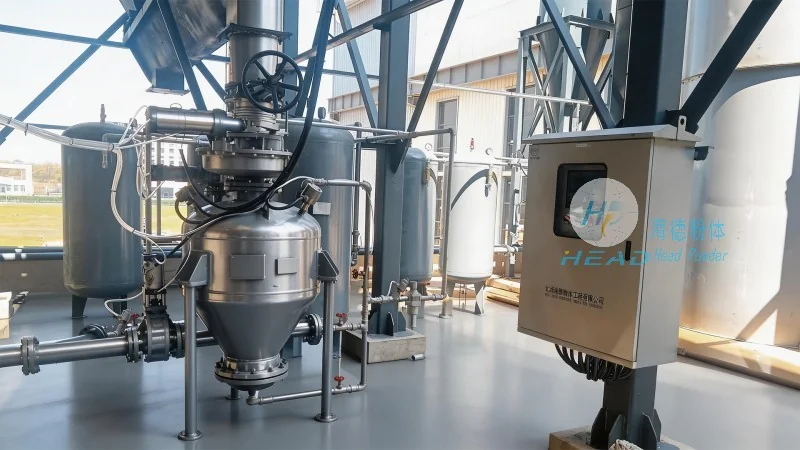
The multi-functional powder conveying system offers numerous benefits to industries that rely on consistent and reliable powder handling. The system's ability to handle diverse materials makes it suitable for applications in pharmaceutical manufacturing, where product purity and contamination control are critical. In the chemical industry, the system's temperature control features allow for the handling of heat-sensitive materials without degradation. The food processing sector benefits from the system's hygienic design and easy cleaning capabilities, ensuring compliance with food safety regulations. Overall, the system enhances operational efficiency by reducing manual handling, improving product quality, and minimizing energy consumption. The robust construction and advanced control systems ensure long-term reliability, making it a cost-effective solution for businesses seeking to optimize their material handling processes.