

Introduction to the Return Coke Powder Pneumatic Conveying System: Structure and Working Principle
HeadPowder, a leading enterprise in the field of industrial material handling, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. This article provides a comprehensive overview of the return coke powder pneumatic conveying system, focusing on its structural design and operational principles. The system is engineered to efficiently handle and transport coke powder, a critical material in various industrial processes, ensuring high reliability and performance.
Company Profile and Core Expertise
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is headquartered in Shandong, China. With years of experience in the engineering and manufacturing of material handling equipment, the company has established itself as a trusted provider of customized pneumatic conveying solutions. HeadPowder's expertise lies in understanding the unique challenges of material transport, particularly in high-temperature and abrasive environments, and developing systems that meet stringent industrial standards.
System Overview and Key Components
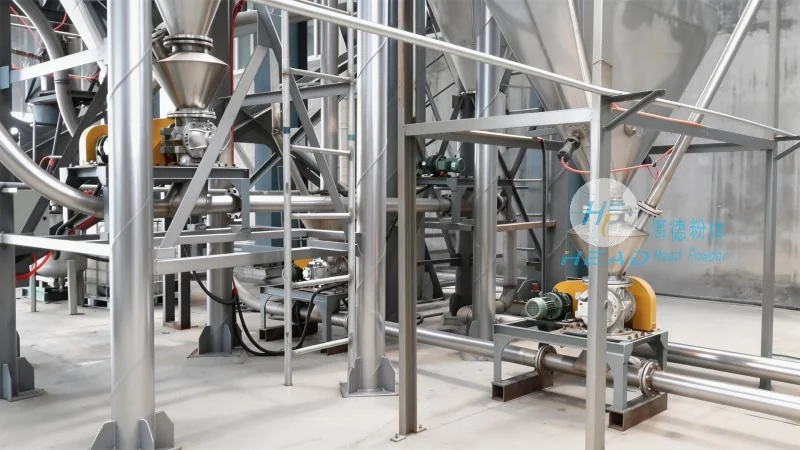
The return coke powder pneumatic conveying system is a sophisticated piece of equipment designed to manage the return flow of coke powder from downstream processes back to upstream handling units. The system comprises several critical components that work in tandem to ensure efficient material transport. These components include a return hopper, a rotary airlock valve, a filter unit, a blower or compressor, and a pipeline network. Each component is strategically designed to address specific operational requirements, such as material feeding, air filtration, and pressure control.
Structural Design and Working Principle
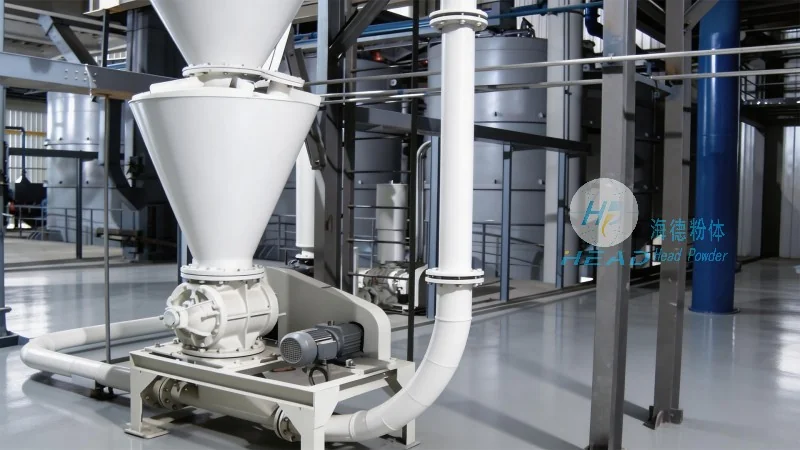
The structural design of the return coke powder pneumatic conveying system is optimized for both functionality and durability. The return hopper is typically made of high-strength materials, such as stainless steel, to withstand the abrasive nature of coke powder and prevent material buildup. It features a sloped bottom to facilitate smooth material discharge and is equipped with a level indicator to monitor the powder level. The rotary airlock valve, positioned at the outlet of the hopper, acts as a controlled feeding device, preventing backflow and maintaining consistent material flow rates.
The filter unit is a crucial component that ensures the air used for conveying is clean and free from particulate matter. It typically consists of a bag filter or a cartridge filter, which captures fine coke powder particles and returns clean air to the system. The blower or compressor provides the necessary air pressure to drive the material through the pipeline. The pipeline network is designed with appropriate diameters and bends to minimize pressure drop and maintain efficient material transport. The system operates on the principle of pneumatic conveying, where the material is suspended in a stream of air and transported through the pipeline under pressure.
Technical Advantages and Performance Characteristics
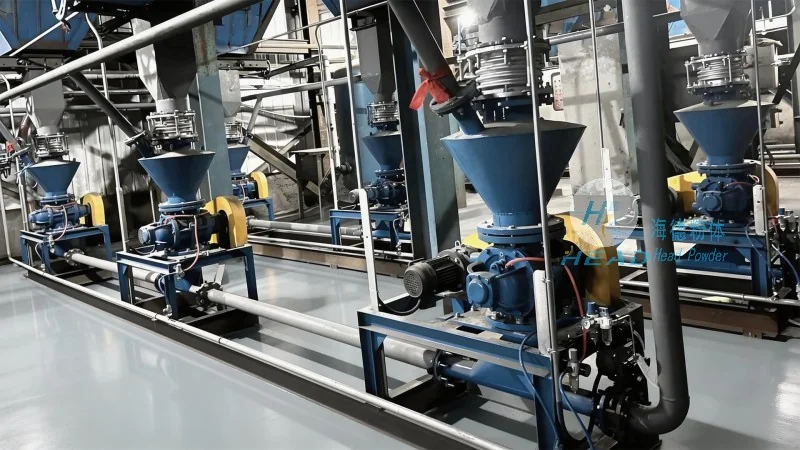
The return coke powder pneumatic conveying system offers several technical advantages that make it suitable for industrial applications. One of the key advantages is its ability to handle abrasive and high-temperature materials without causing wear or damage to the equipment. The stainless steel construction of the hopper and other components ensures long service life and minimal maintenance. The system also provides precise control over material flow rates, allowing for accurate dosing and process control. Additionally, the air filtration system ensures compliance with environmental regulations by preventing dust emissions into the environment.
Application Scenarios and Industry Impact
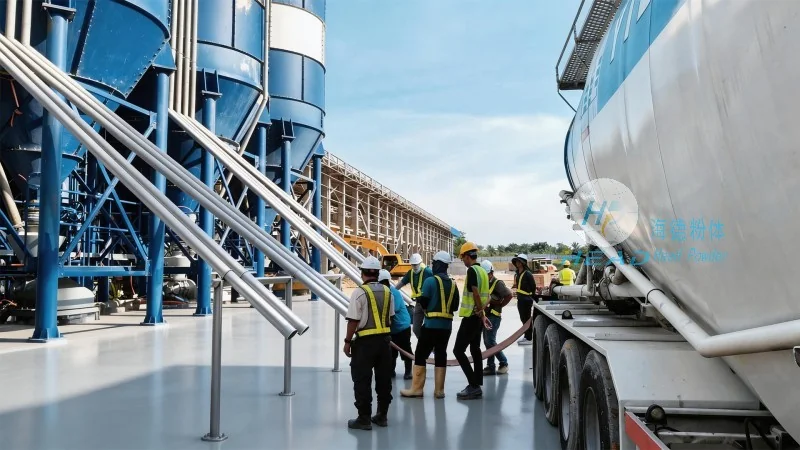
The return coke powder pneumatic conveying system is widely used in various industrial sectors, including steel production, power generation, and chemical processing. In steel mills, the system is used to return coke powder from the coke oven to the blending and storage areas, ensuring a continuous supply of raw material. In power plants, it helps in the efficient transport of coke powder from storage silos to the combustion chambers, improving the overall efficiency of the boiler system. The system's ability to handle large volumes of material at high speeds makes it an essential component in modern industrial operations.
Conclusion and Future Outlook
HeadPowder's return coke powder pneumatic conveying system represents a significant advancement in material handling technology. By combining robust structural design with advanced operational principles, the system provides reliable and efficient transport of coke powder, meeting the demands of modern industrial processes. As industrial requirements evolve, HeadPowder continues to innovate and develop new solutions to enhance material handling efficiency and sustainability. The company's commitment to quality and customer satisfaction ensures that its systems remain at the forefront of the industry, providing long-term value to its clients.