

The Role of Pneumatic Conveying in the Transport of Purified Ash
Efficient and reliable material handling is crucial in industrial processes, especially when dealing with materials like purified ash. Pneumatic conveying systems have emerged as a vital solution for transporting such materials, offering advantages in terms of safety, efficiency, and environmental compliance. This article explores the role of pneumatic conveying in the transport of purified ash, highlighting the capabilities and benefits of such systems.
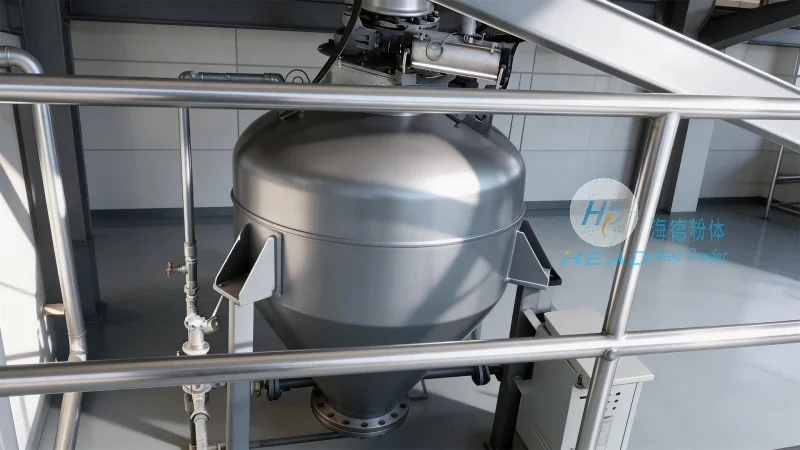
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries requiring efficient and safe transport of bulk materials. HeadPowder operates from its headquarters in Shandong, China, serving a diverse range of sectors including power generation, waste management, and industrial manufacturing.
Pneumatic Conveying Systems for Purified Ash Transport
Purified ash, often generated from industrial processes such as coal combustion or waste incineration, requires specialized handling to ensure environmental safety and operational efficiency. Traditional methods like belt conveyors or bucket elevators may pose challenges in terms of dust control, material degradation, and operational costs. Pneumatic conveying systems, on the other hand, provide a closed-loop transport solution that minimizes dust emissions and protects the material from external contaminants. These systems utilize air pressure to move ash particles through a pipeline network, ensuring a clean and efficient transfer process.
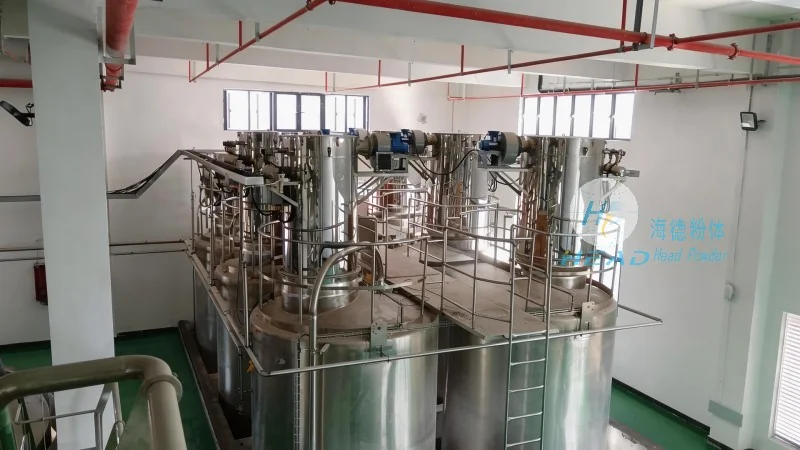
Key components of a pneumatic conveying system for purified ash include the feed hopper, air compressor, pipeline network, and discharge unit. The feed hopper is designed to store and feed the ash into the system, while the air compressor generates the necessary pressure to move the material. The pipeline network, typically made of stainless steel or other corrosion-resistant materials, ensures the safe and efficient transport of the ash. The discharge unit then collects the ash at the destination point, completing the transport cycle. HeadPowder's systems are engineered to handle various ash characteristics, including different particle sizes, moisture content, and chemical compositions, ensuring optimal performance under diverse operational conditions.
Advantages of Pneumatic Conveying for Purified Ash
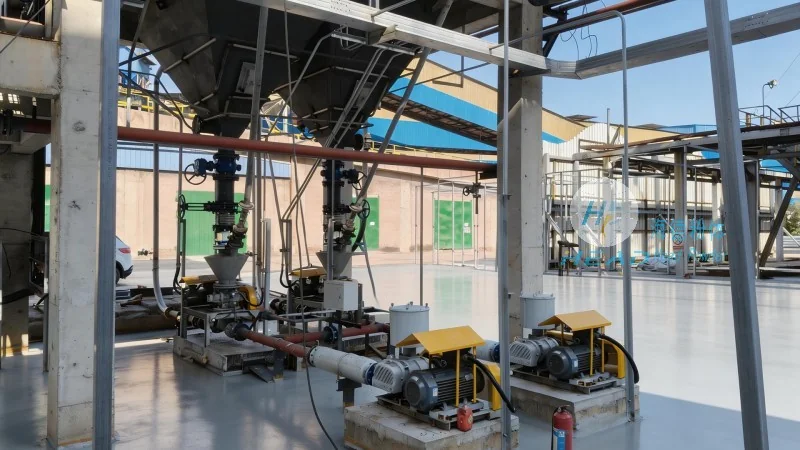
Compared to traditional bulk material handling methods, pneumatic conveying offers several advantages when transporting purified ash. Firstly, it provides a dust-free environment, which is critical for maintaining air quality and ensuring compliance with environmental regulations. The closed-loop system prevents dust from escaping into the workplace or the surrounding environment, reducing the risk of respiratory issues and other health hazards. Secondly, pneumatic conveying systems are highly efficient in terms of energy consumption and operational costs. By using air pressure to move the material, the system minimizes the need for mechanical components like belts or buckets, reducing maintenance requirements and extending the lifespan of the equipment. Thirdly, these systems offer flexibility in terms of layout and installation. The pipeline network can be easily configured to suit the specific needs of the facility, allowing for easy integration with existing infrastructure. Additionally, pneumatic conveying systems can handle high volumes of material at a consistent rate, ensuring smooth and continuous operation.
Application in Industrial Settings
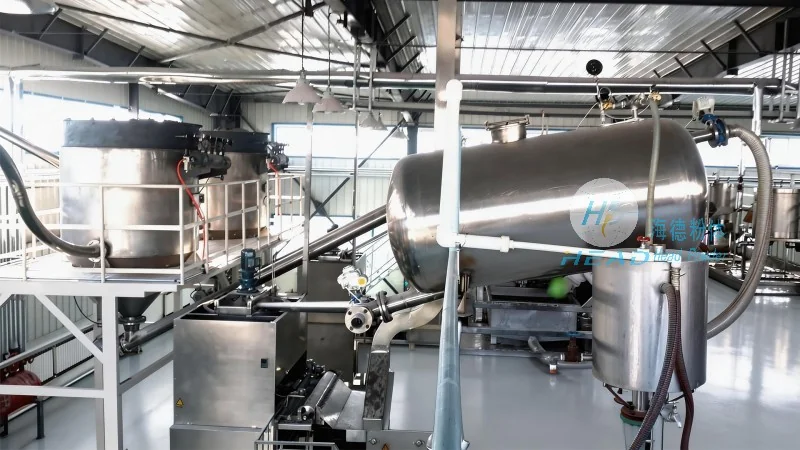
Pneumatic conveying systems are widely used in industrial settings where purified ash needs to be transported from the point of generation to storage or disposal facilities. For example, in power plants, ash generated from coal combustion is often transported using pneumatic systems to avoid dust contamination and ensure safe handling. In waste management facilities, ash from incineration processes is similarly handled using these systems to maintain environmental standards. The systems are also used in industrial manufacturing plants where ash byproducts are produced during production processes. HeadPowder's systems have been successfully implemented in various industrial applications, demonstrating their reliability and effectiveness in meeting the specific needs of different industries.
Conclusion
Pneumatic conveying plays a crucial role in the efficient and safe transport of purified ash. With its ability to provide a dust-free environment, high efficiency, and flexibility, these systems offer significant advantages over traditional material handling methods. Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development and implementation of advanced pneumatic conveying solutions, ensuring that industries can handle purified ash in a manner that is both environmentally responsible and operationally efficient. By leveraging the expertise and technology of HeadPowder, companies can enhance their material handling processes, reduce costs, and improve overall operational performance.