

Role of Airborne Conveying in Yeast Powder Transportation
Yeast powder, a vital component in sectors like food and beverage, pharmaceuticals, and biofuels, requires specialized handling methods to preserve its quality and integrity. Its unique characteristics—such as hygroscopic nature, tendency to agglomerate, and sensitivity to mechanical stress—make traditional bulk material handling techniques inadequate. Airborne conveying, or pneumatic conveying, has become the preferred solution for transporting yeast powder, offering advantages in hygiene, safety, and operational efficiency.
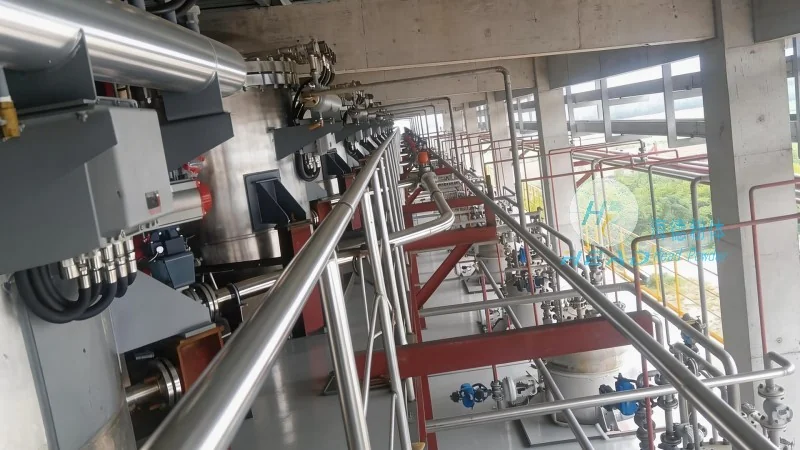
Advantages of Airborne Conveying for Yeast Powder
A key benefit of using air-based systems for yeast powder transport is the creation of a closed, dust-free environment. Unlike mechanical conveyors like belt or screw systems, pneumatic conveying prevents product contamination and minimizes dust emissions, which is critical for maintaining the purity of yeast powder. This sealed system also reduces cross-contamination risks, a top priority in food and pharmaceutical applications where product safety is non-negotiable.
Another significant advantage is the flexibility and scalability of air conveying systems. These systems can be easily adapted to handle varying volumes of yeast powder, from small-scale laboratory use to large-scale industrial production. The modular design allows seamless integration into existing facilities, minimizing downtime and installation costs. Additionally, air conveying enables long-distance transport without multiple transfer points, enhancing operational efficiency and reducing the risk of product degradation from handling.
Challenges in Conventional Yeast Powder Handling
Traditional handling methods often involve manual or semi-automated processes prone to errors and inefficiencies. Manual handling can lead to product loss, contamination, and inconsistent quality. Mechanical conveyors, while common, may not suit yeast powder due to its hygroscopic properties, as they cause moisture accumulation and degradation over time. Moreover, these systems require frequent maintenance and cleaning, increasing operational costs and downtime.
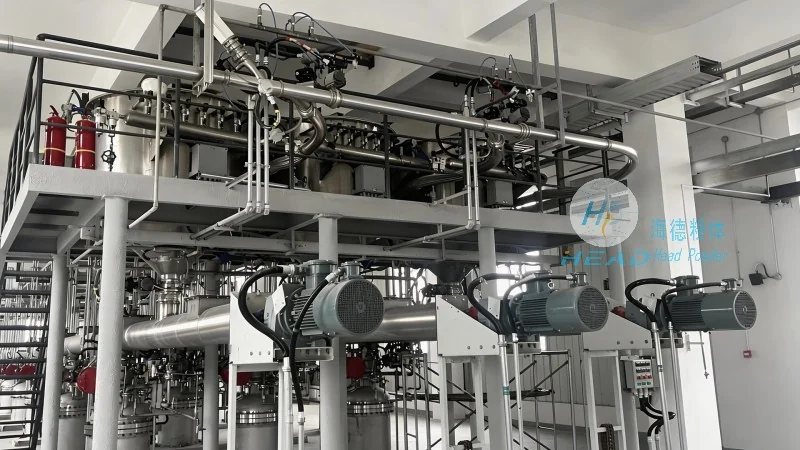
HeadPowder Engineering: Expertise in Air Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., known as HeadPowder, is a leading provider of specialized engineering solutions for bulk material handling, with a focus on pneumatic conveying systems for yeast powder and other sensitive powders. With extensive industry experience, HeadPowder has developed cutting-edge air conveying technologies tailored to yeast powder’s unique requirements. The company’s expertise lies in designing and manufacturing customized systems that ensure optimal performance, reliability, and compliance with industry standards.
HeadPowder’s pneumatic conveying solutions address the specific challenges of yeast powder handling. The systems utilize high-efficiency air pumps and specialized ductwork to ensure smooth, consistent transport, minimizing product degradation and maintaining quality. The company’s engineering team collaborates closely with clients to understand their needs—from production capacity to product characteristics—and designs tailored solutions that meet operational requirements.
Key Features of HeadPowder’s Air Conveying Systems
HeadPowder’s air conveying systems for yeast powder include advanced features that enhance performance and reliability. These include: high-capacity air pumps capable of handling large volumes efficiently; flexible ductwork adaptable to various production layouts; and advanced control systems for precise operation. The systems are designed with hygiene in mind, featuring easy-to-clean components and corrosion-resistant materials to prevent product buildup. This ensures the yeast powder remains in a clean, safe environment throughout the conveying process.
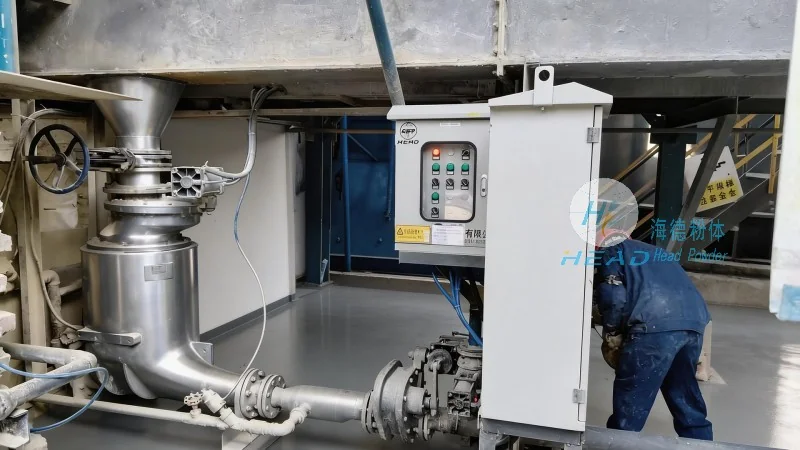
Furthermore, the systems incorporate monitoring and control features for real-time process tracking. This allows operators to identify and resolve issues promptly, ensuring optimal performance and minimizing downtime. Safety features like pressure relief valves and emergency shut-off mechanisms provide additional protection for both the product and personnel.
Applications and Case Studies
HeadPowder’s air conveying systems have been successfully implemented in industries including food processing, pharmaceuticals, and biofuel production. For example, a food facility used the system to transport yeast powder from storage to production lines, improving efficiency and reducing costs while maintaining product quality. In another case, a pharmaceutical company implemented the system for fermentation processes, achieving better moisture control and reducing contamination risks.
Conclusion
Airborne conveying has transformed yeast powder handling by offering superior hygiene, safety, and efficiency. With its closed-loop design and scalability, pneumatic systems are the industry standard for transporting yeast powder. Shandong HeadPowder Engineering Co., Ltd. leads in this technology, providing customized, reliable solutions that meet clients’ unique needs. Through advanced engineering and expertise, HeadPowder enhances the efficiency and safety of yeast powder handling, contributing to success across various sectors.