

What is Cereal Pneumatic Conveying? Classification and Applications of Pneumatic Conveying Systems
Understanding Cereal Pneumatic Conveying: Classification and Practical Applications
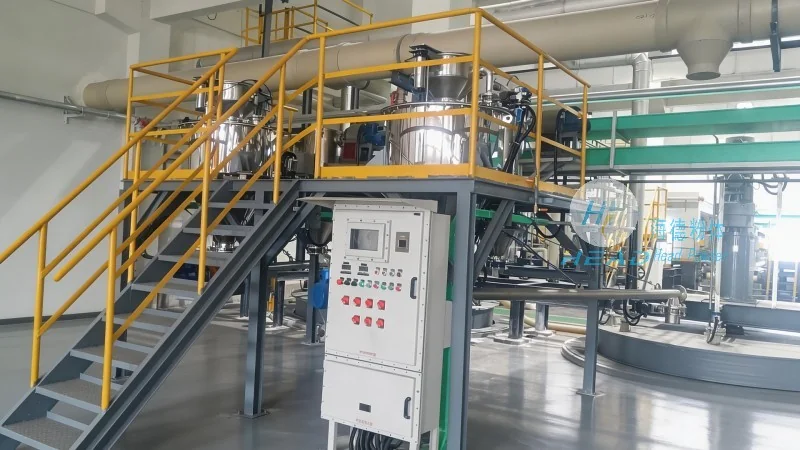
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying solutions for the food processing industry. With a focus on efficiency, hygiene, and reliability, HeadPowder's systems are tailored to handle delicate and high-value products like cereal grains and flakes, ensuring minimal product degradation during transport.
Pneumatic Conveying System Classification
At HeadPowder, we categorize pneumatic conveying systems based on the pressure differential used to move materials. The primary types include vacuum, positive pressure, and combined systems, each suited to different operational requirements and material handling scenarios.
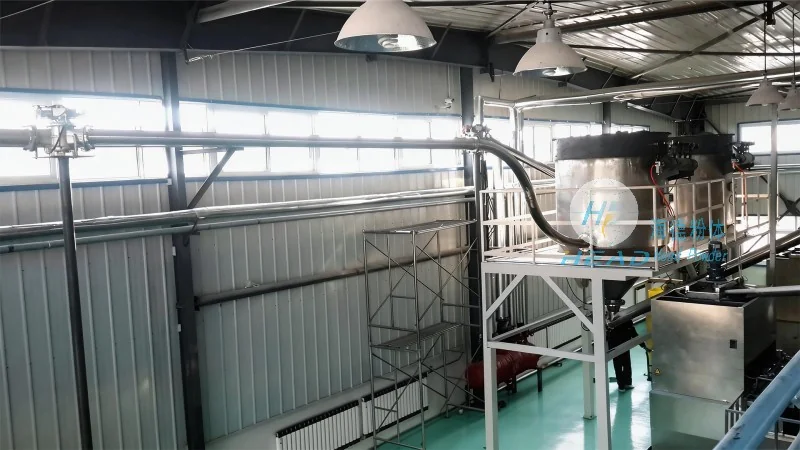
Vacuum Pneumatic Conveying Systems operate by creating a negative pressure (vacuum) in the conveying line, drawing materials from multiple source points into a central collection point. This method is ideal for applications where materials need to be gathered from various locations, such as from bulk storage bins or production lines, and then transported to a central processing or packaging area. The vacuum system ensures gentle handling of delicate cereal products, minimizing breakage and maintaining product integrity.
Positive Pressure Pneumatic Conveying Systems use compressed air to push materials through the conveying line, typically from a single source to multiple destination points. This approach is well-suited for scenarios where materials need to be distributed from a central storage facility to several production lines or packaging stations. The positive pressure system offers high transport rates and can handle a wide range of particle sizes, making it a versatile choice for cereal processing plants.
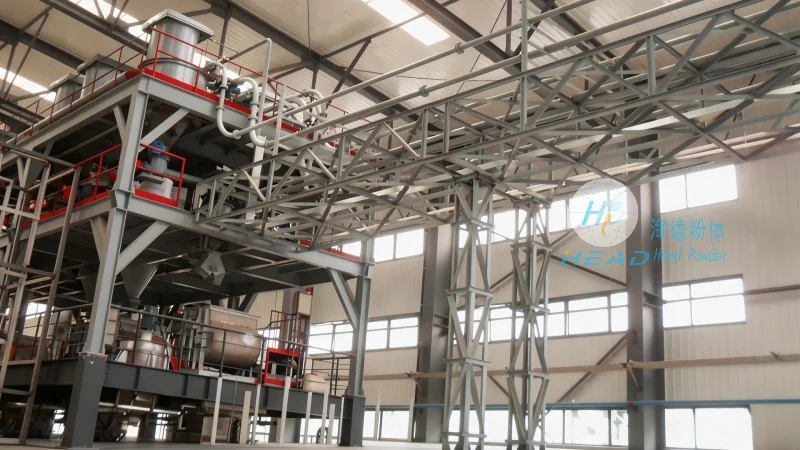
Combined Pneumatic Conveying Systems integrate both vacuum and positive pressure capabilities, allowing for more complex material flow management. These systems are particularly useful in large-scale operations where materials need to be collected from multiple sources and then distributed to multiple destinations. By combining the strengths of both vacuum and positive pressure, combined systems provide flexibility and efficiency, ensuring smooth operation across the entire cereal processing workflow.
Applications in Cereal Processing
HeadPowder's pneumatic conveying solutions are widely applied in the cereal industry to streamline material handling processes. For instance, in a typical cereal production line, raw cereal grains may be stored in bulk silos and then conveyed to a milling or flaking unit using a vacuum system. The processed flakes or powders are then transported to packaging machines via a positive pressure system, ensuring a continuous and hygienic flow of product.
The systems are designed to maintain the quality of the cereal products throughout the conveying process. By using low-velocity air and specialized hopper designs, the equipment minimizes dust generation and prevents product contamination, which is critical for maintaining food safety standards. Additionally, the modular nature of these systems allows for easy integration with existing production lines, reducing downtime and installation costs.
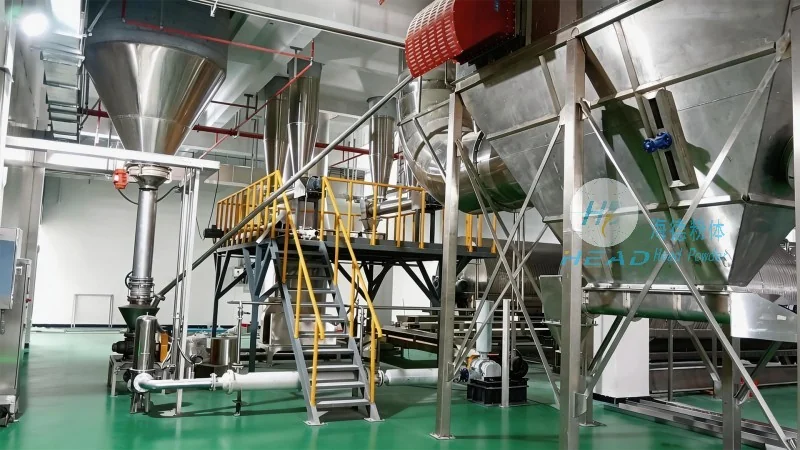
In terms of operational efficiency, pneumatic conveying systems offer significant advantages over traditional mechanical methods. They eliminate the need for multiple transfer points and reduce the risk of material spillage, leading to lower maintenance requirements and higher overall productivity. HeadPowder's engineers work closely with clients to assess their specific needs, selecting the most appropriate system configuration to optimize both performance and cost-effectiveness.
Conclusion
As a trusted provider of pneumatic conveying solutions, HeadPowder leverages its expertise in engineering and material handling to deliver customized systems that meet the unique demands of the cereal industry. By understanding the nuances of different system classifications and their applications, HeadPowder ensures that clients receive reliable, efficient, and cost-effective equipment that enhances their production capabilities. With a strong commitment to quality and customer satisfaction, HeadPowder continues to be a leader in the field, helping businesses in Shandong and beyond improve their material handling processes and maintain competitive advantages in the market.