

Principle of Sulfate Nickel Pneumatic Conveying System
The sulfate nickel pneumatic conveying system is a specialized industrial equipment designed for the efficient and safe transportation of nickel sulfate, a critical raw material widely used in the production of lithium-ion batteries. This system integrates advanced pneumatic conveying technology with robust engineering design to ensure reliable material handling, minimal product degradation, and optimal operational efficiency. As a key component in the battery manufacturing supply chain, the system plays a vital role in maintaining consistent production flow and reducing downtime caused by material handling issues.
System Components and Working Principle
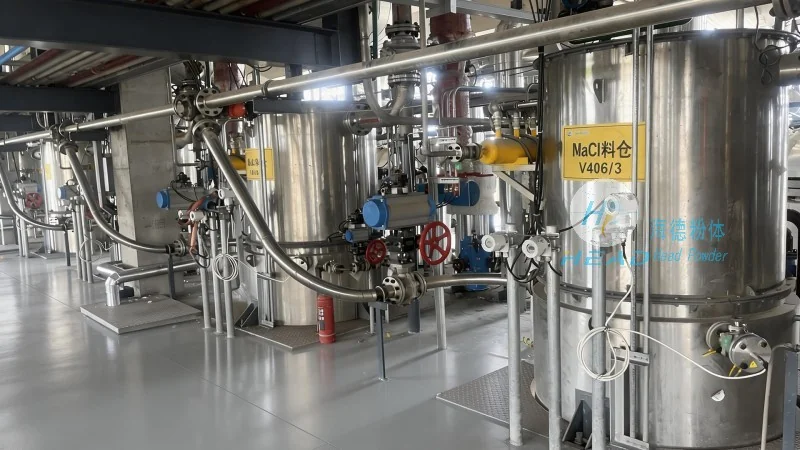
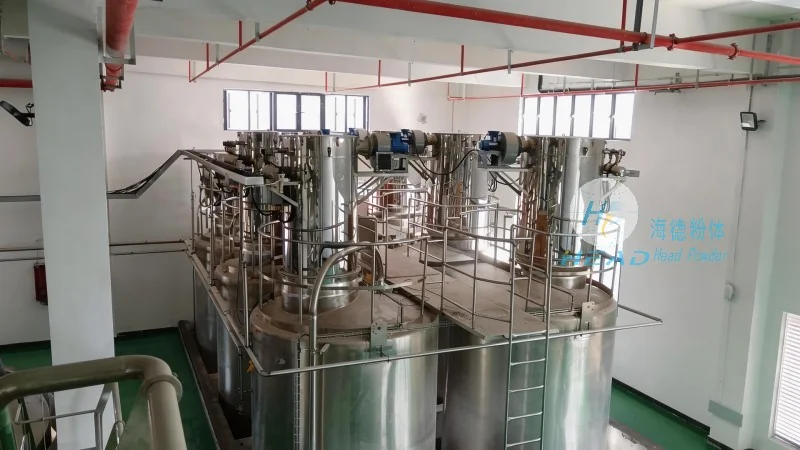
The core components of a typical sulfate nickel pneumatic conveying system include the material feeding unit, air supply system, conveying pipeline network, separation and recovery unit, and control system. The material feeding unit is responsible for accurately metering and feeding the nickel sulfate powder into the system. The air supply system generates the necessary airflow, which can be either positive pressure (blowing) or negative pressure (suction) depending on the specific application requirements. The conveying pipeline network transports the material and air mixture through a network of pipes, often incorporating bends, valves, and other fittings to direct the flow. The separation and recovery unit, such as a cyclone separator or bag filter, separates the material from the air stream, allowing the air to be recirculated or discharged while the nickel sulfate is collected for further processing. The control system monitors and regulates the entire process, ensuring stable operation and preventing issues like blockages or overpressure.
Technical Advantages and Benefits
Compared to traditional mechanical conveying methods, the pneumatic conveying system offers several advantages for handling sulfate nickel. Firstly, it eliminates the need for mechanical components like conveyors or elevators, reducing maintenance costs and minimizing the risk of material contamination. The system is also highly flexible, allowing for easy reconfiguration of the pipeline network to accommodate changes in production needs or facility layout. Additionally, the pneumatic conveying process can be designed to minimize product degradation, which is crucial for sensitive materials like nickel sulfate used in battery production. The system's ability to handle fine powders without caking or agglomeration ensures consistent material quality and reduces the likelihood of equipment blockages. Furthermore, the closed-loop design of the system enhances safety by preventing dust emissions and protecting the environment, aligning with modern industrial standards for sustainability and regulatory compliance.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the company's official name, is a leading engineering solutions provider specializing in the design, manufacturing, and installation of pneumatic conveying systems for various industrial applications. With its headquarters located in Shandong, China, the company leverages over years of industry experience and technical expertise to deliver customized solutions tailored to the unique needs of its clients. HeadPowder's team of engineers and technicians work closely with customers to understand their material handling challenges and develop optimal system configurations that maximize efficiency and reliability. The company's commitment to quality and innovation has established it as a trusted partner in the battery and chemical industries, providing reliable equipment that meets the highest standards of performance and safety.
Application and Conclusion
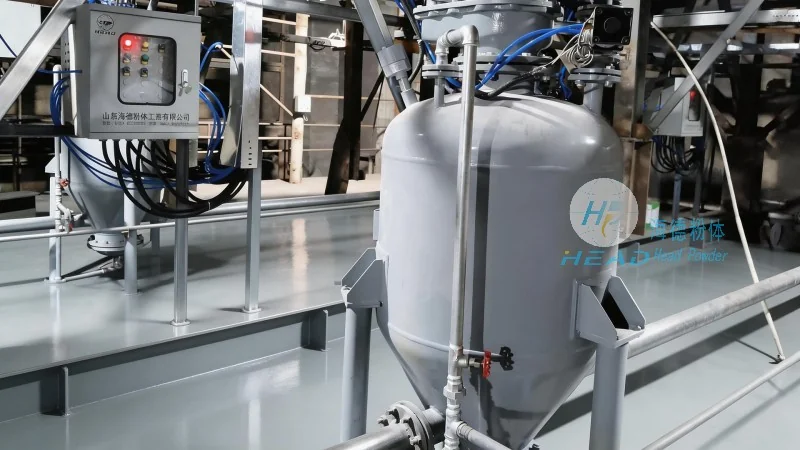
The sulfate nickel pneumatic conveying system is widely used in the battery manufacturing industry, where the efficient handling of nickel sulfate is essential for maintaining production efficiency and product quality. By leveraging pneumatic conveying technology, manufacturers can streamline their material handling processes, reduce operational costs, and improve overall productivity. HeadPowder's expertise in designing and implementing such systems ensures that clients receive tailored solutions that address their specific requirements, from small-scale laboratory applications to large-scale industrial production lines. The system's reliability and durability make it a long-term investment for businesses seeking to enhance their material handling capabilities and stay competitive in the market. With a focus on customer satisfaction and technical excellence, HeadPowder continues to be a key player in providing advanced engineering solutions for the industrial sector.