

Working Principle and Features of Gray Bin Powder Pneumatic Conveying Equipment
Gray bin powder pneumatic conveying equipment is a specialized system designed for the efficient and reliable transportation of powders and bulk materials. This equipment is widely used in various industrial sectors, including chemical, food, pharmaceutical, and cement industries, where the handling of fine or cohesive powders requires precise control and minimal product degradation. The system typically incorporates a gray bin as the primary storage and feeding unit, coupled with a pneumatic conveying pipeline that uses air or gas to move the material from the bin to the discharge point. This approach offers several advantages over traditional mechanical conveying methods, such as reduced maintenance, lower energy consumption, and the ability to handle materials that are difficult to transport through conventional means.
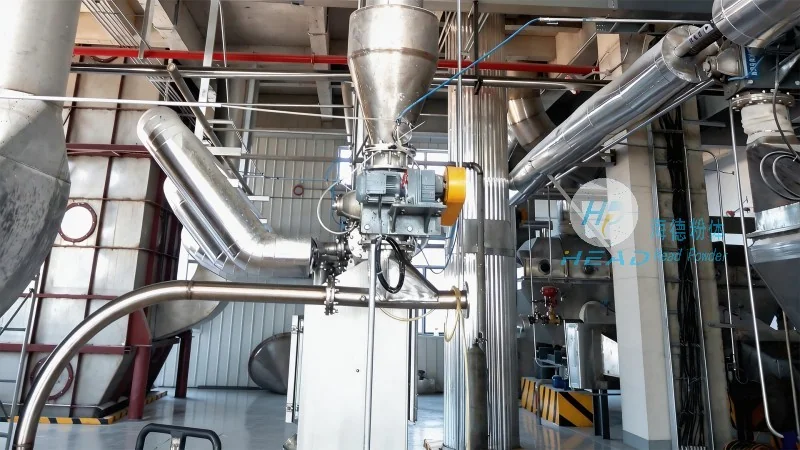
Working Principle of the Gray Bin Powder Pneumatic Conveying System
The operation of the gray bin powder pneumatic conveying equipment is based on the fundamental principle of pneumatic transport, where the material is suspended and carried by a moving air stream within a sealed pipeline. The process begins with the material being discharged from the gray bin into a hopper or feeder, which regulates the flow rate and ensures a consistent feed to the conveying line. A blower or compressor then generates the necessary air pressure and flow, creating a positive or negative pressure environment within the pipeline. In positive pressure systems, air is forced through the material, lifting and transporting it to the destination. In negative pressure systems, air is drawn out of the pipeline, creating a vacuum that pulls the material along. The gray bin, often equipped with a hopper and a discharge valve, serves as the primary source of material, while the conveying line connects the bin to the discharge point, such as a silo, storage tank, or processing unit. The system may also include components like filters, cyclones, and dust collectors to manage the air and prevent contamination, ensuring that the material remains clean and free from moisture or debris.
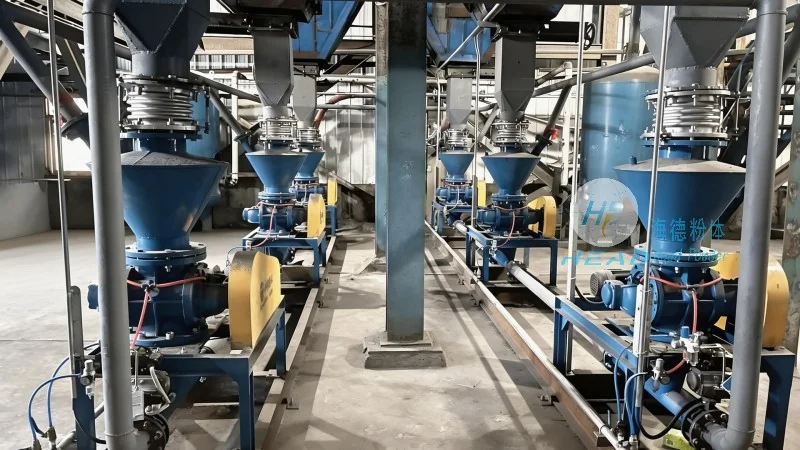
Key Features and Advantages of Gray Bin Powder Pneumatic Conveying Equipment
One of the primary features of this equipment is its ability to handle a wide range of powder characteristics, including fine powders, cohesive materials, and materials with high moisture content. The gray bin design allows for large storage capacities, providing a buffer between production and processing, which helps to stabilize the flow and reduce downtime. The pneumatic conveying system offers flexibility in terms of layout, as the pipeline can be installed in various configurations, including vertical, horizontal, or a combination of both, to accommodate different plant layouts and operational requirements. Another key feature is the low maintenance requirement, as there are fewer moving parts compared to mechanical conveyors, which reduces the risk of wear and tear and extends the equipment's service life. The system also provides better control over the material flow, allowing for precise dosing and regulation, which is crucial in applications where accurate material measurement is essential. Additionally, the enclosed nature of the system helps to prevent dust emissions and environmental contamination, making it more environmentally friendly and compliant with regulatory standards. The use of air as the conveying medium also minimizes product contamination, as the material is not in direct contact with metal or other surfaces that could introduce impurities. Furthermore, the system can be integrated with other processing equipment, such as mixers, dryers, or reactors, to form a complete production line, enhancing overall operational efficiency.
Applications and Industries Served by Gray Bin Powder Pneumatic Conveying Equipment
Gray bin powder pneumatic conveying equipment is widely used in various industries due to its versatility and effectiveness. In the chemical industry, it is commonly employed for the transport of raw materials, intermediates, and finished products, such as powders used in pharmaceuticals, fertilizers, and plastics. The food and beverage industry utilizes this equipment for handling ingredients like flour, sugar, and spices, ensuring that the products remain fresh and free from contamination. The pharmaceutical industry relies on the system for the transport of active pharmaceutical ingredients (APIs) and other sensitive materials, where maintaining product purity and sterility is paramount. In the cement industry, the equipment is used for the conveying of raw materials and finished cement, contributing to the efficiency of the production process. Other applications include the handling of minerals, ceramics, and agricultural products, where the equipment's ability to handle cohesive and fine powders is advantageous. The system's adaptability makes it suitable for both small-scale and large-scale operations, from laboratory settings to industrial plants, providing a reliable solution for material handling needs.
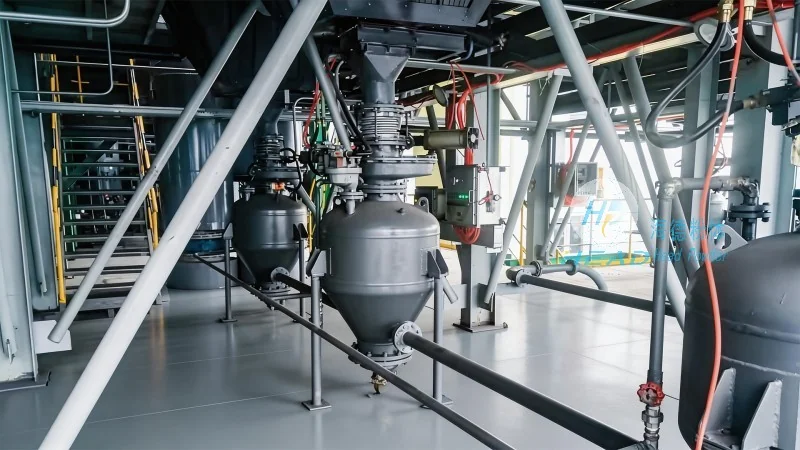
Conclusion and Company Information
Gray bin powder pneumatic conveying equipment offers a robust and efficient solution for the transportation of powders and bulk materials in various industrial applications. The system's working principle, based on pneumatic transport, provides advantages such as low maintenance, flexibility, and minimal product contamination. Its key features, including large storage capacity, precise flow control, and environmental friendliness, make it an ideal choice for industries that require reliable and consistent material handling. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd., based in China, specializes in the design, manufacturing, and supply of high-quality pneumatic conveying systems tailored to meet the specific needs of different industries. With a focus on innovation and quality, the company ensures that its equipment meets the highest standards of performance and reliability, providing customers with a durable and efficient solution for their material handling challenges. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the industry, offering comprehensive support and after-sales services to ensure the long-term operation of the equipment.