

Working Principle and Features of Paper Sheet Powder Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling paper sheet powders. Our equipment is engineered to meet the specific demands of industries requiring efficient, reliable, and clean material transport solutions. This article delves into the working principle and key features of our paper sheet powder pneumatic conveying machines, providing insights into their operational efficiency and practical applications.
Working Principle of the Pneumatic Conveying System
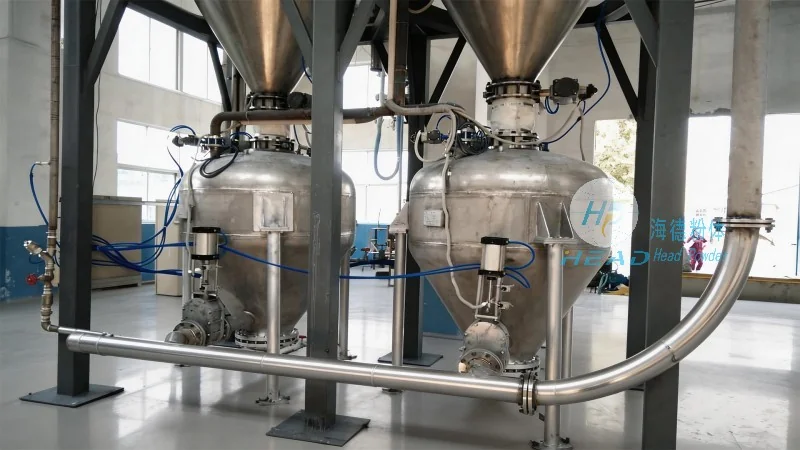
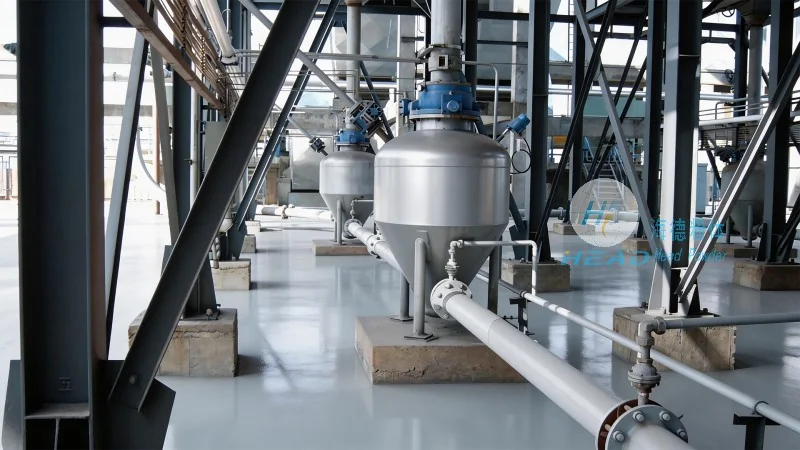
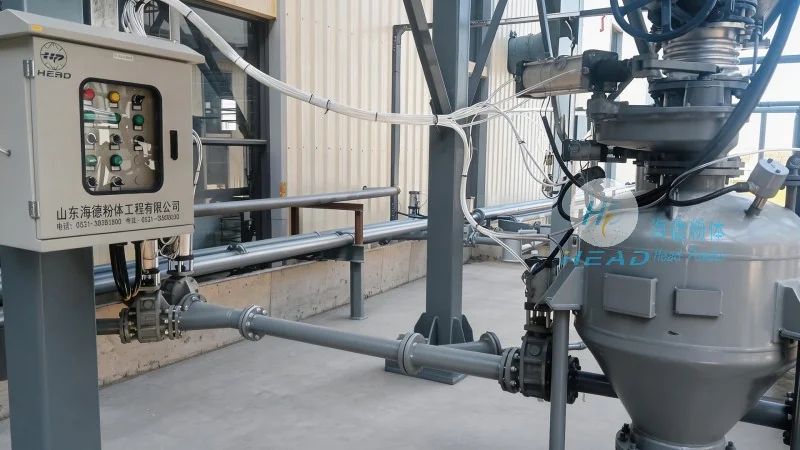
The core mechanism of the paper sheet powder pneumatic conveying equipment involves the use of compressed air to transport dry powders through a pipeline. The system operates by creating a pressure differential between the material feed point and the discharge point. As compressed air is introduced into the conveying line, it generates a flow that draws the powder particles into the pipeline. The air and powder mixture then travels through the system, with the air acting as the medium to move the material. The process typically includes a hopper for material storage, a rotary valve for controlled discharge, and a series of pipes that guide the material to its destination. The design ensures that the powder is conveyed without the need for mechanical components like belts or buckets, minimizing wear and maintenance requirements. The compressed air is supplied by an air compressor, which maintains a consistent pressure throughout the system. The air flow rate is adjustable, allowing users to control the conveying speed based on the material's characteristics and the required distance. The system also incorporates air filters to remove contaminants from the compressed air, ensuring that the conveyed powder remains clean and free from impurities.
Key Features of the Paper Sheet Powder Pneumatic Conveying Machine
Our paper sheet powder pneumatic conveying equipment is characterized by several notable features that enhance its performance and usability. Firstly, the system offers a high degree of flexibility in terms of material handling, as it can transport various types of powders, including those with different particle sizes and moisture content. The use of compressed air allows for a clean and dust-free operation, which is particularly important in industries where contamination control is critical, such as food processing or pharmaceutical manufacturing. Additionally, the equipment is designed for low maintenance, with components like the rotary valve and air filters being easily accessible for routine checks and replacements. The system also provides adjustable conveying rates, enabling users to control the flow rate based on specific operational needs. Furthermore, the compact design of the machine makes it suitable for installation in limited spaces, while the robust construction ensures long-term durability and reliability. The machine is equipped with safety features, including pressure relief valves and overload protection, to prevent accidents and ensure safe operation. The control system is user-friendly, with intuitive interfaces that allow operators to monitor and adjust the conveying process easily.