

Working Principle and Features of Pneumatic Conveying Equipment for Ash Tank Truck Materials
For industrial applications involving the transportation of bulk materials, especially in the context of ash handling from power plants or similar facilities, pneumatic conveying equipment for ash tank trucks plays a crucial role. This equipment is designed to efficiently transfer ash and other fine particulate materials from storage silos or processing units to the ash tank trucks. The following sections will explore the working principle and key features of such equipment, highlighting its operational efficiency and practical advantages.
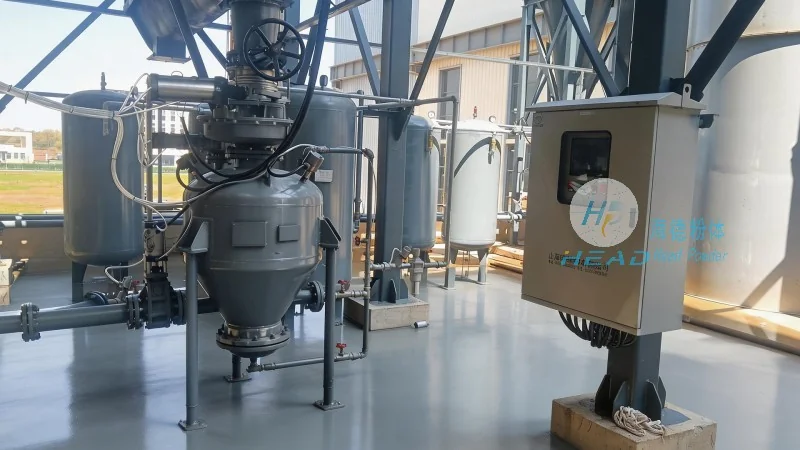
Working Principle of Pneumatic Conveying Equipment for Ash Tank Trucks
The core of pneumatic conveying for ash tank trucks is the use of compressed air or gas to move material through a pipeline system. The process typically involves several key components and steps. First, the ash material is fed into a hopper or feeder that controls the flow rate. From there, the material is introduced into a pipeline where it is mixed with the air stream. The air, often under pressure, propels the material along the pipeline, ensuring it reaches the ash tank truck. The system may use either positive pressure (where air pushes the material) or negative pressure (where air is drawn through the material), depending on the specific design and application requirements. The equipment includes components such as air compressors, dust filters, and control valves to regulate the air flow and material transport. The entire process is automated to maintain consistent material flow and prevent blockages or system failures.
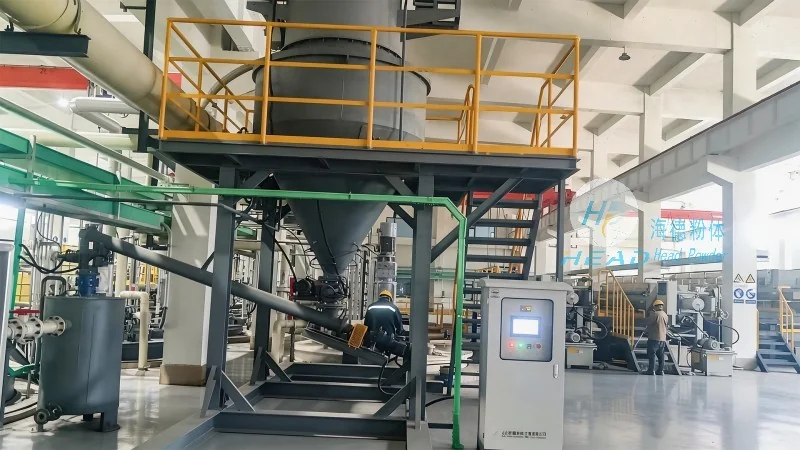
Key Features of Pneumatic Conveying Equipment for Ash Tank Trucks
Several distinct features make pneumatic conveying equipment for ash tank trucks an effective solution for material handling. Firstly, it offers a dust-free operation, which is critical in environments where air quality and worker safety are paramount. Unlike traditional methods like bucket elevators or belt conveyors, pneumatic systems minimize dust generation, reducing the risk of respiratory issues and improving overall workplace conditions. Secondly, the equipment provides high flexibility in terms of layout and installation. It can be configured to handle various distances and angles, adapting to the spatial constraints of industrial sites. This flexibility allows for efficient integration with existing infrastructure without the need for extensive modifications. Thirdly, the system is highly efficient in terms of energy consumption and material throughput. By using compressed air to move material, it achieves a high material-to-air ratio, meaning less energy is required per unit of material transported compared to other methods. This efficiency translates into lower operational costs and reduced environmental impact. Additionally, the equipment is designed for durability and reliability, with components built to withstand the abrasive nature of ash and other fine materials. Regular maintenance and robust construction ensure long service life and minimal downtime, which is essential for continuous operation in industrial settings.
Operational Advantages and Practical Applications
The operational advantages of pneumatic conveying equipment for ash tank trucks extend beyond the basic features discussed. One significant benefit is the ability to handle a wide range of material characteristics, including different particle sizes, moisture contents, and bulk densities. This versatility makes the system suitable for various applications, from small-scale power plants to large industrial facilities. Another advantage is the reduced need for manual labor, as the equipment operates automatically, minimizing the risk of human error and improving safety. The system also allows for precise control over material flow rates, ensuring consistent delivery to the ash tank trucks. This control is crucial for maintaining the operational efficiency of downstream processes, such as ash disposal or further processing. In practical applications, this equipment is commonly used in power generation plants, where ash from coal combustion needs to be transported to storage or disposal sites. The equipment's ability to handle large volumes of ash efficiently and safely makes it an indispensable part of modern industrial operations.
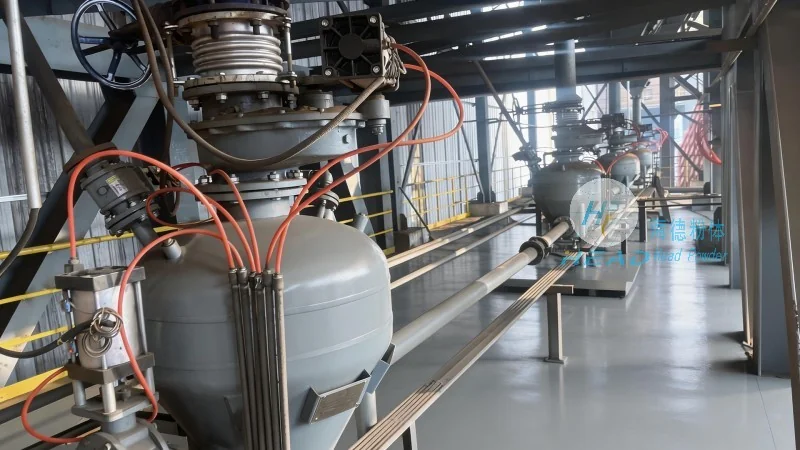
Conclusion and Company Information
In conclusion, pneumatic conveying equipment for ash tank trucks is a sophisticated and efficient solution for the transportation of bulk materials in industrial settings. Its working principle, based on compressed air to move material through pipelines, combined with key features like dust-free operation, flexibility, and high efficiency, makes it a preferred choice for many facilities. The operational advantages and practical applications highlight its importance in modern industrial processes. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such equipment, ensuring high-quality, reliable solutions tailored to the specific needs of clients. With a focus on durability, efficiency, and safety, the company's products contribute to the smooth operation of industrial facilities, supporting the effective handling and transportation of ash and other materials. Based in Shandong, China, HeadPowder Engineering Co., Ltd. continues to innovate and provide advanced solutions for material handling challenges in various industries.