

Working Principle and Features of Silica Fume Material Pneumatic Conveying Systems
HeadPowder, a prominent engineering firm headquartered in Shandong, China, specializes in the development and implementation of advanced material handling systems. A key offering from this company is the silica fume material pneumatic conveying system, a sophisticated solution designed to efficiently transport fine powders such as silica fume across industrial facilities.
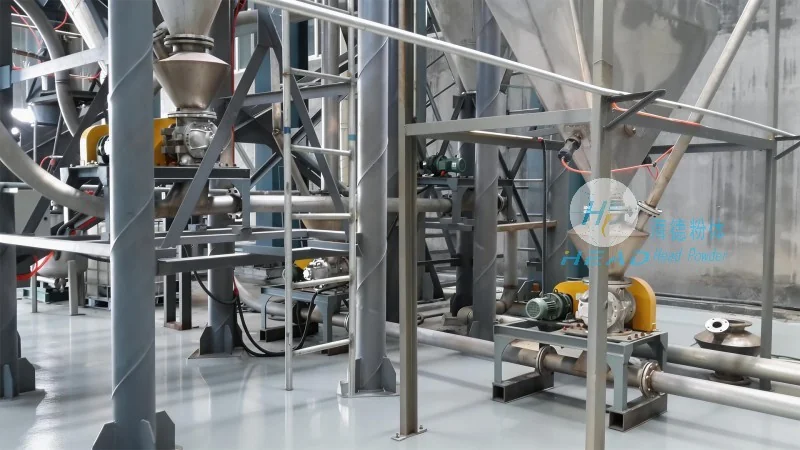
Exploring the Working Principle of Silica Fume Pneumatic Conveying Systems
The fundamental operation of a silica fume pneumatic conveying system revolves around the use of compressed air or gas as the primary medium to move dry powders through a sealed pipeline. This process integrates several critical components and operational steps to ensure reliable and efficient material transport. The system typically comprises a material feeder, a conveying pipeline, a dust collection unit, and a control system. The material feeder, often a rotary valve or screw feeder, introduces silica fume into the system at a controlled rate. Compressed air is then introduced into the pipeline, creating a flow that propels the silica fume particles through the system. The air velocity is meticulously managed to maintain a consistent flow rate and prevent particle deposition or blockages within the pipeline. At the receiving end, a dust collector captures any fine particles that may escape, ensuring environmental compliance and maintaining product purity. The control system continuously monitors and adjusts air pressure, flow rate, and material feed rate to optimize performance and prevent system malfunctions.
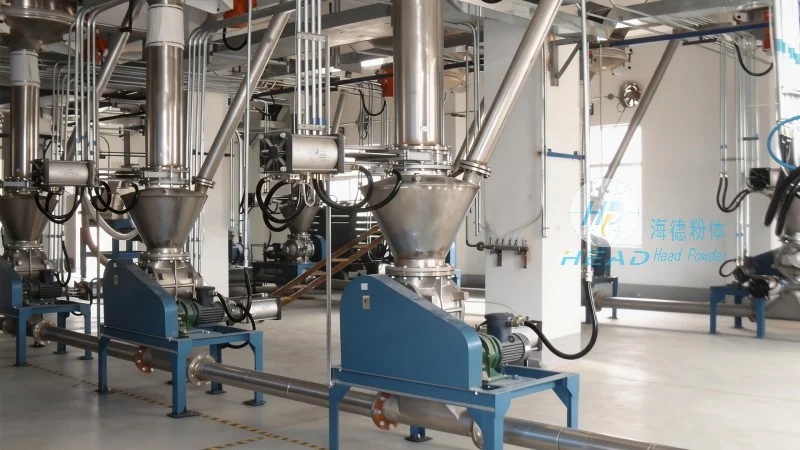
Key Features and Advantages of Silica Fume Pneumatic Conveying Systems
HeadPowder's silica fume pneumatic conveying systems are engineered with several distinctive features that enhance performance and reliability. One of the primary advantages is the ability to transport fine powders over extended distances without relying on mechanical components like belts or buckets, which can be susceptible to wear and maintenance issues. The system's design minimizes product degradation and contamination by keeping the material enclosed within a pipeline, protecting it from moisture, dust, and external pollutants. Additionally, the system offers high efficiency in energy consumption, as it utilizes compressed air efficiently to move the material, reducing operational costs compared to traditional methods. The modular design allows for seamless integration into existing industrial setups and flexible expansion as production requirements evolve. Another notable feature is the system's adaptability to varying material properties, including different particle sizes and moisture content, making it versatile for diverse industrial applications. The closed-loop operation also contributes to improved safety by containing dust and reducing worker exposure, aligning with modern industrial safety standards.
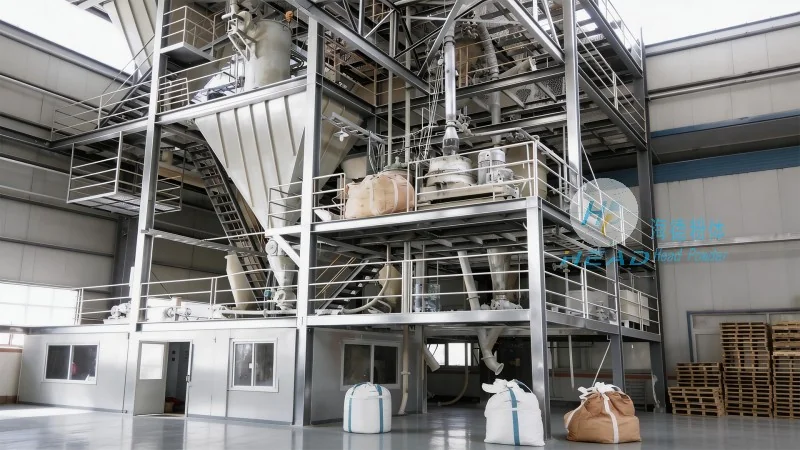
Application-Specific Benefits and Performance Metrics
The silica fume pneumatic conveying systems from HeadPowder are tailored to meet the specific demands of various industries, including cement, concrete, and chemical manufacturing. In cement production, the system efficiently transports silica fume to the mixing plant, ensuring consistent quality and reducing the risk of material segregation. The high conveying velocity and low pressure drop in the system minimize energy consumption while maintaining a high material throughput rate. For concrete production, the system helps maintain the uniformity of the silica fume blend, which is crucial for achieving desired strength and durability characteristics. The system's ability to handle fine powders without clogging or blockages is particularly beneficial in applications where material flow consistency is critical. Performance metrics such as conveying capacity, pressure drop, and energy efficiency are optimized through advanced design and engineering, ensuring that the system meets or exceeds industry standards. The system's reliability is further enhanced by regular maintenance and quality control measures implemented by HeadPowder, ensuring long-term operational stability and minimal downtime.
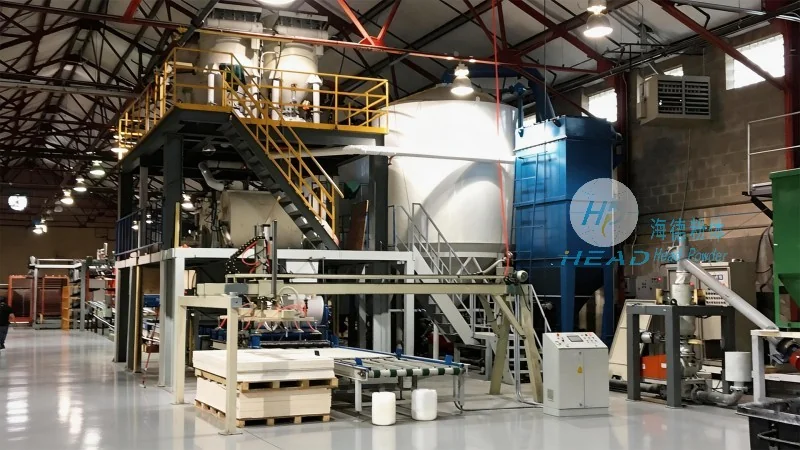
Conclusion: Selecting the Right Pneumatic Conveying Solution for Silica Fume Handling
When choosing a pneumatic conveying system for silica fume handling, it is essential to consider factors such as material properties, conveying distance, and operational efficiency. HeadPowder's expertise in engineering and manufacturing provides a comprehensive solution that addresses these needs effectively. The company's commitment to quality, reliability, and customer satisfaction ensures that their silica fume pneumatic conveying systems are a dependable choice for industrial applications. By leveraging advanced technology and rigorous testing, HeadPowder delivers systems that not only meet current industry requirements but also adapt to future technological advancements. For businesses in need of efficient and reliable silica fume handling solutions, HeadPowder's pneumatic conveying systems offer a proven and effective approach to optimizing material transport processes.