

Operation Process and Working Principle of Chocolate Pneumatic Conveying
Chocolate pneumatic conveying systems are sophisticated industrial solutions designed to efficiently transport chocolate powders, liquids, and other related materials within manufacturing facilities. These systems leverage the principles of pneumatic technology to move products with precision and minimal contamination, making them indispensable in the confectionery industry. The operation process and working principle of such systems involve a series of carefully orchestrated steps that ensure optimal performance and product integrity.
Key Components of Chocolate Pneumatic Conveying Systems
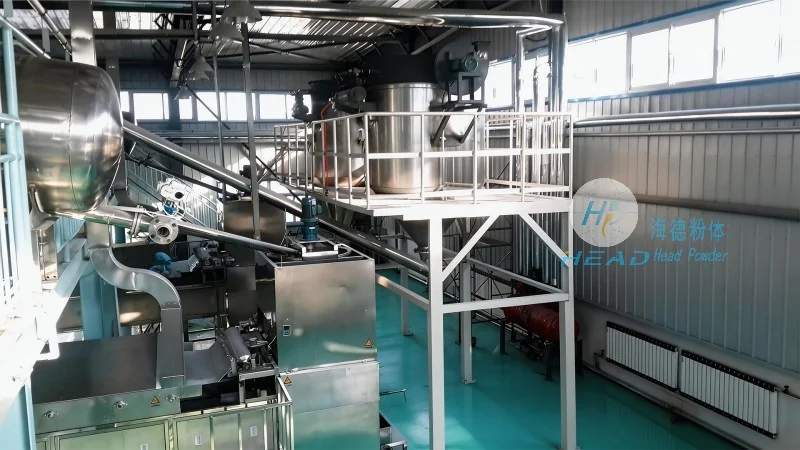
At the core of a chocolate pneumatic conveying system are several critical components that work in tandem to facilitate material transport. These include the hopper or feeding unit, which holds the chocolate material; the air compressor or blower that generates the necessary airflow; the conveying pipes or hoses that carry the material; and the separation or collection equipment that ensures the product is delivered to its intended destination. Each component plays a vital role in maintaining the system's efficiency and reliability.
The Operation Process of Chocolate Pneumatic Conveying
The operation process of a chocolate pneumatic conveying system begins with the loading of the chocolate material into the hopper. As the material is fed into the system, the air compressor starts operating, creating a pressure differential that draws the material into the conveying pipes. The air flow, combined with the material's density and the design of the system, ensures that the chocolate moves smoothly through the pipes. The system may employ various techniques such as positive or negative pressure to control the flow rate and prevent blockages. The material is then transported to the collection point, where it is separated from the air and stored or processed further. This process is typically automated, allowing for consistent and continuous operation, which is crucial in high-volume chocolate production environments.
Working Principle of Chocolate Pneumatic Conveying
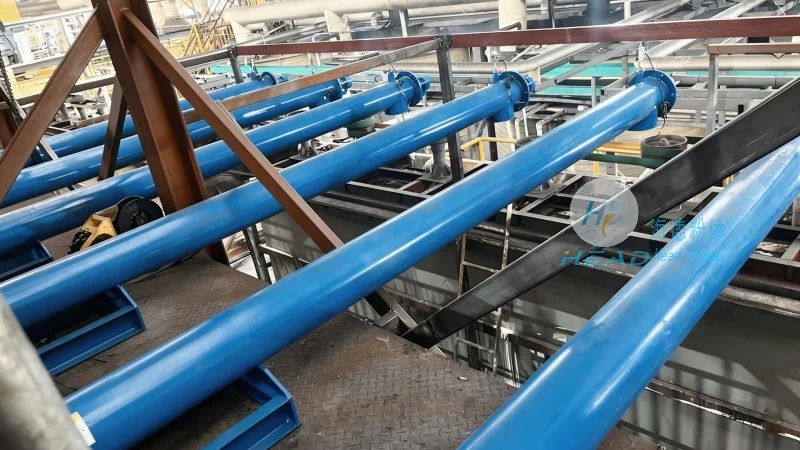
The working principle of chocolate pneumatic conveying systems is based on the fundamental concept of using air to move solid materials. In positive pressure systems, the air compressor forces air into the conveying line, creating a pressure higher than the ambient air. This pressure pushes the chocolate material forward through the pipes. In negative pressure systems, the air is drawn out of the line, creating a vacuum that pulls the material into the system. The choice between positive and negative pressure depends on factors such as the material's properties, the system's layout, and the desired flow rate. The system's design, including the size and shape of the pipes, the angle of the conveying line, and the use of bends or elbows, all contribute to the efficient movement of the chocolate. Additionally, the system may incorporate features like cyclones or filters to separate the material from the air, ensuring that the chocolate remains in a clean and usable state.
Benefits of Using Chocolate Pneumatic Conveying Systems
Implementing chocolate pneumatic conveying systems offers numerous benefits to manufacturers. These systems provide a hygienic and contamination-free method of transporting chocolate, which is essential for maintaining product quality and meeting regulatory standards. They also offer flexibility in system design, allowing for customization to fit specific production needs and facility layouts. The automated nature of these systems reduces labor costs and increases operational efficiency, as they can operate continuously without the need for constant manual intervention. Furthermore, pneumatic conveying systems are energy-efficient compared to traditional mechanical conveyors, as they use less power while achieving higher throughput. These advantages make chocolate pneumatic conveying systems a preferred choice for modern confectionery production.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of industrial conveying solutions, including chocolate pneumatic conveying systems. With a focus on innovation and quality, the company has established itself as a trusted partner in the confectionery industry. HeadPowder's expertise lies in designing and manufacturing systems that meet the unique requirements of chocolate production, ensuring that clients receive reliable and efficient equipment. The company's headquarters are located in Shandong, China, where it leverages advanced technology and skilled engineering to deliver top-tier solutions. By combining years of experience with cutting-edge design, HeadPowder continues to set industry standards for chocolate pneumatic conveying systems.
Conclusion
Chocolate pneumatic conveying systems represent a sophisticated and efficient solution for transporting chocolate materials in industrial settings. The operation process, which involves loading, air compression, material transport, and collection, is carefully engineered to ensure optimal performance. The working principle, based on pneumatic technology, offers flexibility and reliability, making these systems suitable for various production scales. With the support of companies like Shandong HeadPowder Engineering Co., Ltd., manufacturers can enhance their production processes, improve product quality, and achieve greater operational efficiency. As the confectionery industry continues to evolve, the importance of advanced conveying systems like these will only grow, ensuring that chocolate production remains both effective and sustainable.