

Operation Process and Working Principle of Coal and Coke Powder Conveyors
Coal and coke powder conveying equipment serves as a vital component in industrial material handling, facilitating the efficient transportation of fine powders like coal and coke. These systems are engineered to handle bulk materials with high reliability and performance, ensuring smooth operation in diverse industrial settings. The following content will explore the operation process and working principle of coal and coke powder conveyors, offering a comprehensive overview of their functionality and practical applications.
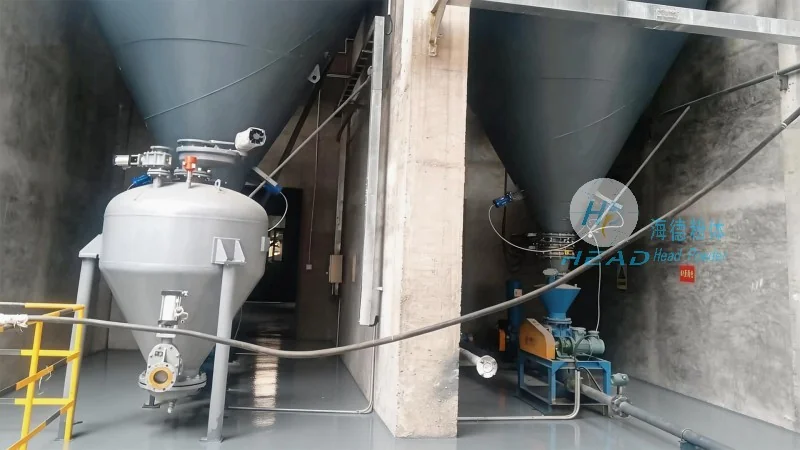
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in bulk material handling solutions, specializes in developing and producing advanced powder conveying systems. The company, headquartered in Shandong, China, is committed to innovation and quality, delivering reliable equipment tailored to meet the needs of industrial clients. With a focus on technical excellence and customer satisfaction, HeadPowder leverages its expertise to create efficient and durable coal and coke powder conveyors that enhance operational efficiency in various industrial processes.
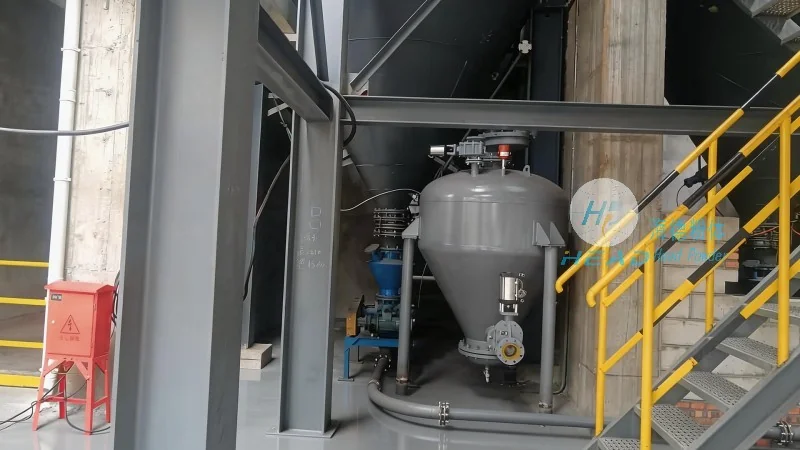
The Operation Process of Coal and Coke Powder Conveyors
The operation of coal and coke powder conveyors involves a systematic sequence of steps to ensure continuous and efficient material transport. The process starts with the loading of the powder into the hopper or inlet of the conveyor system. Once loaded, the material is fed into the main body of the conveyor, where it is transported through a series of components designed to handle fine powders effectively. Depending on the system design, mechanisms such as screw conveyors, belt conveyors, or pneumatic systems may be utilized to move the material. The conveyor ensures consistent flow and minimal material loss, maintaining the integrity of the powder and preventing clogging or blockages. The control system monitors the conveyor's performance, adjusting parameters as needed to optimize efficiency and safety. This integrated approach guarantees reliable operation, meeting the demands of industrial production and material handling requirements.
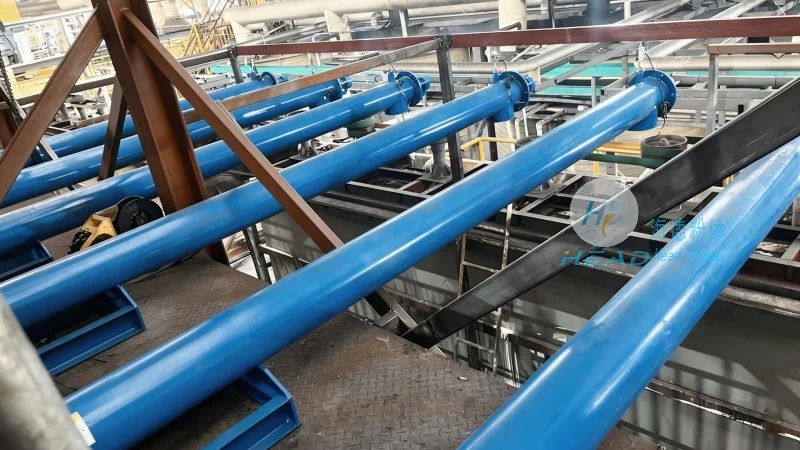
Working Principle of Coal and Coke Powder Conveyors
The working principle of coal and coke powder conveyors centers on the efficient movement of fine particles through mechanical or pneumatic means. Mechanical conveyors, such as screw or belt systems, utilize rotating components to propel the powder along a channel or belt. For example, a screw conveyor employs a rotating screw to push the material forward, while a belt conveyor relies on a moving belt to transport the material. In pneumatic conveying systems, the powder is carried by a stream of air or gas, creating a flow that transports the material through pipes or ducts. The design of the conveyor is tailored to the powder's properties, including particle size, moisture content, and density, to ensure optimal performance. The system incorporates sealing mechanisms, dust collection, and material separation to maintain cleanliness and prevent contamination. By understanding these principles, users can appreciate the efficiency and reliability of coal and coke powder conveyors in handling fine materials in industrial applications.
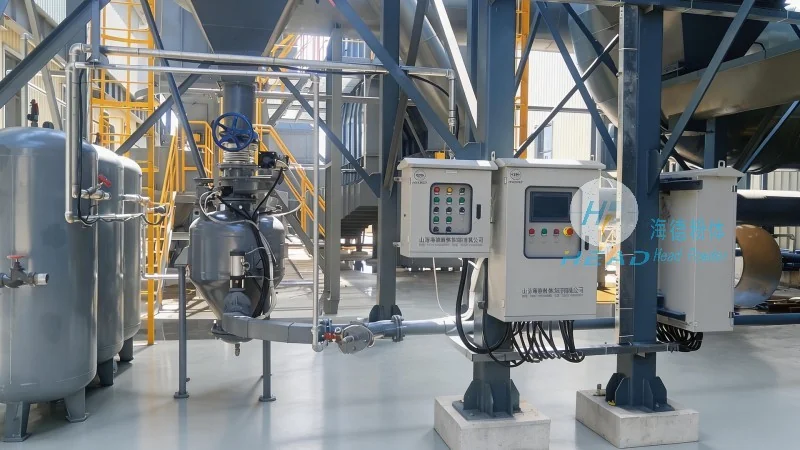
Key Features and Benefits of Coal and Coke Powder Conveyors
Coal and coke powder conveyors from HeadPowder are equipped with several key features that enhance their performance and usability. These include robust construction to withstand the demands of industrial environments, adjustable speed controls for precise material handling, and integrated safety systems to prevent accidents. The conveyors are designed for low maintenance, reducing downtime and operational costs. Additionally, the systems are compatible with various material types, making them versatile for different industrial applications. The benefits of using these conveyors include improved efficiency in material transport, reduced labor costs, and enhanced safety in handling fine powders. By leveraging advanced technology and quality materials, HeadPowder ensures that its conveyors deliver consistent performance and reliability in coal and coke powder handling.