

Operating Process and Working Principle of Sulfur Tablet Powder Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the powder handling industry, specializes in the design, manufacturing, and installation of advanced powder conveying systems. The company, commonly known as headpowder, is headquartered in Shandong, China, and has built a strong reputation for delivering reliable and efficient solutions tailored to the needs of various industrial sectors.
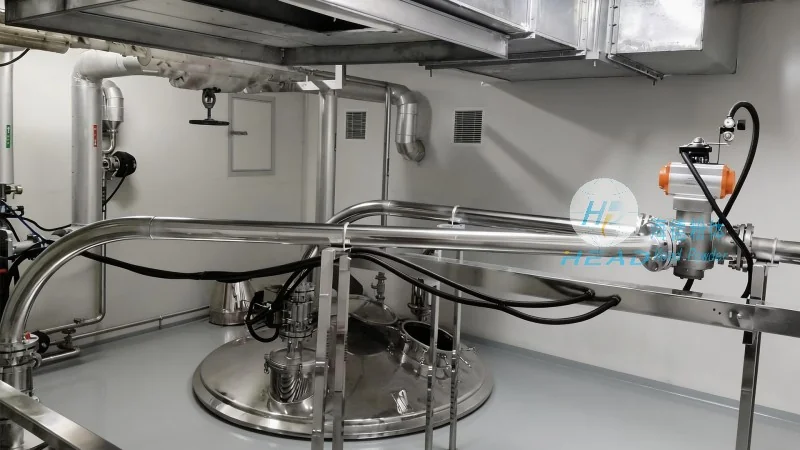
Overview of the Sulfur Tablet Powder Conveying System
The sulfur tablet powder conveying system is a specialized piece of equipment engineered to handle the transportation of sulfur tablets, a critical raw material in many industrial applications. This system combines precision engineering with advanced control technologies to ensure safe, efficient, and consistent powder transfer. The system is designed to meet the stringent requirements of industries such as chemical manufacturing, pharmaceuticals, and food processing, where the quality and integrity of the powder are paramount.
Key Components of the Conveying System
The sulfur tablet powder conveying system typically consists of several key components that work in tandem to achieve seamless operation. These include a hopper for material storage, a feeder to regulate the flow of tablets, a conveyor mechanism (such as a screw conveyor or pneumatic system) for transporting the powder, and a control panel to monitor and adjust the system parameters. Each component is carefully selected and integrated to ensure optimal performance and minimal downtime.
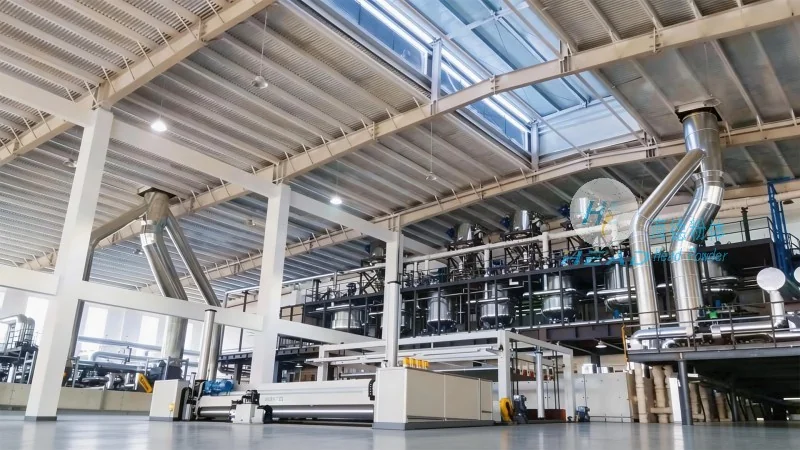
Operating Process of the Sulfur Tablet Powder Conveying System
The operation of the sulfur tablet powder conveying system begins with the loading of sulfur tablets into the hopper. The feeder then controls the discharge rate of the tablets from the hopper, ensuring a steady and controlled flow into the conveyor. The conveyor mechanism then transports the tablets through the system, delivering them to the desired destination, such as a processing unit or storage silo. Throughout the process, the control panel continuously monitors parameters like flow rate, pressure, and temperature to maintain optimal conditions. The system is equipped with safety features, including overload protection and emergency stop mechanisms, to prevent accidents and ensure the safety of operators.
Working Principle of the Sulfur Tablet Powder Conveying System
The working principle of the sulfur tablet powder conveying system is based on the principles of mechanical and pneumatic powder handling. The system utilizes a combination of gravity and mechanical force to move the tablets through the conveyor. The feeder regulates the flow by adjusting the speed of the rotating blades or screws, which pushes the tablets forward. The conveyor mechanism, whether a screw or pneumatic system, provides the necessary force to transport the powder over long distances. The control panel uses sensors and feedback mechanisms to adjust the system's operation in real-time, ensuring that the flow rate and pressure remain within the optimal range. This closed-loop control system enhances the system's efficiency and reliability, minimizing the risk of material loss or system failure.
Advantages of the Sulfur Tablet Powder Conveying System
The sulfur tablet powder conveying system offers several advantages that make it an ideal choice for industrial applications. Firstly, it provides a dust-free and hygienic environment, which is crucial for industries where contamination must be avoided. The system's design minimizes the generation of dust, reducing the risk of respiratory issues for operators and preventing product contamination. Secondly, the system is highly efficient, with minimal energy consumption and low maintenance requirements. The use of advanced materials and components ensures long service life and reduced downtime. Thirdly, the system is flexible and can be customized to meet specific operational requirements, such as varying flow rates or material types. This adaptability makes it suitable for a wide range of applications, from small-scale production to large-scale industrial operations.
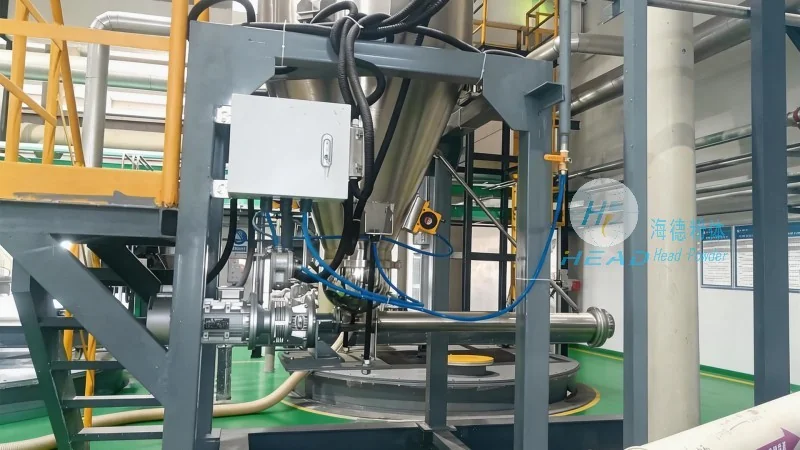
Application Scenarios
The sulfur tablet powder conveying system is widely used in various industrial sectors. In the chemical industry, it is used to transport sulfur tablets to reactors and processing units, ensuring a consistent supply of raw material. In the pharmaceutical industry, the system is employed to handle sulfur tablets used in the production of medications, maintaining the purity and quality of the final product. In the food processing industry, the system is utilized to transport sulfur tablets used as preservatives or flavor enhancers, ensuring compliance with food safety regulations. The system's ability to handle sensitive materials with precision makes it a valuable asset in these and other industries.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. has developed a highly efficient and reliable sulfur tablet powder conveying system that meets the demanding requirements of modern industrial applications. The system's advanced design, precise control, and safety features make it an ideal solution for transporting sulfur tablets with minimal risk and maximum efficiency. By leveraging the expertise of headpowder, industries can enhance their production processes, improve product quality, and ensure compliance with industry standards. The sulfur tablet powder conveying system represents a significant advancement in powder handling technology, offering a robust and versatile solution for the transportation of sensitive materials.