

Operation Process and Working Principle of Fully Automatic Bag Opening Material Handling System Equi
The fully automatic bag opening material handling system is a sophisticated piece of industrial equipment designed to streamline the process of unpacking and transporting bulk materials from sealed bags. This system integrates advanced automation technologies to ensure efficient, safe, and consistent operation in various industrial settings. Developed by Shandong HeadPowder Engineering Co., Ltd., based in China, this equipment represents a significant advancement in material handling solutions, particularly for industries dealing with powders, granules, or other bulk materials that require precise and controlled handling.
Operation Process of the System
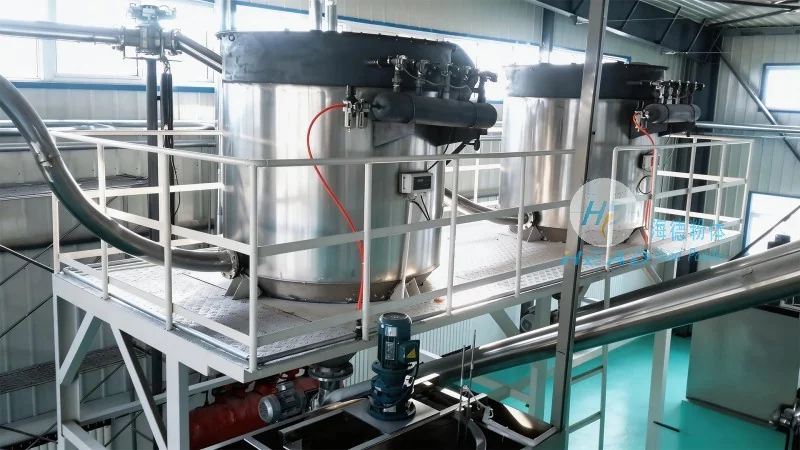
The operation process of the fully automatic bag opening material handling system involves several sequential steps, each meticulously designed to ensure optimal performance and minimal downtime. The process begins with the placement of sealed bags into the system's input hopper or conveyor. The system then uses a combination of mechanical and pneumatic components to open the bags, typically through cutting or tearing mechanisms that are tailored to the specific bag material and type. Once the bag is opened, the material is discharged into a hopper or a secondary conveyor. The system may include a level sensor or a weight sensor to monitor the material level, ensuring that the discharge process is controlled and prevents overfilling or underfilling. The material is then transported to the next stage of the production line via a conveyor system, which may include adjustable speed controls and directional changes to match the requirements of downstream equipment. The system also incorporates safety features such as emergency stop buttons, interlocks, and protective guards to prevent accidents and ensure compliance with safety regulations. Regular maintenance checks are performed to ensure all components are functioning correctly, including the bag opening mechanism, conveyor belts, and material sensors.
Working Principle of the System
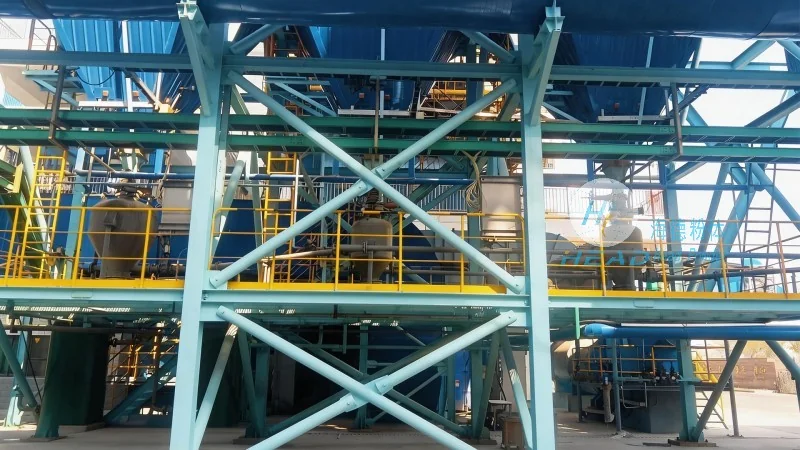
The working principle of the fully automatic bag opening material handling system is based on a combination of mechanical, pneumatic, and possibly electronic control systems. The core components include a bag opening unit, a material discharge hopper, a conveyor system, and a control panel with sensors and actuators. The bag opening unit is responsible for accessing the contents of the sealed bag. This unit may use a rotary cutter, a pneumatic knife, or a tearing mechanism, depending on the bag's material (e.g., plastic, paper, or composite). The system's control panel processes signals from various sensors, such as position sensors, pressure sensors, and level sensors, to coordinate the opening and discharge actions. The material discharge hopper collects the material from the opened bag and transfers it to the conveyor system. The conveyor system uses motor-driven belts or rollers to transport the material to the next processing stage. The speed and direction of the conveyor can be adjusted via the control panel to accommodate different material types and production rates. The control system, often a programmable logic controller (PLC), manages the entire operation by receiving input from sensors and sending commands to actuators. This ensures that each step of the process is executed in the correct sequence and at the appropriate time. The system may also include feedback loops to monitor performance and make adjustments in real-time, enhancing overall efficiency and reliability.
Technical Features and Advantages
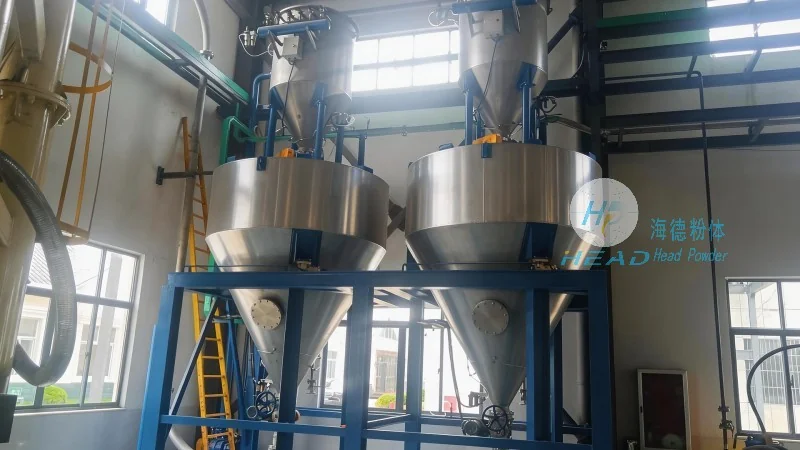
The fully automatic bag opening material handling system by Shandong HeadPowder Engineering Co., Ltd. offers several technical features that enhance its performance and usability. These features include: High Efficiency and Throughput: The system is designed to handle a high volume of bags per hour, with adjustable speeds to match production demands. This ensures that material handling operations are not a bottleneck in the production process. Versatility in Bag Types: The equipment can handle various bag sizes, materials, and types, including polyethylene, paper, and composite bags. This versatility makes it suitable for a wide range of industries, such as food processing, pharmaceuticals, and chemical manufacturing. Precise Material Control: The system uses sensors to monitor the material level and flow rate, ensuring accurate and consistent discharge. This reduces waste and improves product quality by preventing overfilling or underfilling. Safety and Reliability: The system incorporates multiple safety features, including emergency stop buttons, interlocks, and protective guards. Regular maintenance and diagnostic tools help to minimize downtime and ensure long-term reliability. Easy Integration and Customization: The system can be easily integrated with existing production lines and customized to meet specific customer requirements. This flexibility allows the equipment to adapt to different production environments and processes.
Application in Industrial Settings
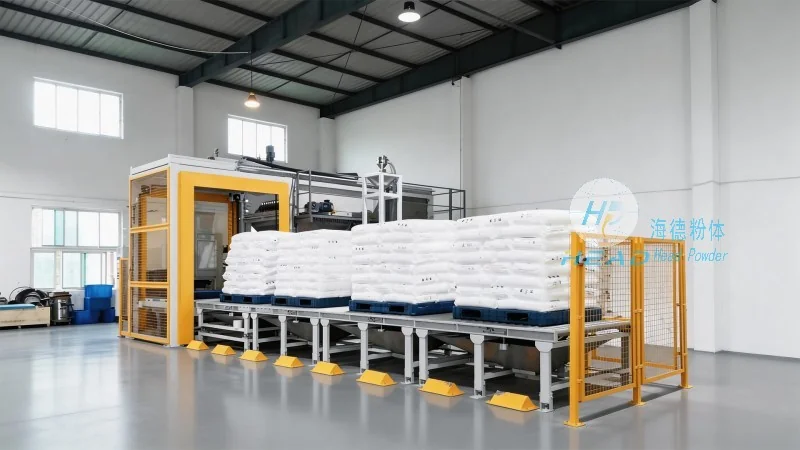
The fully automatic bag opening material handling system is widely used in various industrial settings where bulk materials need to be efficiently transferred from sealed bags. Some common applications include: Food and Beverage Industry: For handling raw materials such as flour, sugar, or coffee beans, where hygiene and precise control are critical. Pharmaceutical Industry: For processing active pharmaceutical ingredients (APIs) or other medicinal powders, where contamination and accuracy are paramount. Chemical Industry: For handling chemical powders and granules, where safety and material integrity are essential. Agricultural Industry: For processing agricultural products such as fertilizers or seeds, where large volumes and consistent quality are required. In each of these applications, the system contributes to increased productivity, reduced labor costs, and improved product quality by automating the material handling process.