

[WTTLE]Working Principle and Features of Automatic Powder Material Bag Opening and Pneumatic Conveyi
HeadPowder, a leading enterprise in the field of powder material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. Based in Shandong, China, the company has established itself as a trusted provider of efficient and reliable equipment for industries that require the safe and effective transportation of bulk powders. This article explores the working principle and key features of their automatic powder bag opening and pneumatic conveying systems, offering insights into how these technologies enhance operational efficiency and product integrity.
Working Principle of Automatic Powder Bag Opening and Pneumatic Conveying
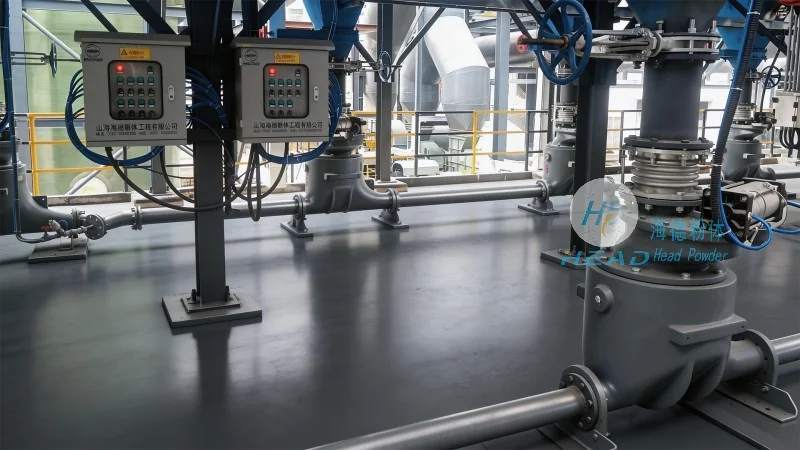
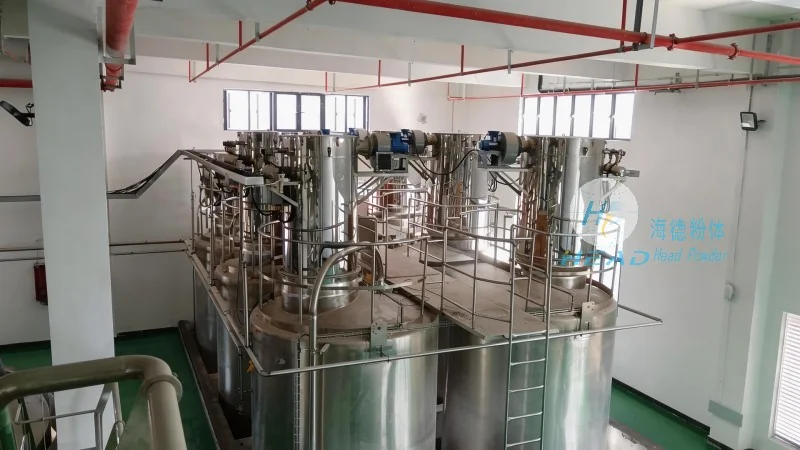
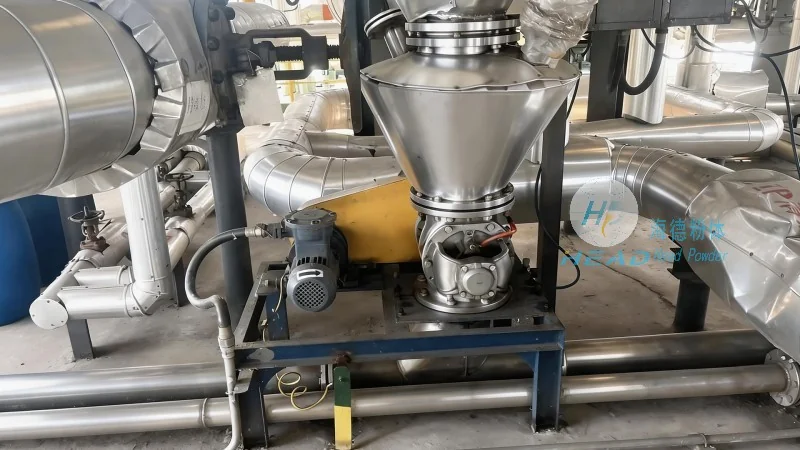
The automatic powder bag opening and pneumatic conveying system by HeadPowder operates through a series of integrated steps designed to streamline the handling of bulk powders from bag to process. The process begins with the automatic opening of sealed bags, which is typically achieved through mechanical or pneumatic means. Once the bag is opened, the powder is discharged into a hopper or collection bin. From there, the system uses a combination of air pressure and vacuum to transport the material through a network of pipes to the desired destination, such as a silo, storage tank, or processing equipment. The system may incorporate features like airlocks, rotary valves, and filters to ensure airtight operation and prevent dust contamination. The entire process is automated, reducing the need for manual intervention and minimizing the risk of product exposure to contaminants or environmental factors. The airlock system, for example, acts as a seal between the hopper and the conveying line, preventing backflow of air and ensuring that the powder is transferred smoothly and without loss. Rotary valves are used to control the flow of powder from the hopper to the conveying line, providing precise control over the material discharge rate. Filters are integrated to capture any fine particles or dust, maintaining the purity of the conveyed material and protecting the downstream equipment from wear and tear.
Key Features of the Automatic Powder Bag Opening and Pneumatic Conveying System
HeadPowder's automatic powder bag opening and pneumatic conveying system offers several distinct advantages that make it an ideal solution for industries dealing with sensitive or high-value powders. First, the system ensures airtight and dust-free operation, which is crucial for maintaining product quality and compliance with environmental regulations. The automated bag opening mechanism reduces labor costs and improves safety by eliminating the need for workers to handle heavy or potentially hazardous bags. Additionally, the pneumatic conveying technology provides gentle handling of the powder, minimizing product degradation and preserving its physical properties. The system is also highly customizable, allowing HeadPowder to tailor the design to the specific requirements of each client, including the type of powder, bag size, and conveying distance. Another key feature is the integration of monitoring and control systems, which enable real-time tracking of the conveying process and allow for quick adjustments to optimize performance. The robust construction of the equipment ensures long-term reliability and low maintenance costs, making it a cost-effective solution for long-term use. The system also incorporates energy-efficient components, such as variable frequency drives, which adjust the air pressure and flow rate based on the actual demand, reducing energy consumption and operational costs. Furthermore, the design allows for easy cleaning and maintenance, with removable parts that can be cleaned or replaced without disrupting the entire system. This feature is particularly important for industries that handle hygroscopic or sticky powders, as it prevents product buildup and ensures consistent performance over time.
Application and Benefits in Industrial Settings
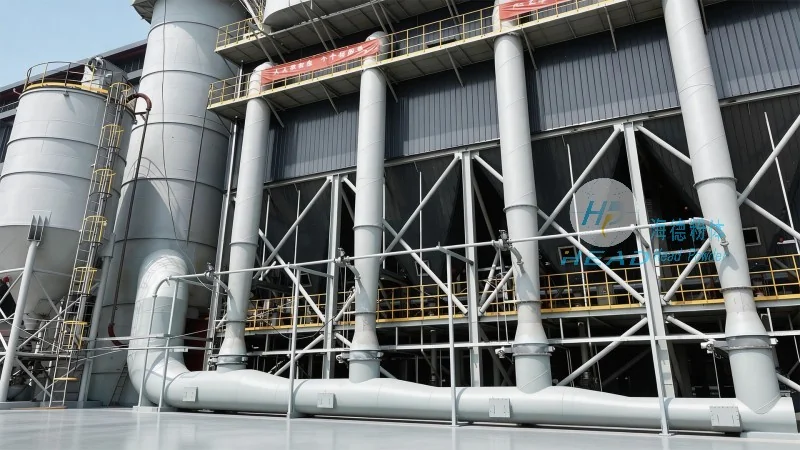
The automatic powder bag opening and pneumatic conveying system by HeadPowder is widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and cement production. In the pharmaceutical industry, for example, the system is used to transport active pharmaceutical ingredients (APIs) and excipients with high purity requirements, ensuring that the powders are handled in a sterile and controlled environment. The airtight operation and filtration system prevent contamination from airborne particles, maintaining the quality of the final product. In the food industry, the system is used to transport ingredients like flour, sugar, and spices, ensuring that the powders are handled hygienically and without cross-contamination. The gentle conveying process preserves the flavor and texture of the ingredients, which is critical for maintaining product quality. In the chemical industry, the system is used to transport powders like pigments, catalysts, and reagents, which may be hazardous or reactive. The automated operation reduces the risk of human exposure to these materials, while the airtight design prevents leaks and spills. The system's ability to handle a wide range of powder types and sizes makes it versatile and suitable for various industrial applications. The benefits of this system extend beyond operational efficiency, as it also contributes to improved workplace safety and environmental compliance. By reducing manual handling of heavy bags and minimizing dust emissions, the system helps to create a safer working environment and reduces the company's environmental footprint. The long-term reliability and low maintenance costs of the equipment also provide a significant return on investment, making it a cost-effective solution for businesses looking to enhance their material handling capabilities.