

Working Principle and Features of Polyvinyl Alcohol Formaldehyde Pneumatic Conveying System
For industries dealing with polyvinyl alcohol formaldehyde (PVOH-Formaldehyde) materials, efficient material handling is crucial. The Polyvinyl Alcohol Formaldehyde Pneumatic Conveying System offers a reliable solution for transporting these materials with precision and control. This system is designed to meet the specific needs of applications where handling such materials requires advanced technology and robust engineering. By understanding its working principle and key features, users can appreciate how this system enhances operational efficiency and safety in material processing.
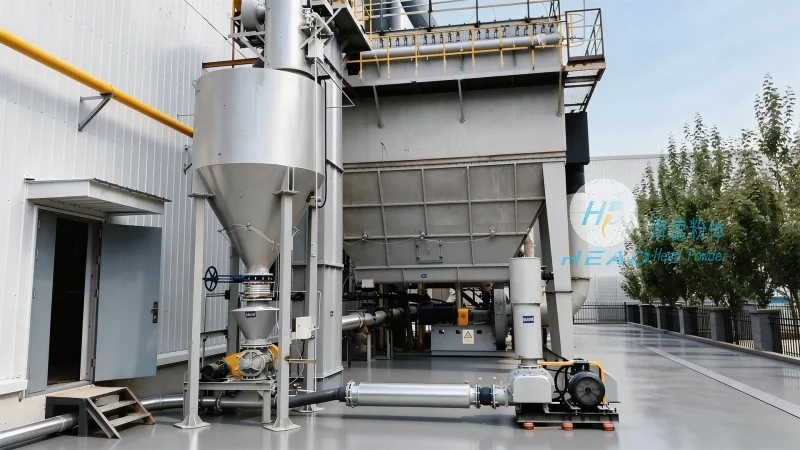
Working Principle of the PVOH-Formaldehyde Pneumatic Conveying System
The core of the Polyvinyl Alcohol Formaldehyde Pneumatic Conveying System lies in its pneumatic conveying mechanism, which utilizes air pressure to transport materials. The system operates by creating a pressure differential between the material source and the destination. A blower or compressor generates the necessary airflow, which draws the PVOH-Formaldehyde particles into the conveying line. The system typically includes components such as a hopper, a rotary valve, a conveying pipe, and a receiver. The hopper holds the material, and the rotary valve controls the flow of material into the conveying line. The conveying pipe transports the material using the air stream, while the receiver collects the material at the destination. The system can operate in both positive and negative pressure modes, depending on the application requirements. This flexibility allows for efficient handling of various PVOH-Formaldehyde products, ensuring consistent and reliable material transport.
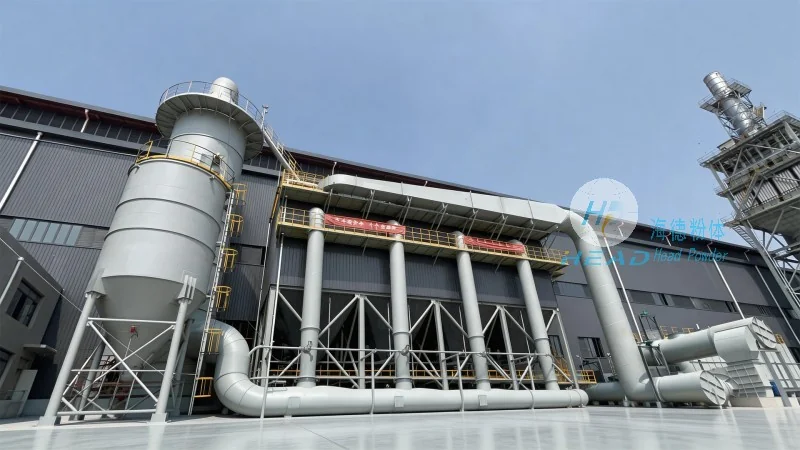
Key Features of the PVOH-Formaldehyde Pneumatic Conveying System
The Polyvinyl Alcohol Formaldehyde Pneumatic Conveying System is equipped with several features that enhance its performance and usability. One of the primary features is its ability to handle fine or powdery PVOH-Formaldehyde materials without clogging or blockages. The system uses a specially designed hopper and rotary valve to ensure smooth material flow, preventing material buildup that could lead to system failure. Another key feature is the adjustable airflow control, which allows operators to optimize the conveying speed and pressure based on the material characteristics and system requirements. This feature ensures that the material is transported at the optimal speed, reducing wear and tear on the system components and improving overall efficiency. Additionally, the system includes safety features such as pressure relief valves and overload protection, which safeguard the equipment and personnel from potential hazards. The system also offers easy maintenance and cleaning, with removable components that can be cleaned without disassembling the entire system. This reduces downtime and maintenance costs, making it a cost-effective solution for long-term use.
Applications and Benefits in Industrial Settings
The Polyvinyl Alcohol Formaldehyde Pneumatic Conveying System is widely used in various industrial applications where PVOH-Formaldehyde materials are processed. In the chemical industry, it is used for transporting raw materials and finished products in production lines. In the pharmaceutical industry, it is used for handling PVOH-Formaldehyde-based excipients and active ingredients, ensuring precise dosing and transport. The system also finds applications in the food and beverage industry, where it is used for transporting PVOH-Formaldehyde-based additives and ingredients. The benefits of using this system include improved material handling efficiency, reduced labor costs, and enhanced safety in the workplace. By automating the material transport process, the system minimizes human error and ensures consistent material quality. Additionally, the system reduces the risk of material contamination, which is critical in industries where product purity is paramount. The system's ability to handle different PVOH-Formaldehyde products with varying particle sizes and densities makes it a versatile solution for diverse industrial needs.
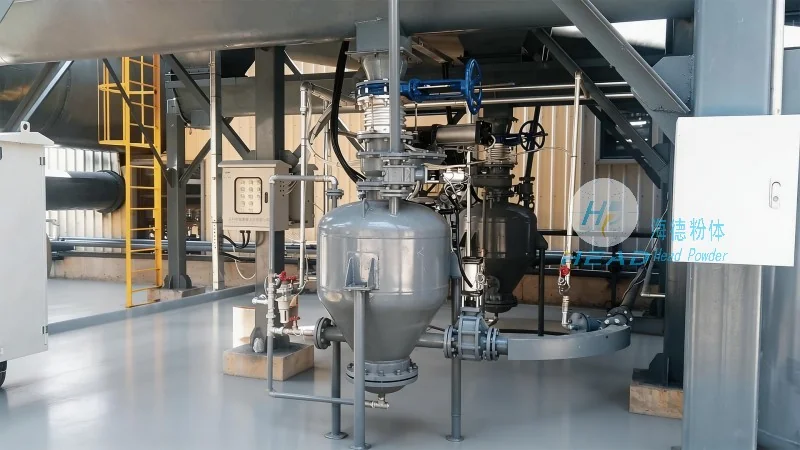
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of material handling equipment, specializes in providing high-quality solutions for industries dealing with various materials. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the material handling industry. The company's products, including the Polyvinyl Alcohol Formaldehyde Pneumatic Conveying System, are designed to meet the specific needs of its clients. HeadPowder's team of engineers and technicians work closely with clients to understand their requirements and develop customized solutions that enhance operational efficiency. The company's commitment to quality is reflected in its rigorous testing and quality control processes, ensuring that each product meets the highest standards. HeadPowder's products are widely used in various industries, including chemicals, pharmaceuticals, food, and manufacturing. The company's reputation for reliability and performance has made it a preferred choice for businesses seeking efficient and effective material handling solutions.