

Working Principle and Features of Denitrification Urea Material Handling Equipment
Denitrification urea material handling equipment is a critical component in modern industrial operations, particularly in power generation and chemical processing facilities where nitrogen oxide (NOx) reduction is mandated by environmental regulations. This equipment is specifically engineered to transport urea solution, a primary reducing agent used in selective catalytic reduction (SCR) systems for flue gas treatment. Understanding the working principle and distinctive features of such equipment is essential for optimizing operational efficiency, ensuring compliance with environmental standards, and maintaining the longevity of the system.
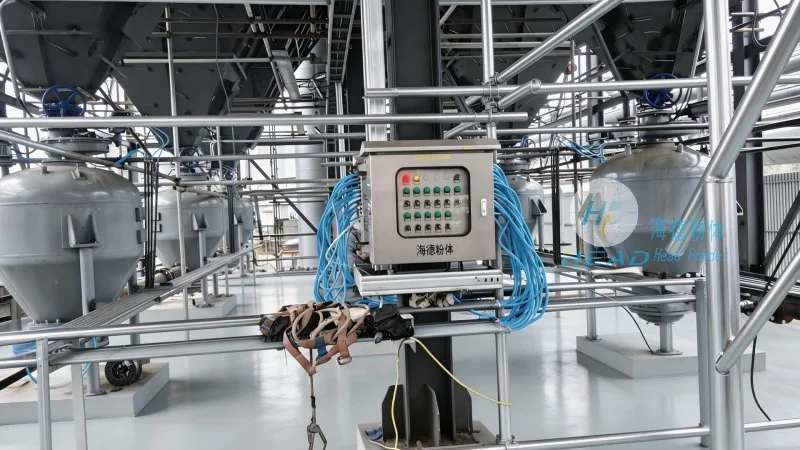
Working Principle of Denitrification Urea Material Handling Equipment
The working principle of denitrification urea material handling equipment revolves around the precise and controlled delivery of urea solution from storage to the injection point in the flue gas system. The process begins with the storage of urea solution in a dedicated tank, which is often equipped with temperature control mechanisms to maintain the solution at an optimal viscosity and flow rate. From the storage tank, the urea solution is pumped through a network of pipelines and valves to the dosing system. The dosing system typically utilizes advanced metering pumps or positive displacement pumps that regulate the flow rate and concentration of the urea solution based on real-time data from the flue gas system. This data includes parameters such as flue gas flow rate, NOx concentration, and temperature, enabling the system to calculate and deliver the exact amount of urea required for effective denitrification. The equipment incorporates a closed-loop control system that continuously monitors and adjusts the operation, ensuring consistent performance and minimizing waste. Additionally, safety features like pressure relief valves and leak detection sensors are integrated to prevent accidents and protect the environment.
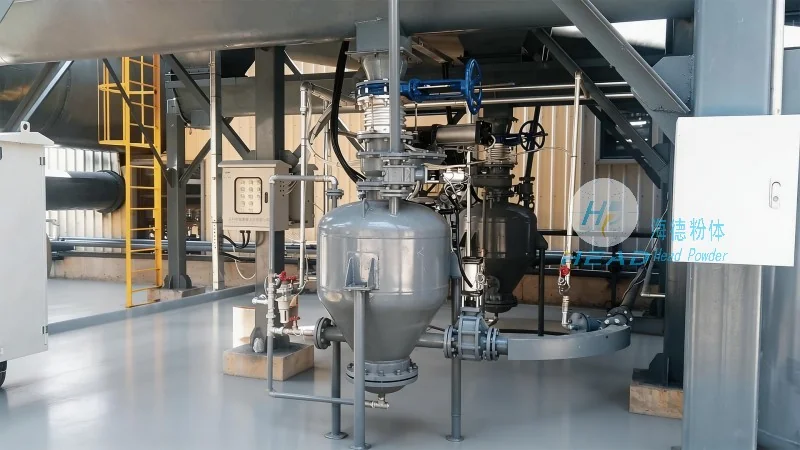
Key Features of Denitrification Urea Material Handling Equipment
Denitrification urea material handling equipment is distinguished by several key features that enhance its performance and reliability. One of the most significant features is its high precision in dosage control, which is crucial for achieving the desired NOx reduction while avoiding over-dosing that could lead to equipment corrosion or environmental contamination. The equipment is constructed with corrosion-resistant materials, such as stainless steel or specialized alloys, to withstand the chemical properties of urea and the harsh flue gas environment. This design ensures long-term durability and reduces maintenance requirements. Another notable feature is the integration of automated cleaning and maintenance functions, which help minimize downtime and maintain consistent operational performance. The modular design of the system allows for easy installation and integration into existing industrial facilities, providing flexibility for various plant configurations. Furthermore, advanced monitoring and control systems enable remote management, allowing operators to oversee the equipment from a central control room, enhancing efficiency and reducing the need for on-site personnel. The equipment also includes environmental protection measures, such as emergency shut-off valves and spill containment systems, to prevent accidental releases and mitigate environmental risks.
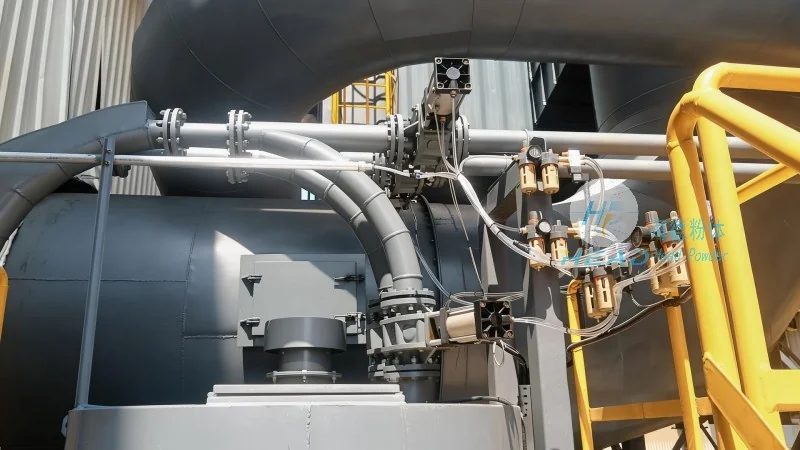
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading manufacturer and supplier of industrial material handling solutions, specializing in denitrification urea material handling systems. HeadPowder has established a strong reputation in the power and chemical industries by delivering high-quality, reliable equipment that meets stringent operational and environmental requirements. The company’s headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and a dedicated research and development team. HeadPowder’s engineers and technicians work closely with clients to understand their specific needs and provide tailored solutions that enhance efficiency and reduce costs. By adhering to international quality standards and implementing rigorous quality control processes, HeadPowder ensures that its products are durable, efficient, and compliant with industry regulations. The company’s commitment to innovation and customer satisfaction has made it a trusted partner for facilities worldwide, contributing to the sustainable advancement of industrial operations and environmental protection efforts.