

Principles and Application Scenarios of Intelligent Bag-Opening Pneumatic Conveying Machines
The intelligent bag-opening pneumatic conveying machine is a specialized equipment designed for efficient handling of bulk materials from sealed bags. It integrates advanced pneumatic conveying technology with intelligent bag-opening mechanisms, enabling seamless material transfer from packaging to processing or storage systems. This equipment is particularly valuable in industries where bulk materials are packaged in bags, such as chemicals, food, pharmaceuticals, and construction materials.
Principles of Operation
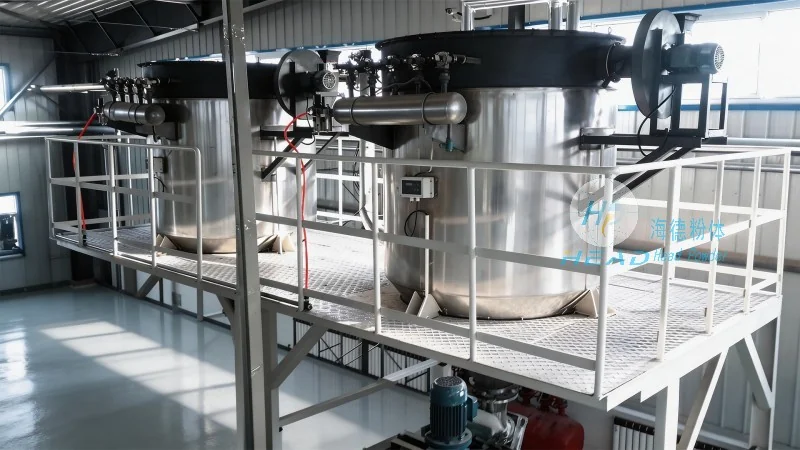
The core principle of pneumatic conveying involves using air to transport materials through a pipeline system. In the case of the intelligent bag-opening machine, the process begins with the machine identifying and opening the bag, then extracting the material inside. The bag is typically placed on a platform, and the machine uses a mechanical or pneumatic system to cut or tear the bag open. Once opened, the material is fed into a hopper or a pneumatic conveying line. The conveying system then uses compressed air to move the material through the pipeline to the destination. This method eliminates the need for manual bag opening and material handling, reducing labor costs and improving safety in the workplace.
Key Features and Advantages
Intelligent bag-opening pneumatic conveying machines offer several advantages over traditional methods. Firstly, they enhance operational efficiency by automating the material transfer process, which significantly reduces downtime and increases production throughput. Secondly, the equipment ensures material integrity and quality control, as it prevents contamination and maintains the purity of the bulk material. Additionally, the hygienic design of these machines is particularly important in food and pharmaceutical industries, where compliance with regulatory standards is essential. The machines are also equipped with sensors and control systems that allow for real-time monitoring and adjustment of the conveying process, ensuring optimal performance.
Application Scenarios and Industry Use Cases
The intelligent bag-opening pneumatic conveying machine is widely used in various industrial settings. In the chemical industry, it can handle powders and granules from bags, ensuring safe and efficient transfer to reactors or storage tanks. In the food and pharmaceutical sectors, the machine's hygienic design and ability to maintain material integrity are crucial, as it prevents contamination and preserves product quality. For construction material manufacturers, the equipment efficiently transfers cement, sand, and other bulk materials from bags to mixing plants or silos, improving production line throughput. Furthermore, in the agricultural sector, it can handle fertilizers and seeds from bags, facilitating their distribution to farms and processing facilities.
About HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing and producing advanced pneumatic conveying solutions. The company's intelligent bag-opening machines are engineered to meet the diverse needs of modern industrial applications, combining reliability, efficiency, and user-friendly operation. With a focus on innovation and quality, HeadPowder provides customized solutions tailored to specific material handling requirements. The company adheres to strict quality control standards and offers comprehensive after-sales support to ensure customer satisfaction and long-term partnership.