

Principle and Working Scene Characteristics of Fully Automatic Bulk Bag Unloading Material Pneumatic
For industries that handle bulk materials, efficient and reliable material handling is crucial for maintaining production efficiency and reducing operational costs. The fully automatic bulk bag unloading material pneumatic conveying system is a specialized solution designed to streamline the process of transferring bulk materials from bulk bags into processing equipment or storage systems. This system integrates advanced automation technologies and pneumatic conveying principles to achieve seamless, dust-free, and safe material transfer, making it an ideal choice for various industrial applications.
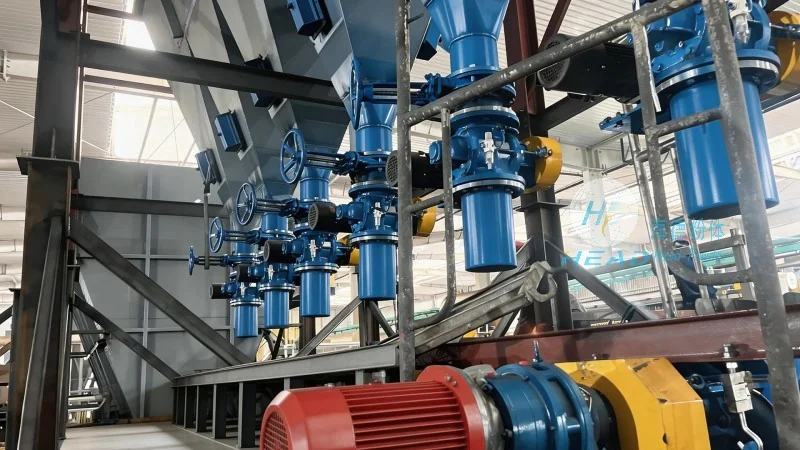
Overview of the Fully Automatic Bulk Bag Unloading Pneumatic Conveying System
The system is engineered to handle the entire process of bulk bag unloading, material transfer, and subsequent processing with minimal human intervention. It typically consists of several key components, including a bulk bag unloader, a pneumatic conveying pipeline, a material receiver, and an air filtration system. Each component works in coordination to ensure the smooth flow of materials from the bulk bag to the target destination. The system is designed to be compact, easy to install, and adaptable to different material types and processing requirements.
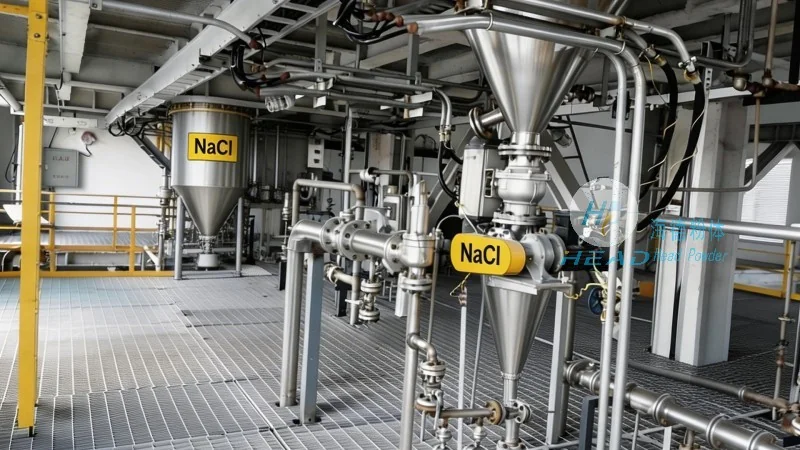
Working Principle of the System
The core principle of the pneumatic conveying system is the use of compressed air to create a flow that transports bulk materials through a pipeline. In the context of bulk bag unloading, the process begins with the opening of the bulk bag, followed by the controlled release of material into the conveying system. The system uses a combination of positive and negative pressure (or a combination of both) to move the material through the pipeline. The bulk bag unloader is equipped with a hopper and a valve mechanism that allows for the controlled discharge of material. As the material is discharged, compressed air is introduced into the hopper to create a vacuum or pressure differential that propels the material forward through the pipeline. The air filtration system ensures that any dust or particles are captured and filtered out, maintaining a clean and safe working environment.
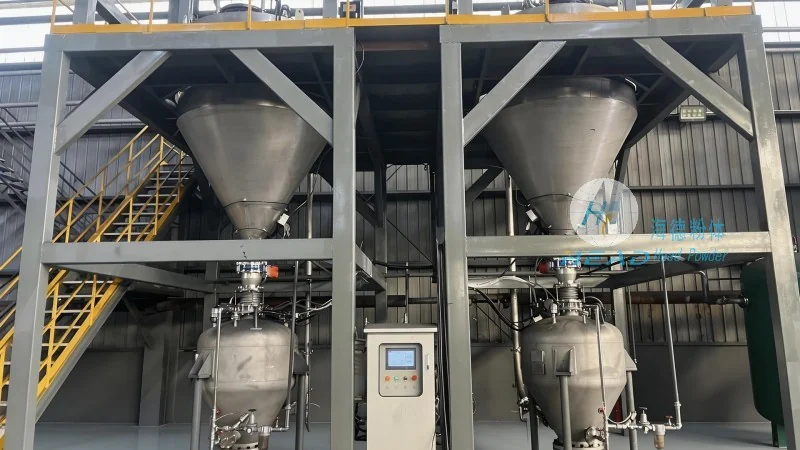
Key Working Scene Characteristics
The fully automatic bulk bag unloading material pneumatic conveying system is characterized by several distinct features that make it suitable for a wide range of industrial applications. Firstly, it offers high efficiency and speed, significantly reducing the time required for material transfer compared to manual methods. The system can handle large volumes of material with consistent performance, ensuring that production lines operate without interruptions. Secondly, it provides a dust-free and clean transfer process, which is particularly important for materials that are sensitive to contamination or for environments where dust control is mandatory. The system’s design minimizes the generation of dust and ensures that any particles are effectively captured and filtered. Thirdly, it enhances safety by reducing the need for manual handling of heavy or hazardous bulk bags. The automated process eliminates the risk of injury associated with lifting and moving heavy bags, and the enclosed system prevents exposure to dust and other airborne contaminants. Additionally, the system is highly adaptable, allowing for integration with existing production lines and equipment. It can be customized to accommodate different bag sizes, material types, and conveying distances, making it a versatile solution for various industrial settings.
Company Information
HeadPowder, a leading provider of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. With a focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for industries seeking efficient and reliable material transfer solutions. The company is headquartered in Shandong, China, and serves clients across various sectors, including chemicals, food, pharmaceuticals, and minerals. HeadPowder’s commitment to quality and technical excellence ensures that its systems meet the highest industry standards and deliver long-term performance and reliability.