

Operation Process and Working Principle of Soda Ash Powder Conveying System
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and installation of advanced conveying systems for soda ash powder. With a focus on efficiency, reliability, and safety, the company has established itself as a trusted partner for industries requiring precise and effective powder transportation solutions. This article provides an in-depth look at the operation process and working principle of their soda ash powder conveying system, highlighting the key components, operational steps, and technical aspects that contribute to its superior performance.
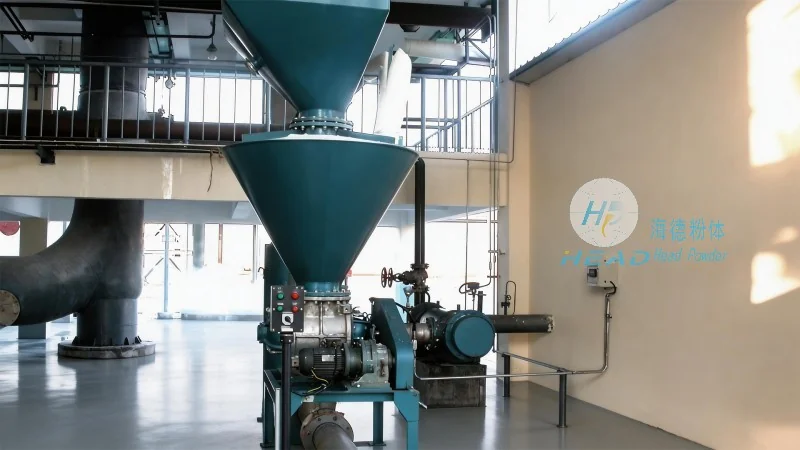
System Overview and Key Components
The soda ash powder conveying system developed by Shandong HeadPowder Engineering Co., Ltd. is a comprehensive solution tailored to meet the demanding requirements of modern industrial applications. The system typically consists of several critical components that work in harmony to ensure smooth and efficient powder transport. These components include a hopper for material storage, a feeder to control the flow rate, a conveyor (such as a screw or pneumatic conveyor) for actual transportation, and a control system to monitor and regulate the entire process. Each component is meticulously designed to handle the unique characteristics of soda ash powder, including its fine particle size, low bulk density, and potential for static charge accumulation.
Operation Process: Step-by-Step Guide
The operation of the soda ash powder conveying system follows a systematic sequence of steps to ensure consistent and reliable performance. The process begins with the loading of soda ash powder into the hopper. The hopper is equipped with a level indicator to monitor the material inventory, allowing operators to track the amount of powder available for transport. Once the hopper is filled to the desired level, the feeder activates to regulate the flow of powder into the conveyor. The feeder may use a variable speed motor or a weight-based mechanism to maintain a stable flow rate, preventing overloading or underloading of the conveyor. As the powder enters the conveyor, it is transported to the discharge point, which is typically connected to a storage silo or a processing unit. The control system continuously monitors parameters such as flow rate, pressure, and temperature to ensure that the system operates within safe and optimal conditions. Any deviations from the set parameters are immediately detected and corrected by the control system, minimizing downtime and maintaining the integrity of the powder.
Working Principle: How the System Transfers Powder Efficiently
The working principle of the soda ash powder conveying system is based on the principles of fluidization and mechanical transport. For the system utilizing a pneumatic conveyor, the powder is suspended in a stream of air or gas, creating a fluidized state that allows for smooth movement through the pipeline. The air pressure is carefully controlled to maintain the powder in a suspended state, preventing clogging and ensuring consistent flow. The screw conveyor, on the other hand, relies on the rotation of a helical screw to push the powder forward. The design of the screw, including its pitch and diameter, is optimized to handle the specific characteristics of soda ash powder, minimizing friction and wear while maximizing efficiency. The combination of these mechanisms—whether pneumatic or mechanical—ensures that the powder is transported with minimal degradation, preserving its quality and preventing segregation or agglomeration.
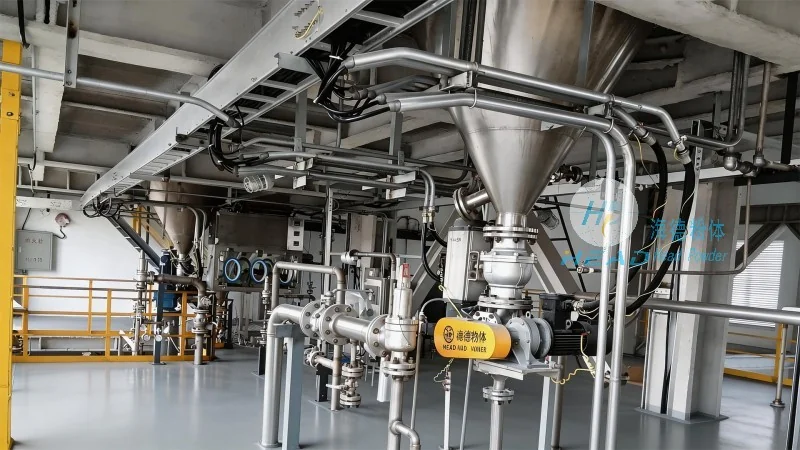
Advantages and Applications in Industrial Settings
The soda ash powder conveying system from Shandong HeadPowder Engineering Co., Ltd. offers several advantages that make it an ideal choice for various industrial applications. One of the key benefits is its ability to handle fine powders without causing blockages or system failures, which is crucial for maintaining production continuity. The system's design also minimizes the risk of dust generation and static charge buildup, enhancing workplace safety and compliance with environmental regulations. Additionally, the modular nature of the system allows for easy integration with existing production lines and scalability to accommodate increased production demands. Industries such as chemical manufacturing, food processing, and pharmaceuticals can benefit from this system, as it provides a reliable and efficient means of transporting soda ash powder to various processing stages, from storage to final product formulation.
Conclusion: Ensuring Optimal Performance and Reliability
In conclusion, the soda ash powder conveying system developed by Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated and reliable solution for the transportation of soda ash powder. By understanding the operation process and working principle of the system, users can appreciate how each component contributes to the overall efficiency and safety of the operation. The company's commitment to quality and innovation ensures that their systems are designed to meet the evolving needs of the industry, providing long-term value and performance. With its robust design and advanced control features, this system is a testament to the company's expertise in powder handling technology and its dedication to delivering superior solutions for its clients.