

Operation Process and Working Principle of Soil Powder Conveying System
Soil powder conveying systems are essential in various industrial applications, particularly in the construction, mining, and environmental sectors. These systems are designed to efficiently transport fine soil particles, powders, and other granular materials over long distances with minimal loss and optimal performance. Understanding the operation process and working principles of such systems is crucial for optimizing their use and ensuring reliable material handling.
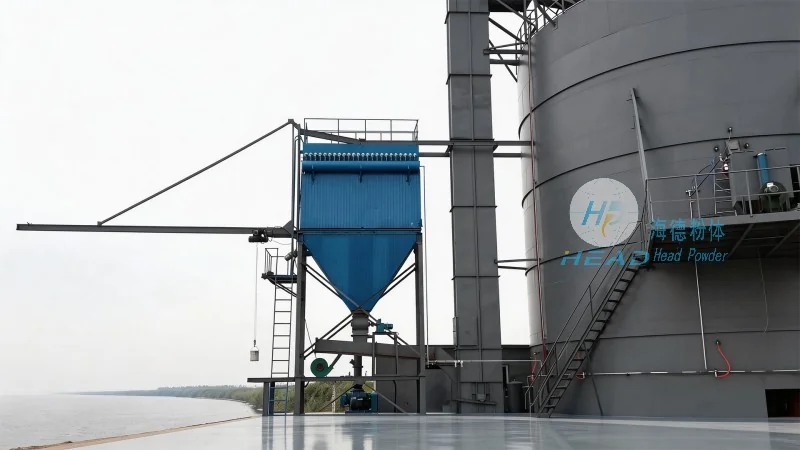
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of material handling equipment, specializes in the design, development, and production of advanced soil powder conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses requiring efficient and reliable solutions for transporting fine materials. HeadPowder's headquarters is located in Shandong, China, where the company leverages local expertise and resources to deliver cutting-edge technology tailored to global market needs.
Key Components of Soil Powder Conveying Systems
The operation of a soil powder conveying system involves several key components that work in tandem to ensure smooth material transport. These components typically include a feeding mechanism, a conveying device (such as a screw conveyor, pneumatic conveyor, or belt conveyor), a control system, and a discharge unit. Each component plays a vital role in the overall functionality of the system, contributing to the efficient movement of soil particles from the source to the destination.
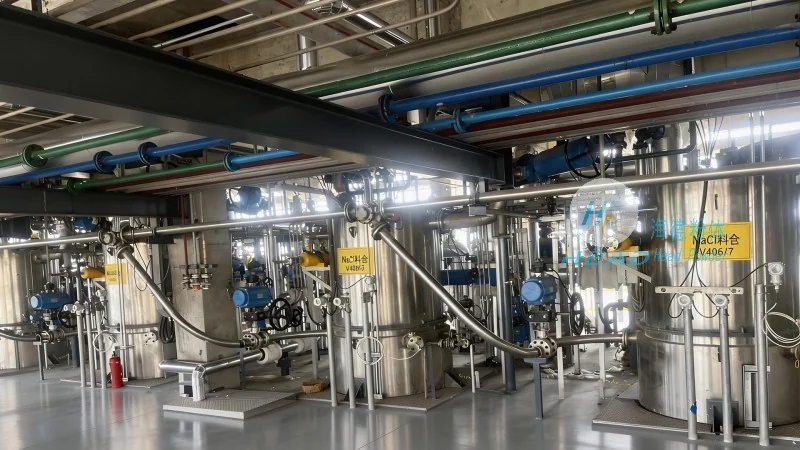
Working Principle of Soil Powder Conveying Systems
The working principle of a soil powder conveying system is based on the transfer of material through a closed or semi-closed pipeline. The system utilizes either mechanical force or pneumatic pressure to move the soil particles. In mechanical conveying systems, a rotating screw or auger pushes the material forward through the pipeline. In pneumatic conveying systems, air is used to create a pressure differential that propels the powder. The choice of system depends on factors such as the material characteristics, distance to be covered, and the required flow rate. The control system monitors and adjusts the conveying parameters to maintain optimal performance and prevent issues like blockages or material degradation.
Operation Process of Soil Powder Conveying Systems
The operation process of a soil powder conveying system begins with the feeding of soil material into the system. The material is then transported through the conveying pipeline, guided by the chosen mechanism. The system continuously monitors the flow rate and pressure to ensure consistent performance. At the discharge end, the material is collected and prepared for further processing or use. Regular maintenance and monitoring are essential to keep the system running efficiently and to extend its operational lifespan. HeadPowder's systems are engineered with durability and reliability in mind, ensuring that they can handle the demands of various industrial applications while minimizing downtime and maintenance costs.
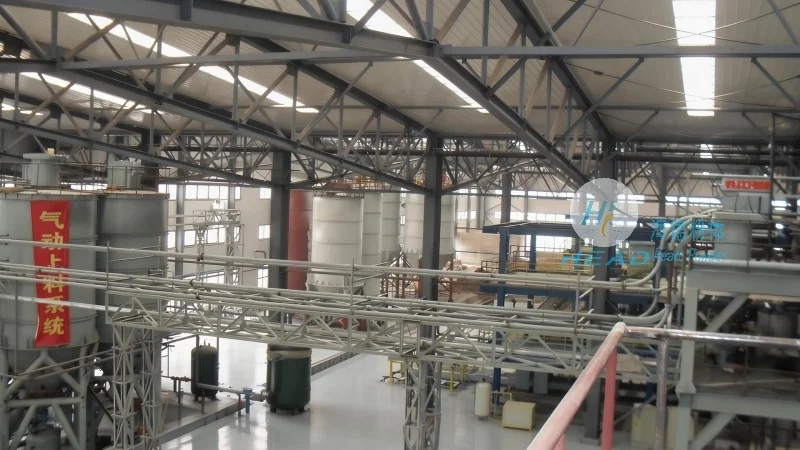
Applications and Benefits of Soil Powder Conveying Systems
Soil powder conveying systems are widely used in applications such as construction material transport, mining operations, and environmental remediation. These systems offer several benefits, including high efficiency, low energy consumption, and minimal material loss. By using advanced technology, HeadPowder's systems can handle a wide range of soil particle sizes and moisture content, making them versatile for different industrial needs. The systems also contribute to improved safety by reducing manual handling of powders and minimizing the risk of dust explosions. Overall, soil powder conveying systems provide a cost-effective and sustainable solution for material transport in various industries.
Conclusion
In conclusion, soil powder conveying systems are critical equipment for efficient material handling in industrial settings. The operation process and working principles of these systems, as exemplified by HeadPowder's advanced solutions, ensure reliable and efficient transport of soil particles. By understanding the key components and operation process, businesses can optimize their material handling operations and achieve better productivity and cost savings. HeadPowder continues to innovate and provide high-quality soil powder conveying systems that meet the evolving needs of the industry.