

Operation Process and Working Principle of Rice Husk Ash Powder Conveying System
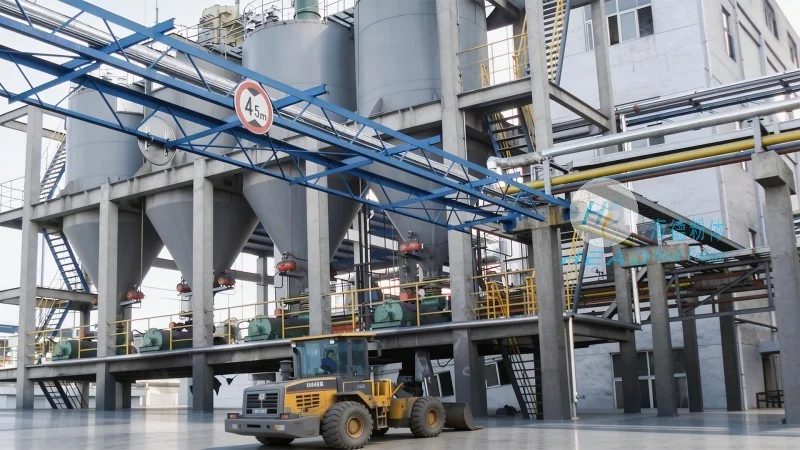
For industries dealing with rice husk ash, efficient and reliable powder conveying systems are crucial for maintaining production efficiency and ensuring product quality. The Rice Husk Ash Powder Conveying System developed by Shandong HeadPowder Engineering Co., Ltd. is a specialized solution designed to handle the unique challenges of transporting this specific material. This article will explore the operation process and working principle of this system, highlighting its key components, operational workflow, and the technical advantages it offers.
Company Overview
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer in the field of powder handling and conveying systems. With a strong focus on innovation and customer-centric solutions, the company has built a reputation for delivering high-quality equipment tailored to the needs of various industrial sectors. HeadPowder's expertise lies in designing systems that optimize material flow, minimize downtime, and enhance overall operational efficiency. The company's headquarters is located in Shandong, China, where its research and development teams continuously work on improving existing technologies and developing new solutions to meet evolving industry demands.
System Components and Design
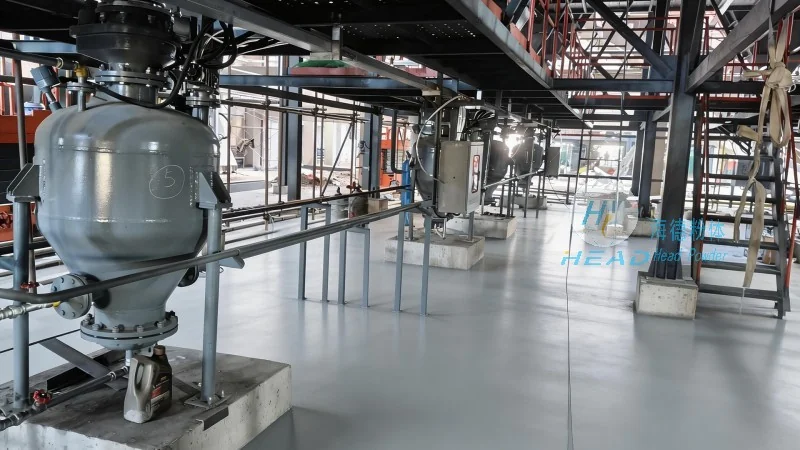
The Rice Husk Ash Powder Conveying System comprises several key components, each playing a vital role in the overall operation. The system typically includes a hopper for material storage, a feeder to control the flow rate, a conveyor mechanism (such as a screw conveyor or pneumatic system) for transporting the powder, and a control panel for monitoring and adjusting the process. The design of the system is tailored to handle the abrasive and lightweight nature of rice husk ash, ensuring durability and efficient performance. The hopper is equipped with a discharge valve to regulate the material release, while the feeder maintains a consistent feed rate to prevent blockages or overloading. The conveyor system is engineered to minimize material degradation and maintain the integrity of the powder, which is critical for downstream processing applications.
Working Principle
The working principle of the Rice Husk Ash Powder Conveying System is based on the principles of material flow and mechanical or pneumatic transport. The process begins with the storage of rice husk ash in the hopper. The feeder then regulates the flow of material into the conveyor. For mechanical conveying systems, a screw or belt conveyor moves the powder through the system, utilizing the force of gravity and mechanical drive to transport the material to the desired destination. In pneumatic conveying systems, compressed air is used to create a flow of air and material through a pipeline, allowing for more flexible and controlled transport. The control panel monitors key parameters such as pressure, flow rate, and temperature, providing real-time feedback to adjust the system's operation as needed. This closed-loop control ensures optimal performance and prevents issues like clogging or overpressure.
Operation Process
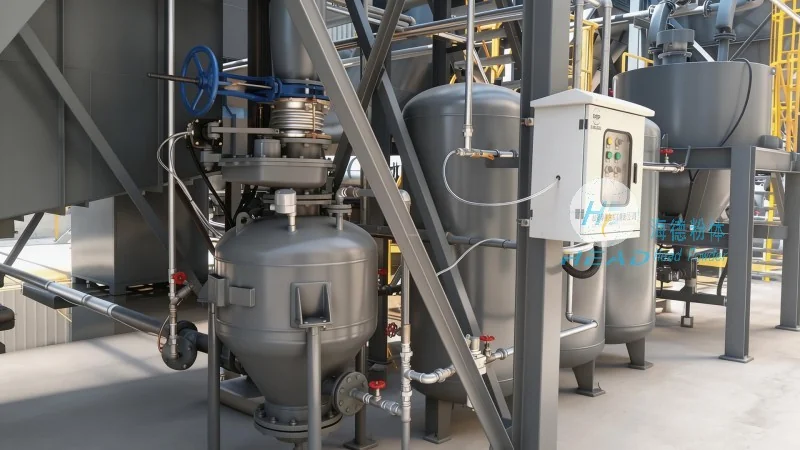
The operation process of the Rice Husk Ash Powder Conveying System is straightforward and designed for ease of use. The system starts by filling the hopper with rice husk ash. The operator then activates the feeder and conveyor, which begins the material transport. The control panel displays real-time data, allowing the operator to monitor the system's performance and make adjustments if necessary. The system is equipped with safety features, such as overload protection and emergency stop buttons, to ensure safe operation. Once the material reaches the destination, the conveyor slows down or stops, and the discharge valve opens to release the powder into the receiving container. The process can be automated, with the system running continuously based on preset parameters, reducing the need for manual intervention and minimizing labor costs.
Technical Advantages and Applications
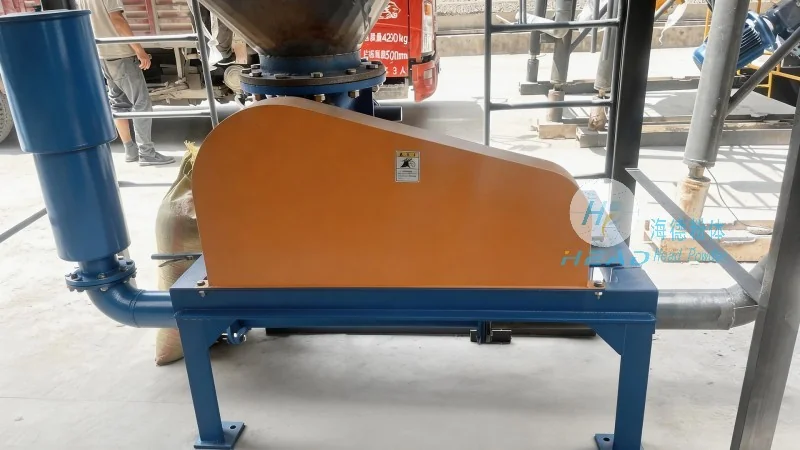
The Rice Husk Ash Powder Conveying System offers several technical advantages that make it an ideal choice for industries processing rice husk ash. The system's design minimizes material degradation, preserving the quality of the ash for downstream applications such as fuel or fertilizer production. The efficient conveying process reduces downtime and increases production throughput, leading to higher operational efficiency. The system's compact design and modular components allow for easy installation and maintenance, reducing the overall cost of ownership. Additionally, the system's control panel provides comprehensive monitoring and data logging capabilities, enabling operators to analyze performance and identify areas for improvement. The system is widely used in power plants, agricultural processing facilities, and other industries that rely on rice husk ash as a raw material.
Conclusion
In conclusion, the Rice Husk Ash Powder Conveying System developed by Shandong HeadPowder Engineering Co., Ltd. is a reliable and efficient solution for transporting rice husk ash. By understanding the operation process and working principle of this system, industries can optimize their material handling processes, improve productivity, and reduce operational costs. The system's robust design, advanced control features, and customization options make it a versatile choice for various applications, ensuring that it meets the specific needs of different industrial sectors. With its focus on innovation and customer satisfaction, HeadPowder continues to be a leader in providing high-quality powder conveying systems that enhance operational efficiency and support sustainable industrial practices.