

Operation Process and Working Principle of Cotton Seed Powder Conveying Equipment
For the efficient handling and transportation of cotton seed powder, specialized conveying equipment is essential. This article provides a detailed overview of the operation process and working principles of cotton seed powder conveying equipment, highlighting key components and operational steps that ensure smooth and reliable material transport. The information is presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China.
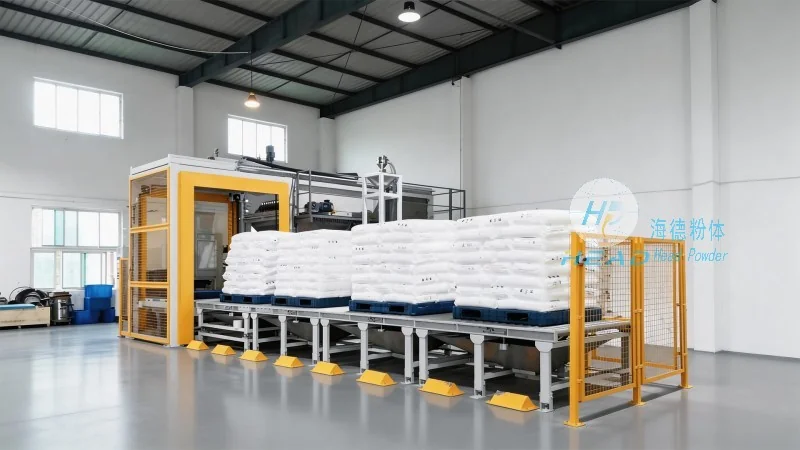
Overview of Cotton Seed Powder Conveying Equipment
Cotton seed powder conveying equipment is designed to handle the unique characteristics of cotton seed powder, such as its fine particle size, potential for static electricity, and varying moisture content. These factors require specialized equipment to prevent material buildup, ensure consistent flow, and maintain product integrity. The system typically includes components like hoppers, feeders, conveyor lines, and control systems, all working in tandem to achieve efficient material transfer.
Key Components and Their Functions
The operation of cotton seed powder conveying equipment relies on several critical components, each playing a specific role in the overall process. The primary components include:
- Feed Hopper: A storage container that holds the cotton seed powder, providing a consistent feed to the conveyor system. The hopper is designed with a sloped bottom to facilitate material flow and may include a level sensor to monitor inventory.
- Rotary Valve (Airlock): A device that regulates the flow of material from the hopper to the conveyor line. It acts as a seal to prevent dust emissions and ensures a controlled discharge of powder, preventing surges or blockages.
- Pneumatic Conveying System: This system uses compressed air to transport the cotton seed powder through a network of pipes. The air velocity and pressure are carefully controlled to maintain a consistent flow rate and prevent material degradation.
- Control Panel: An integrated system that monitors and controls the operation of all components. It includes sensors for flow rate, pressure, and temperature, as well as alarms and safety features to ensure the equipment operates within safe parameters.
Operation Process of Cotton Seed Powder Conveying Equipment
The operation process of cotton seed powder conveying equipment involves several sequential steps, each designed to ensure efficient and safe material transport. The process typically begins with the loading of cotton seed powder into the feed hopper. The powder is then discharged from the hopper into the rotary valve, which regulates the flow to the pneumatic conveying line. Compressed air is introduced into the line, creating a flow that carries the powder to the destination point, such as a storage silo or processing unit.
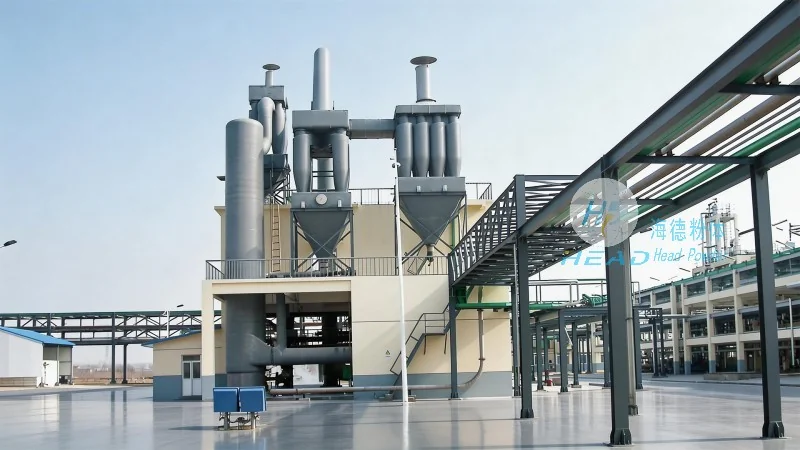
During operation, the control panel continuously monitors key parameters, such as air pressure, flow rate, and material level. If any parameter deviates from the set points, the system automatically adjusts or triggers an alarm to alert operators. This real-time monitoring ensures that the conveying process remains stable and efficient, minimizing downtime and material loss.
Working Principle of Cotton Seed Powder Conveying Equipment
The working principle of cotton seed powder conveying equipment is based on the principles of fluidization and pneumatic transport. The pneumatic conveying system uses compressed air to create a flow that suspends the cotton seed powder particles in the air stream. This suspension allows the powder to be transported through the pipeline without the need for mechanical contact, reducing wear and tear on the equipment and preventing material degradation.
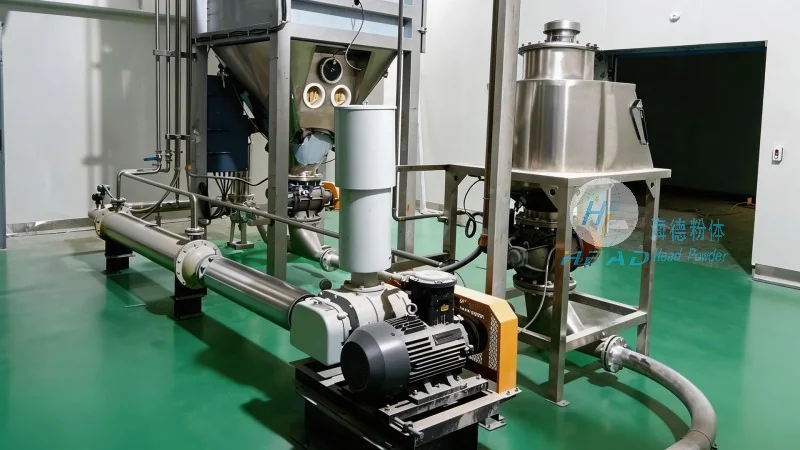
The rotary valve acts as a critical component in maintaining the flow rate and preventing dust emissions. By controlling the opening and closing of the valve, the system ensures a consistent discharge of powder from the hopper to the conveyor line. The airlock design also prevents backflow of air and material, maintaining a sealed system that minimizes environmental contamination.
Benefits of Using Cotton Seed Powder Conveying Equipment
Implementing cotton seed powder conveying equipment offers several benefits for industrial operations. These include improved efficiency in material handling, reduced labor costs, and enhanced product quality. The equipment also minimizes dust generation and improves workplace safety by containing the material within a sealed system. Additionally, the controlled flow and consistent delivery of cotton seed powder ensure that downstream processes, such as processing or packaging, operate smoothly and without interruptions.
Conclusion
Cotton seed powder conveying equipment is a vital component in the processing and handling of cotton seed products. By understanding the operation process and working principles of this equipment, operators can optimize its performance and ensure reliable material transport. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality conveying systems tailored to the unique needs of cotton seed powder, providing solutions that enhance efficiency and product integrity.