

Types and Practical Applications of Pneumatic Conveying Systems for Carbon Black and Coal Powder Han
Pneumatic conveying systems are essential for the efficient and safe transportation of fine powders such as carbon black and coal powder. These systems utilize air or gas to move materials through a pipeline, offering advantages like reduced dust, improved safety, and enhanced process control. For industries dealing with carbon black and coal powder, selecting the right type of pneumatic conveying system is crucial to optimize performance and operational efficiency. This article explores the different types of pneumatic conveying systems used in carbon black and coal powder handling, along with their practical applications, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. (headpowder) in providing tailored solutions for such applications.
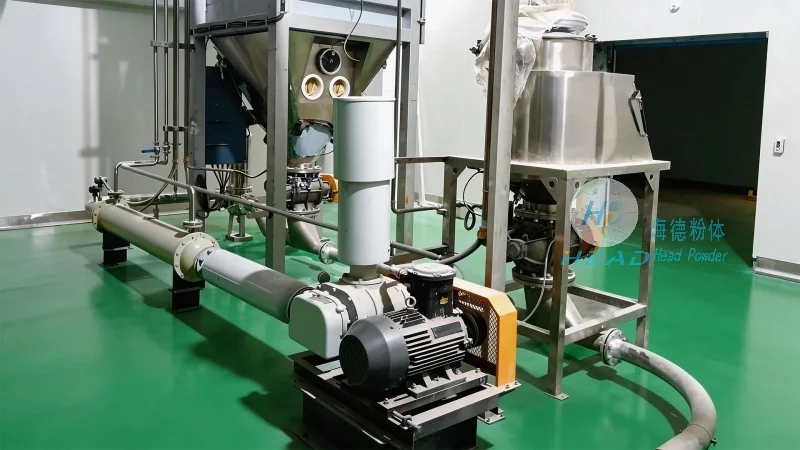
Types of Pneumatic Conveying Systems
There are several types of pneumatic conveying systems, each designed to suit different material characteristics, flow rates, and operational requirements. The primary types include:
1. Dilute Phase Pneumatic Conveying - This system operates at low pressure and high velocity, where the powder is suspended in the air stream. It is suitable for long-distance transport and is commonly used for carbon black and coal powder due to its ability to handle fine particles efficiently. The system uses a positive pressure or negative pressure (vacuum) to move the material, ensuring minimal pressure drop and consistent flow.
2. Dense Phase Pneumatic Conveying - Also known as low velocity conveying, this system operates at higher pressure and lower velocity, where the powder is conveyed in a dense phase. It is ideal for transporting sensitive materials or those that are prone to degradation, as the lower velocity reduces particle impact and friction. This type is particularly useful for carbon black and coal powder that require gentle handling to maintain quality.
3. Hybrid Pneumatic Conveying - This system combines elements of both dilute and dense phase conveying, offering flexibility in handling various materials and flow rates. It can switch between low and high velocity modes based on the material being transported, making it suitable for complex applications where different materials or conditions are encountered. For carbon black and coal powder handling, hybrid systems provide a versatile solution that can adapt to changing operational needs.
Practical Applications in Carbon Black and Coal Powder Handling
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing pneumatic conveying systems tailored to the specific needs of carbon black and coal powder industries. The practical applications of these systems vary across different sectors, including:
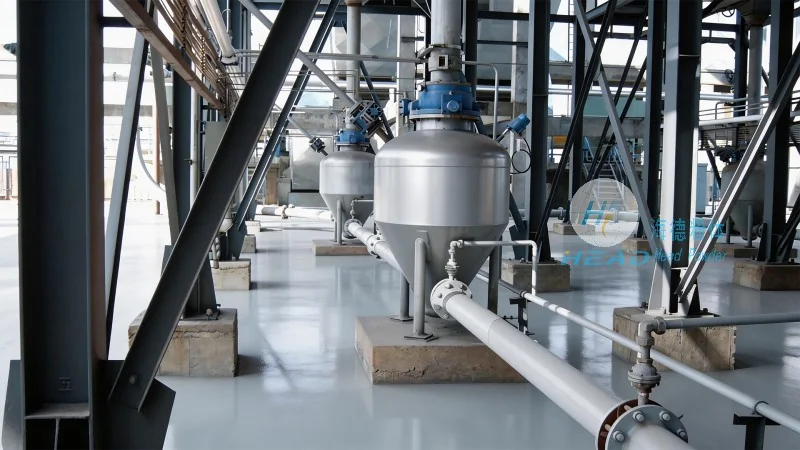
1. Manufacturing Plants - In carbon black production facilities, pneumatic conveying systems are used to transport raw materials, intermediate products, and finished goods between processing units. For example, in the production of carbon black, raw petroleum or coal is converted into the powder, and the system efficiently moves the material from the reactor to storage or further processing stages. This ensures a continuous and smooth production flow, minimizing downtime and material loss.
2. Coal Processing Facilities - In coal processing plants, pneumatic conveying systems are employed to transport coal from storage areas to processing equipment, such as crushers, screens, and conveyors. The systems help in maintaining a consistent supply of coal, reducing the risk of dust accumulation and improving safety in the plant. For coal powder, the dense phase conveying is often preferred to prevent particle degradation and ensure the quality of the final product.
3. Industrial Applications - Beyond manufacturing, pneumatic conveying systems are used in various industrial applications involving carbon black and coal powder. For instance, in the production of rubber and plastics, carbon black is added as a pigment or reinforcing agent, and the system efficiently delivers the powder to the mixing and extrusion processes. Similarly, in coal-fired power plants, coal powder is transported to the boilers for combustion, where the system ensures a steady and controlled supply of fuel.
Benefits of Using Pneumatic Conveying Systems
Implementing pneumatic conveying systems for carbon black and coal powder handling offers several key benefits that enhance operational efficiency and product quality:
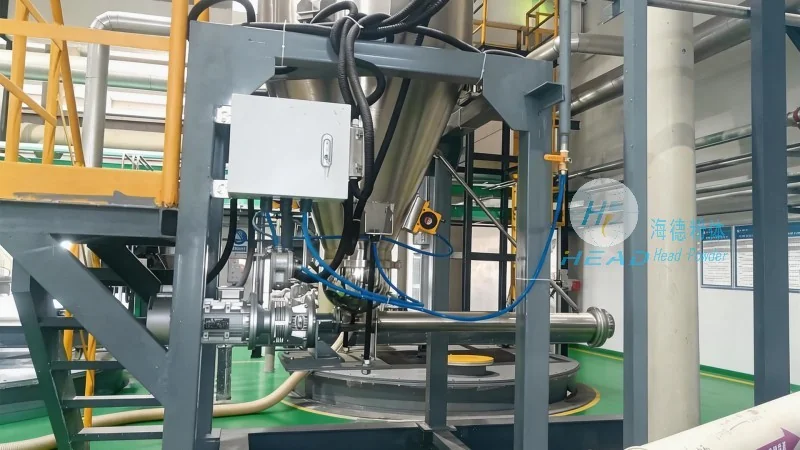
1. Improved Safety and Environmental Control - Unlike traditional belt or bucket elevators, pneumatic conveying systems minimize dust generation and exposure, reducing the risk of respiratory issues and environmental contamination. The enclosed system also helps in controlling dust emissions, making it compliant with environmental regulations. This is particularly important for carbon black and coal powder, which are known to be hazardous if not handled properly.
2. Enhanced Process Control and Flexibility - Pneumatic conveying systems allow for precise control over the flow rate, pressure, and temperature of the material being transported. This flexibility enables manufacturers to adjust the system according to changing production demands, such as varying the amount of carbon black added to a product or the flow rate of coal powder to a boiler. The ability to integrate with other process control systems further enhances operational efficiency.
3. Reduced Maintenance and Downtime - With fewer moving parts compared to traditional conveying equipment, pneumatic systems require less maintenance and have lower downtime. The use of high-quality materials and components ensures durability and longevity, reducing the overall operational costs for carbon black and coal powder handling facilities. Shandong HeadPowder Engineering Co., Ltd. provides robust and reliable systems that minimize maintenance needs and ensure consistent performance.
Customized Solutions by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. (headpowder) is a leading provider of pneumatic conveying systems tailored to the specific requirements of carbon black and coal powder industries. With years of experience and expertise in material handling, the company offers customized solutions that address the unique challenges faced by manufacturers. The company’s team of engineers works closely with clients to understand their operational needs, material characteristics, and production goals, ensuring that the designed system meets all requirements and delivers optimal performance.
For carbon black and coal powder handling, headpowder provides a range of services, including system design, installation, and maintenance. The company uses advanced technology and high-quality components to ensure that the systems are efficient, reliable, and cost-effective. By leveraging the expertise of headpowder, manufacturers can enhance their production processes, improve product quality, and reduce operational costs. The company’s commitment to quality and customer satisfaction has made it a trusted partner in the industry, serving clients across China and beyond.