

Types, Features, and Applications of Dry Coffee Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored for the coffee industry. With a focus on efficient and reliable solutions, the company has established itself as a key player in providing advanced dry coffee handling technologies.
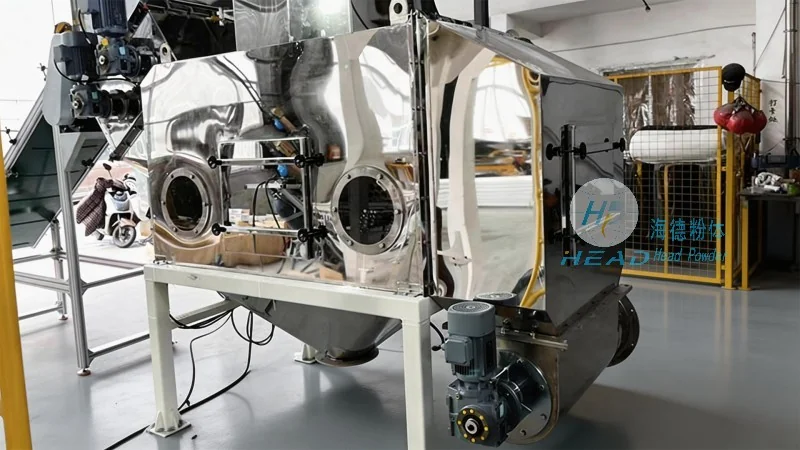
Types of Dry Coffee Pneumatic Conveying Systems
Dry coffee pneumatic conveying systems are categorized based on the principle of air flow and material transport mechanisms. The primary types include positive pressure systems, negative pressure systems, and hybrid systems. Each type offers distinct advantages depending on the specific requirements of coffee processing facilities.
Positive pressure systems utilize compressed air to push coffee particles through the conveying line, ensuring consistent flow and minimal product degradation. This method is particularly effective for long-distance or high-temperature applications where maintaining product quality is critical. Negative pressure systems, on the other hand, use vacuum to draw coffee from the source, making them suitable for short-distance or low-volume operations. Hybrid systems combine elements of both positive and negative pressure, offering flexibility in handling various coffee types and processing conditions.
Key Features of Dry Coffee Pneumatic Conveying Systems
Efficiency and reliability are paramount in coffee processing, and dry coffee pneumatic conveying systems are engineered to meet these demands. The systems are designed with high-capacity air pumps and durable materials to withstand the abrasive nature of coffee beans and grounds. Advanced filtration and separation technologies are integrated to prevent product contamination and ensure clean air circulation. Additionally, these systems feature automated controls and monitoring capabilities, allowing for real-time adjustments and maintenance alerts to minimize downtime.
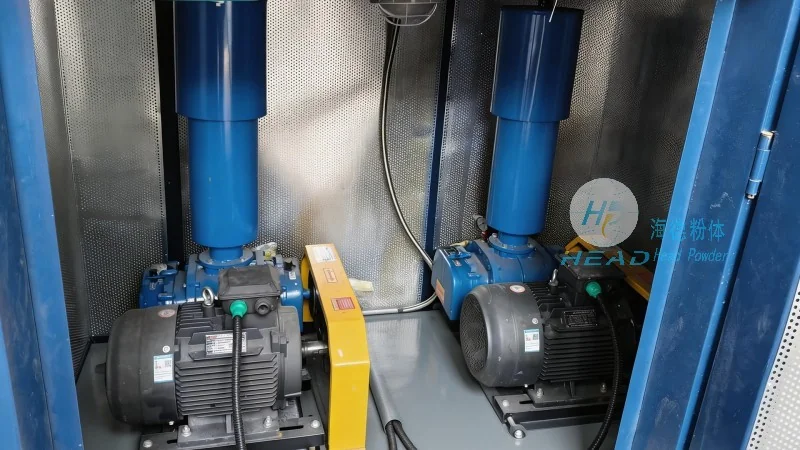
Another notable feature is the ability to handle a wide range of coffee products, from raw green coffee beans to ground coffee powders. The flexibility in material handling ensures that different stages of coffee processing can be efficiently managed with a single or modular system. Energy efficiency is also a key consideration, with modern systems incorporating variable frequency drives and optimized air flow to reduce operational costs while maintaining performance.
Application Ranges of Dry Coffee Pneumatic Conveying Systems
Dry coffee pneumatic conveying systems find extensive applications across various stages of coffee production and processing. In the raw material handling phase, these systems efficiently transport green coffee beans from storage silos to roasting equipment, ensuring a continuous and smooth workflow. During the roasting process, the systems can handle roasted coffee beans, transferring them to cooling and packaging areas without manual intervention.
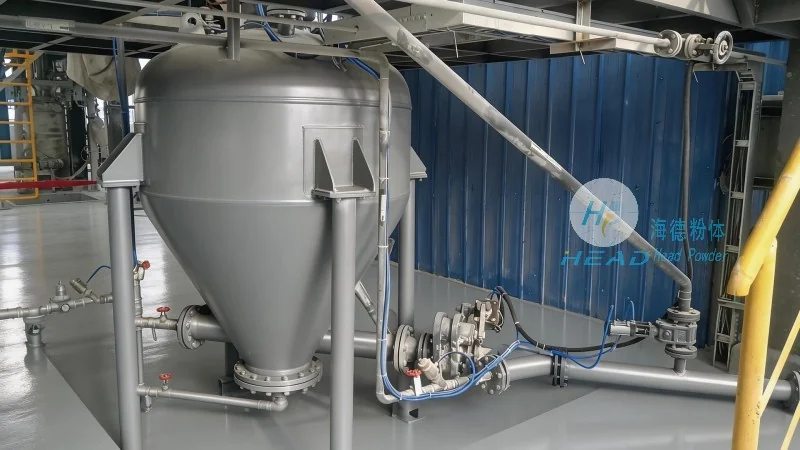
Post-roasting, the systems are used to convey ground coffee from grinding machines to packaging lines, maintaining product integrity and preventing cross-contamination. For specialty coffee operations, such as those involving flavored or blended coffee products, the systems can handle additional ingredients like spices, sweeteners, or flavorings, integrating seamlessly into complex production lines. Additionally, these systems are suitable for small-scale coffee roasters and large industrial coffee processing plants, adapting to different production volumes and facility sizes.
Company Expertise and Services
Shandong HeadPowder Engineering Co., Ltd. leverages years of industry experience to deliver customized pneumatic conveying solutions for the coffee industry. The company’s team of engineers and technicians work closely with clients to understand their specific needs, from initial system design and material selection to on-site installation and commissioning. With a commitment to quality and customer satisfaction, headpowder provides comprehensive after-sales support, including maintenance services, spare parts supply, and technical training to ensure long-term system performance.
HeadPowder’s facilities are equipped with advanced manufacturing equipment and testing labs, enabling the production of high-quality components and thorough system performance validation. The company adheres to international standards and certifications, ensuring that all products meet the rigorous requirements of the coffee industry. By combining technical expertise with customer-centric service, headpowder helps coffee processing facilities enhance operational efficiency, reduce costs, and maintain product quality throughout the entire production process.