

What is a Coffee Powder Material Pneumatic Conveying System? What Are Its Design Principles?
Understanding Coffee Powder Material Pneumatic Conveying Systems
Coffee powder material pneumatic conveying systems are specialized industrial equipment designed to transport coffee powder and other fine particulate materials efficiently and reliably. These systems utilize air or gas as the conveying medium to move the material from one location to another, eliminating the need for mechanical components like belts or screws that might cause contamination or degradation of the product.
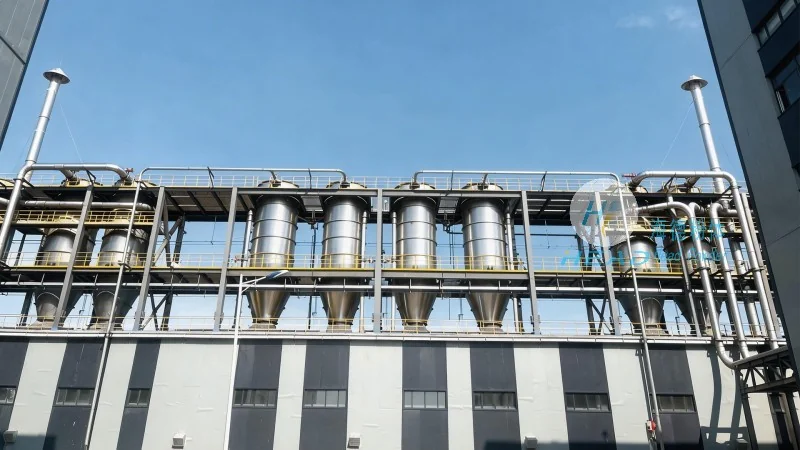
Design Principles of Coffee Powder Pneumatic Conveying Systems
The design of coffee powder pneumatic conveying systems is based on several key principles to ensure optimal performance. First, the system must maintain a consistent air flow rate to ensure the material is fully entrained and transported without clogging. Second, the system incorporates proper filtration and separation mechanisms to prevent dust accumulation and maintain product purity. Third, the design considers the specific properties of coffee powder, such as its density, moisture content, and flow characteristics, to optimize the conveying velocity and pressure.
Key Components and Their Roles
A typical coffee powder pneumatic conveying system includes several critical components. The air compressor or blower provides the necessary pressure and airflow to move the material. The hopper or storage bin holds the coffee powder, with a feeder mechanism that controls the material discharge rate. The conveying line, often made of stainless steel or other corrosion-resistant materials, transports the material from the source to the destination. The receiver or discharge hopper collects the material at the end of the line. Additionally, the system may include filters, cyclones, and pressure vessels to manage air and material separation.
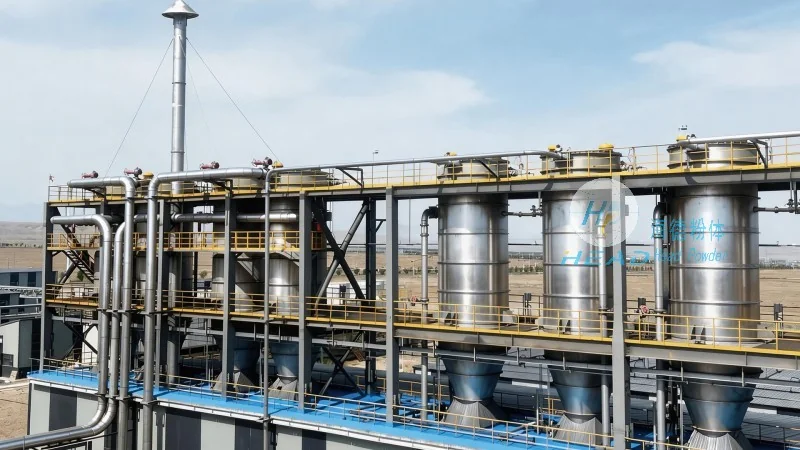
Advantages of Using Pneumatic Conveying for Coffee Powder
Pneumatic conveying offers several advantages for coffee powder handling. It provides a clean and hygienic method of transport, which is crucial for maintaining the quality and safety of coffee products. The system can handle fine powders without causing particle breakdown or agglomeration, preserving the product's texture and flavor. Additionally, pneumatic conveying systems are flexible, allowing for changes in material flow rates and destinations without major modifications. They also reduce labor costs by automating the material transport process and minimizing the need for manual handling.
HeadPowder's Expertise in Coffee Powder Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced coffee powder pneumatic conveying systems tailored to the unique needs of the coffee industry. With years of experience in material handling technology, HeadPowder understands the importance of maintaining product integrity and operational efficiency. The company's engineers work closely with clients to analyze their specific requirements, such as production volume, material properties, and facility layout, to develop customized solutions that meet or exceed industry standards.
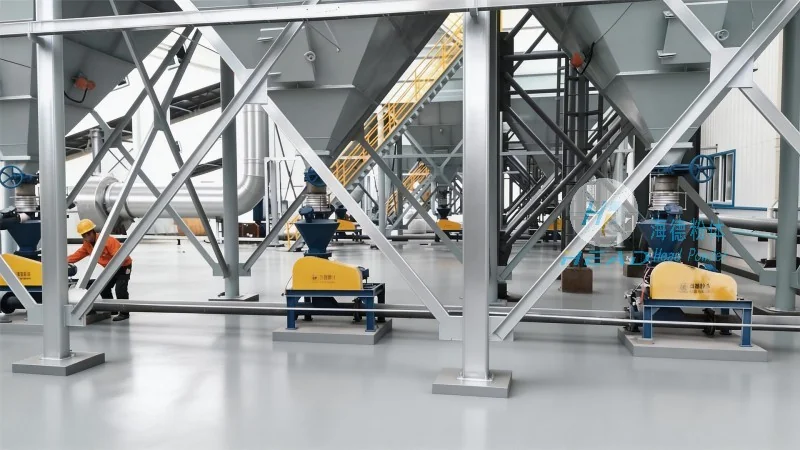
Customization and Innovation in Coffee Powder Conveying Solutions
HeadPowder offers a range of customization options for coffee powder pneumatic conveying systems. This includes selecting appropriate air velocities, pressure levels, and equipment materials based on the coffee powder's characteristics. The company also integrates advanced control systems that monitor and adjust the conveying process in real-time, ensuring consistent performance and minimizing downtime. By leveraging cutting-edge technology and industry best practices, HeadPowder delivers reliable and efficient solutions that help coffee manufacturers improve their operational efficiency and product quality.