

Working Principle and Features of Corn Kernels Pneumatic Conveying Systems
For those in the agricultural processing industry, the efficient and reliable handling of bulk materials like corn kernels is crucial to maintaining operational productivity and product quality. Pneumatic conveying systems have emerged as a preferred solution for transporting corn kernels due to their versatility and effectiveness in various processing environments. This article delves into the working principle and key features of corn kernels pneumatic conveying systems, highlighting how they contribute to streamlined material handling in agricultural and food processing applications.
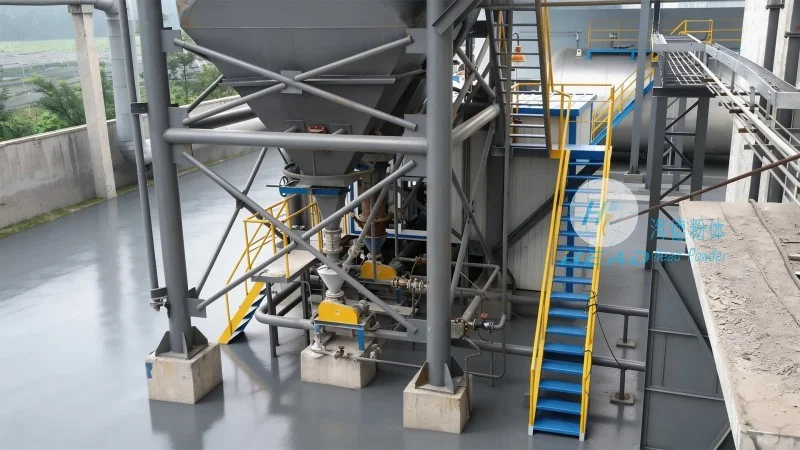
Understanding the Working Principle of Corn Kernels Pneumatic Conveying Systems
The core mechanism of a corn kernels pneumatic conveying system involves the use of air to transport solid particles through a pipeline. At its essence, the system operates by creating a pressure differential that propels the corn kernels from the source to the destination. There are primarily two types of pneumatic conveying systems: pressure and vacuum systems, each with distinct operational characteristics suited to different corn processing scenarios.
In a pressure system, compressed air is introduced into the conveying line at the discharge end, pushing the corn kernels forward. This method is often used for short to medium-distance transport and is particularly effective when the destination is at a higher elevation than the source. The pressure system ensures consistent flow rates and can handle a wide range of corn kernel sizes and moisture contents without causing excessive wear on the system components.
Conversely, vacuum systems utilize a vacuum pump to create a negative pressure at the inlet, drawing the corn kernels into the pipeline. This approach is ideal for longer distances or when the destination is at a lower elevation than the source. Vacuum systems are generally more energy-efficient for long-distance transport and can handle more delicate or fragile corn kernels with minimal breakage. Both systems rely on specialized equipment such as airlocks, cyclones, and filters to control the flow and ensure the corn kernels are conveyed safely and efficiently.
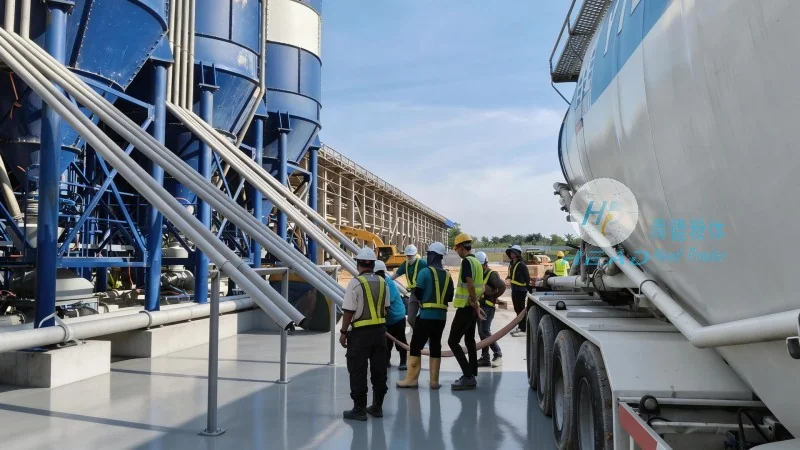
Key Features of Corn Kernels Pneumatic Conveying Systems
Several critical features distinguish corn kernels pneumatic conveying systems from other material handling technologies, making them a preferred choice for agricultural applications. These features include:
1. Gentle Material Handling: Unlike mechanical conveyors that may cause abrasion or breakage, pneumatic systems use air to move corn kernels, minimizing product damage. This is especially important for corn kernels, which can be sensitive to impact or friction during transport.
2. Versatility in Transport: Pneumatic conveying systems can handle a wide variety of corn kernel sizes, shapes, and moisture levels. They are adaptable to different processing stages, from raw corn kernel reception to storage or further processing, making them a flexible solution for diverse agricultural operations.
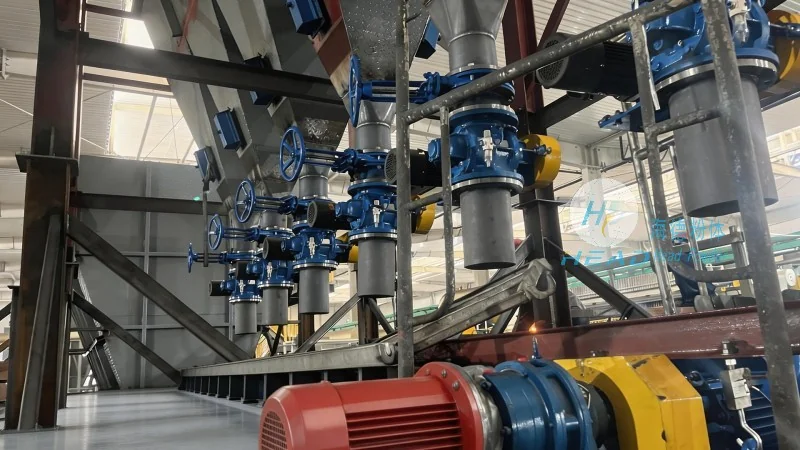
3. Dust Control and Environmental Benefits: By containing the corn kernels within a sealed pipeline, pneumatic systems effectively control dust and prevent contamination. This not only improves workplace safety but also maintains the quality of the corn kernels by preventing exposure to external elements or contaminants.
4. Energy Efficiency and Cost-Effectiveness: Compared to traditional conveyor systems, pneumatic conveying can be more energy-efficient, especially for longer distances. The reduced need for mechanical components and maintenance also contributes to lower operational costs over time.
5. Scalability and Customization: Modern pneumatic conveying systems are highly customizable, allowing manufacturers to tailor the system to specific operational needs. This includes adjusting the air pressure, flow rate, and pipeline design to optimize performance for different corn kernel types and processing requirements.
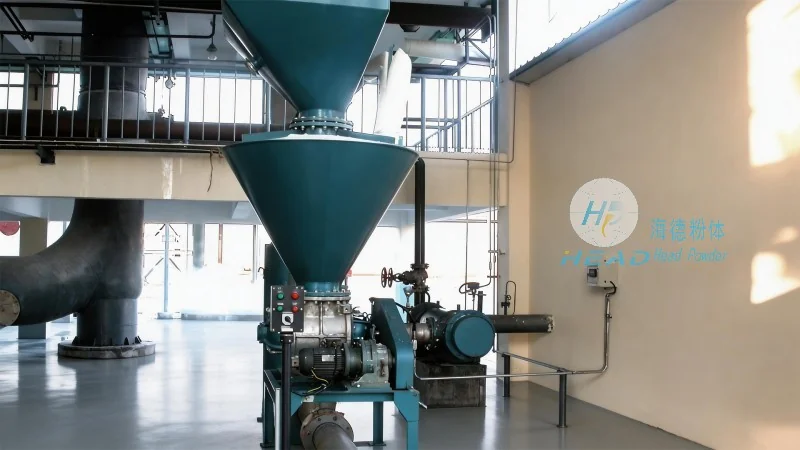
About Shandong HeadPowder Engineering Co., Ltd.
As a leading provider of engineering solutions for the agricultural and food processing industries, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the unique needs of corn kernel handling. With a focus on innovation and quality, the company has built a reputation for delivering reliable, efficient, and cost-effective solutions that enhance the productivity and sustainability of agricultural operations.
HeadPowder Engineering leverages years of industry experience to develop customized pneumatic conveying systems that meet the specific requirements of their clients. Their expertise in material handling technology ensures that each system is optimized for the safe and efficient transport of corn kernels, minimizing downtime and maximizing operational efficiency.
Based in Shandong, China, HeadPowder Engineering combines cutting-edge technology with local manufacturing capabilities to deliver high-quality products that meet international standards. The company’s commitment to customer satisfaction and technological advancement has made it a trusted partner for agricultural processing facilities worldwide.