

Working Principle and Features of Gray Calcium Powder Pneumatic Conveying Systems
Gray calcium powder is a widely used material in various industrial applications, and the efficient handling of this fine powder is crucial for maintaining production efficiency and product quality. Pneumatic conveying systems offer a reliable solution for transporting gray calcium powder from one location to another, ensuring minimal dust generation and contamination. This article explores the working principle and key features of such systems, providing insights into their operation and benefits.
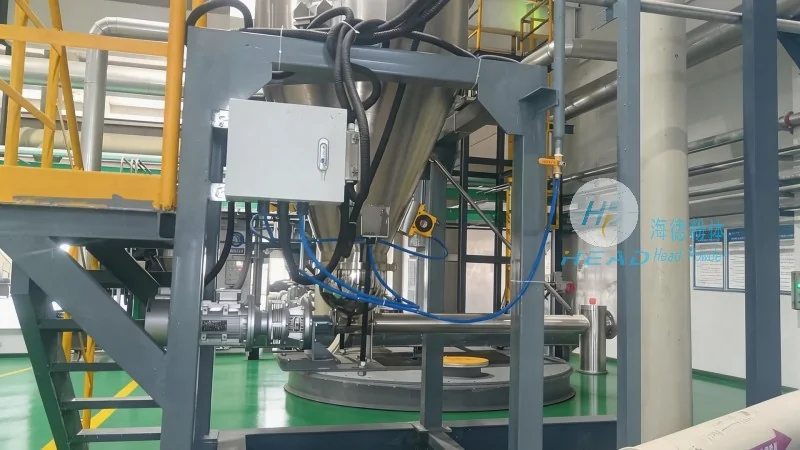
Working Principle of Gray Calcium Powder Pneumatic Conveying Lines
The core of a gray calcium powder pneumatic conveying system lies in its ability to use air as the conveying medium. The system typically consists of a feeding hopper, a conveyor pipeline, a blower or air compressor, and a discharge unit. The process begins with the powder being fed into the hopper. As the blower generates a high-pressure airflow, the powder is drawn into the pipeline and transported to the discharge point. The air and powder mixture is then separated at the discharge end, with the air being recirculated or vented, while the powder is collected in the receiving container. This continuous process ensures a steady flow of gray calcium powder without the need for mechanical components that might cause wear or contamination.
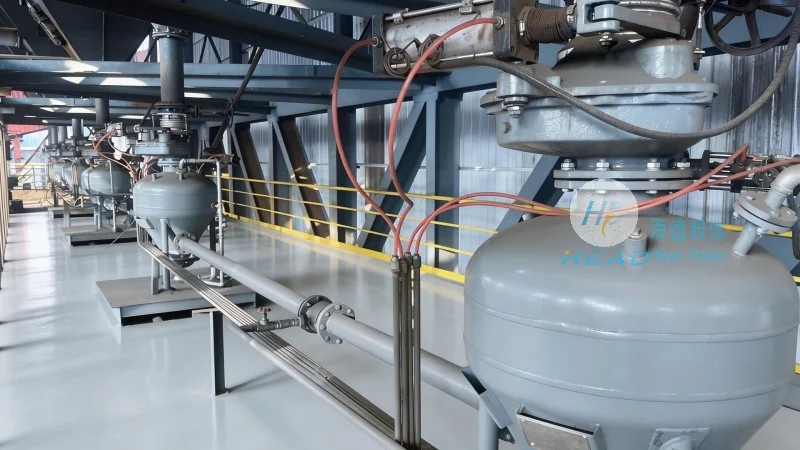
Key Features of Gray Calcium Powder Pneumatic Conveying Systems
Several distinct features make gray calcium powder pneumatic conveying systems an attractive choice for industrial applications. Firstly, they provide a dust-free and hygienic environment, which is essential for food and pharmaceutical industries where product purity is paramount. The enclosed system prevents dust from escaping into the workspace, reducing health risks and maintaining compliance with safety regulations. Secondly, these systems offer high flexibility in terms of layout and installation. They can be easily integrated into existing production lines, adapting to different plant layouts and space constraints. Thirdly, the operation is relatively simple and requires minimal maintenance. The absence of moving parts in the conveying line reduces the risk of mechanical failure and simplifies routine checks and repairs. Additionally, the system can handle a wide range of powder characteristics, including varying particle sizes and moisture content, making it versatile for different gray calcium powder types. The energy efficiency of pneumatic conveying is another notable feature, as it uses compressed air effectively to transport the material, minimizing energy consumption compared to other bulk material handling methods.
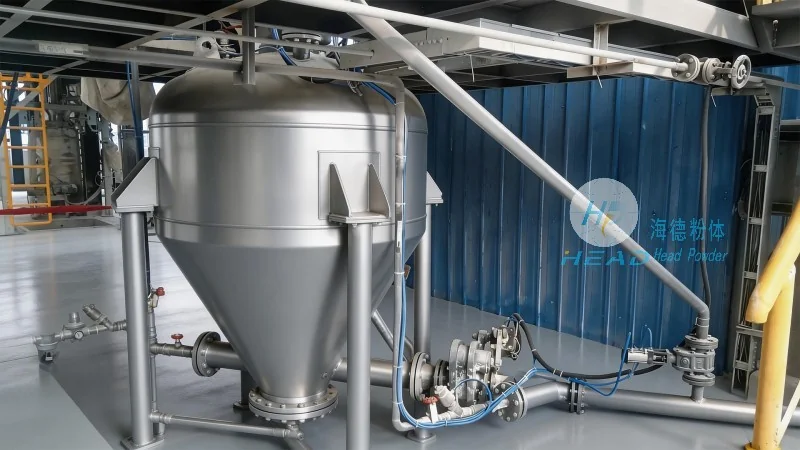
Applications and Benefits in Industrial Settings
Gray calcium powder pneumatic conveying systems are widely utilized in various industries, including construction, food processing, and chemical manufacturing. In the construction industry, they are used to transport gray calcium powder for cement production and other building materials, ensuring consistent quality and reduced downtime. In food processing, the hygienic design of these systems is critical for handling calcium supplements and other food additives, maintaining product safety and regulatory compliance. The benefits of using such systems extend beyond material handling efficiency; they also contribute to improved workplace safety by eliminating manual handling of powders, reducing the risk of respiratory issues and other health hazards. Furthermore, the consistent flow and reduced contamination levels lead to higher product quality and reduced waste, which are significant advantages for manufacturers aiming to enhance their operational performance.
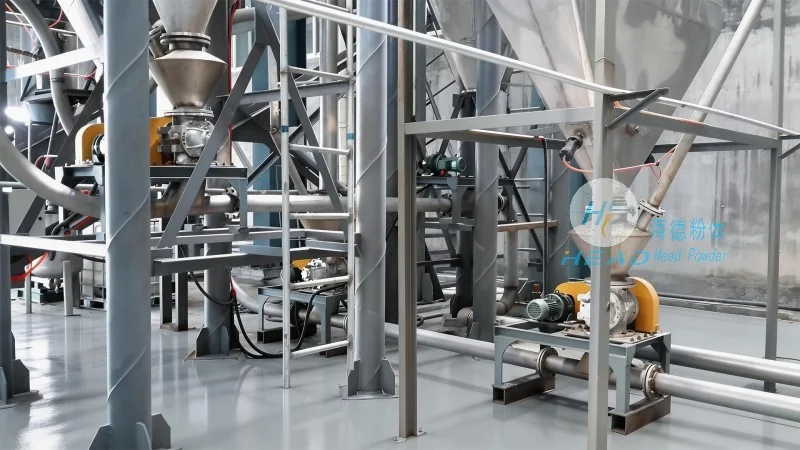
Conclusion and Company Overview
Gray calcium powder pneumatic conveying systems represent a sophisticated and efficient solution for the transportation of fine powders. By leveraging the principles of pneumatic transport, these systems offer reliable, hygienic, and flexible handling of gray calcium powder. The working principle, which involves the use of compressed air to move the material through an enclosed pipeline, ensures minimal dust and contamination, making them suitable for a variety of industrial applications. The key features, including dust-free operation, high flexibility, and low maintenance requirements, contribute to their widespread adoption in industries where product quality and safety are top priorities. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the specific needs of clients. With a focus on quality and innovation, the company ensures that its systems meet the highest standards of performance and reliability, supporting clients in achieving their production goals while maintaining operational efficiency and safety.