

Working Principle and Features of Small Bag Quantitative Weighing Material Conveying System
For industrial applications requiring precise and efficient handling of small bagged materials, the small bag quantitative weighing material conveying system offers a reliable solution. This system is designed to streamline the process of weighing, packaging, and transporting materials in a controlled environment, ensuring accuracy and consistency in every step. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. has developed this system to meet the demands of modern manufacturing and processing industries.
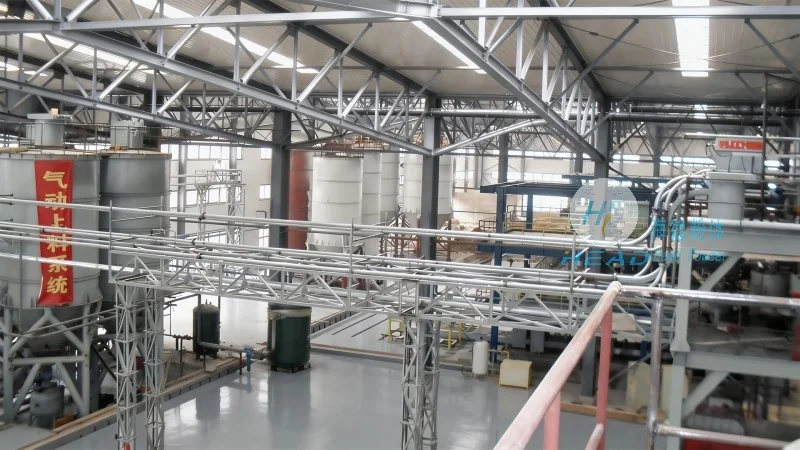
Overview of the Small Bag Quantitative Weighing Material Conveying System
The small bag quantitative weighing material conveying system is a sophisticated piece of equipment that integrates multiple functions to handle small bagged materials efficiently. It typically consists of components such as a conveyor belt, a weighing scale, a bagging unit, and a control system. The system is engineered to handle various types of materials, including powders, granules, and other bulk materials, ensuring that each bag is filled to the exact required weight. The system is designed with precision in mind, utilizing advanced technology to minimize errors and maximize productivity.
Working Principle of the System
The operation of the small bag quantitative weighing material conveying system involves several key steps. First, the material is fed into the system via a hopper or feeder. The conveyor belt then transports the material to the weighing scale, where the weight is measured. Once the desired weight is achieved, the system triggers the bagging unit to fill the bag. The filled bag is then transported to the next stage of the process, such as sealing or labeling. The control system monitors all operations, ensuring that each bag meets the specified weight and that the system operates smoothly. The system uses a closed-loop control mechanism to maintain accuracy, adjusting the feed rate as needed to achieve the target weight. This ensures that even with variations in material density or flow rate, the system can maintain consistent results.
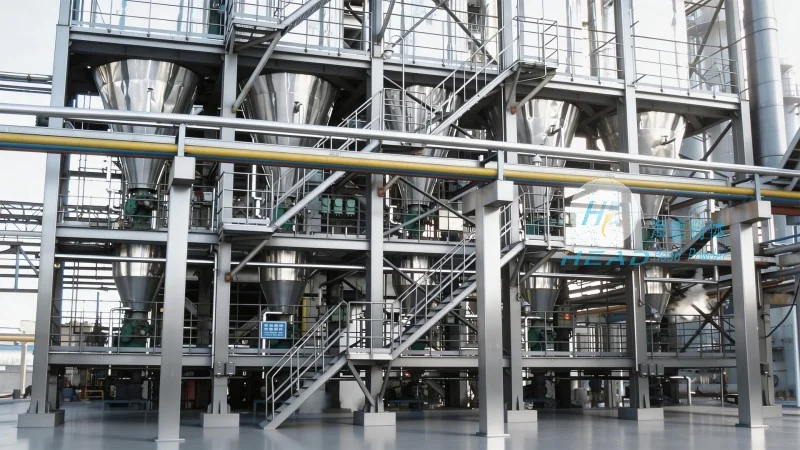
Key Features and Advantages
The small bag quantitative weighing material conveying system from Shandong HeadPowder Engineering Co., Ltd. offers several features that make it an ideal choice for industrial applications. One of the primary advantages is its high accuracy, which is crucial for applications where precise weight control is essential. The system is also highly efficient, with the ability to process a large number of bags per hour without compromising on quality. Another key feature is its versatility, as it can handle a wide range of materials and bag sizes. The system is also designed for easy maintenance and operation, with user-friendly controls and clear indicators for system status. Additionally, the system is built with durability in mind, using high-quality materials and components that can withstand the rigors of industrial use. The system also offers flexibility in terms of customization, allowing it to be adapted to specific customer requirements. This ensures that the system can be tailored to meet the unique needs of each application.
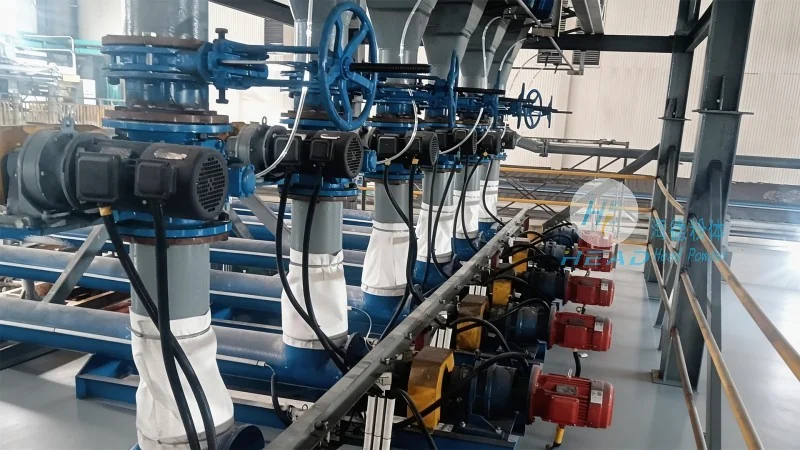
Applications and Industries
The small bag quantitative weighing material conveying system is widely used in various industries, including food processing, pharmaceuticals, chemicals, and agriculture. In the food industry, it is used to package ingredients such as flour, sugar, and spices with precision. In the pharmaceutical industry, it is used to package active ingredients and other components with strict weight control. In the chemical industry, it is used to package powders and granules for industrial applications. The system is also used in the agriculture industry to package fertilizers and other agricultural products. The versatility of the system makes it suitable for a wide range of applications, making it a valuable asset for any industrial operation.
Conclusion
Overall, the small bag quantitative weighing material conveying system from Shandong HeadPowder Engineering Co., Ltd. is a reliable and efficient solution for industrial material handling. Its advanced technology and precise operation ensure that each bag is filled to the exact required weight, while its versatility and durability make it suitable for a wide range of applications. The system is designed to meet the demands of modern manufacturing and processing industries, providing a cost-effective and efficient solution for material handling. With its high accuracy and efficiency, the system is an ideal choice for any industrial operation that requires precise and consistent material handling.