

Working Principle and Features of Ammonium Sulfate Powder Pneumatic Conveying Equipment
Ammonium sulfate is a widely used chemical fertilizer, and the efficient handling of its powder form is crucial for industrial operations. The pneumatic conveying system designed specifically for ammonium sulfate powder offers a reliable solution that combines advanced technology with practical application. This article will explore the working principle and key features of such equipment, highlighting how it enhances productivity and safety in material handling processes.
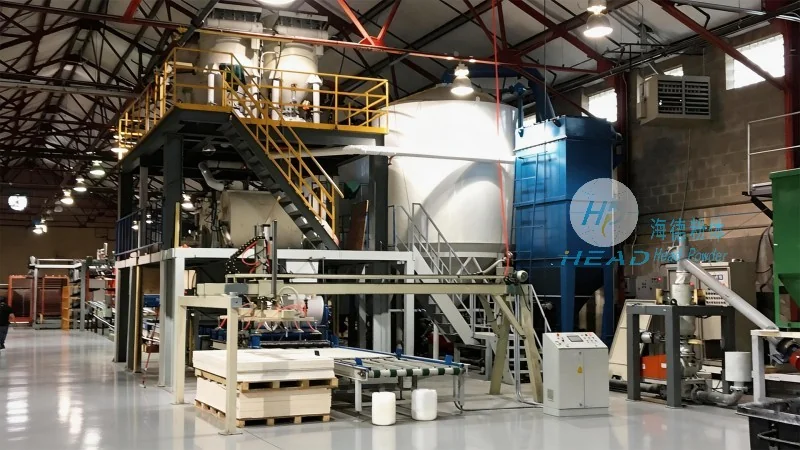
Understanding the Working Principle of Ammonium Sulfate Powder Pneumatic Conveying Equipment
The core of the pneumatic conveying system for ammonium sulfate powder lies in its ability to transport dry bulk materials through a pressurized or vacuum environment. The process typically begins with the material being fed into a hopper or feeder, where it is then drawn into a pipeline by a fan or blower. The air, which acts as the conveying medium, is introduced at a controlled velocity, creating a flow that carries the powder particles through the system. This method eliminates the need for mechanical components like belts or buckets, reducing friction and wear while ensuring a continuous, dust-free transfer. The system can operate under both positive pressure (where air is forced through the pipeline) and negative pressure (where air is drawn out), adapting to different industrial setups and material characteristics.
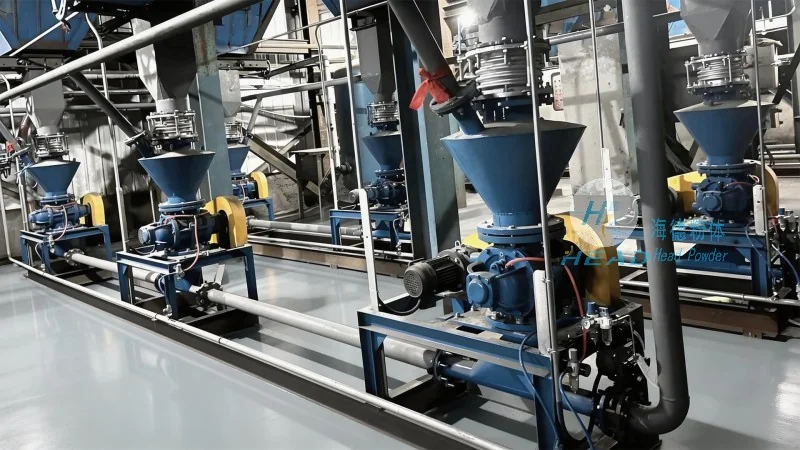
Key Features of the Ammonium Sulfate Powder Pneumatic Conveying System
Several distinct features make this equipment ideal for handling ammonium sulfate powder. First, its dust-free operation minimizes environmental contamination and health risks associated with fine powders. The enclosed system prevents dust from escaping into the workplace, aligning with safety regulations and maintaining a clean operational environment. Second, the system offers high efficiency in material transfer, with the ability to move large quantities of powder over considerable distances without the need for multiple transfer points. This reduces downtime and labor costs associated with manual handling or traditional conveying methods. Third, the equipment is designed for durability and low maintenance. The use of corrosion-resistant materials, such as stainless steel, ensures longevity even in the presence of moisture or acidic conditions, which are common in fertilizer processing. Additionally, the modular design allows for easy integration into existing production lines, providing flexibility for future expansions or modifications.
Application and Benefits in Industrial Settings
In industrial applications, the ammonium sulfate powder pneumatic conveying system proves to be a versatile and reliable choice. It is commonly used in fertilizer manufacturing plants, where large volumes of ammonium sulfate need to be moved from storage to processing units or packaging areas. The system's ability to handle fine powders without clogging or blockages is particularly advantageous, as ammonium sulfate can be prone to agglomeration under certain conditions. By maintaining consistent air flow and pressure, the equipment ensures smooth and uninterrupted operation, which is critical for maintaining production schedules. Furthermore, the system's compact design and low energy consumption contribute to operational cost savings, making it an economically viable solution for businesses in the chemical and agricultural sectors. The safety features, including pressure relief valves and emergency shut-off mechanisms, provide an additional layer of protection for operators and the facility.
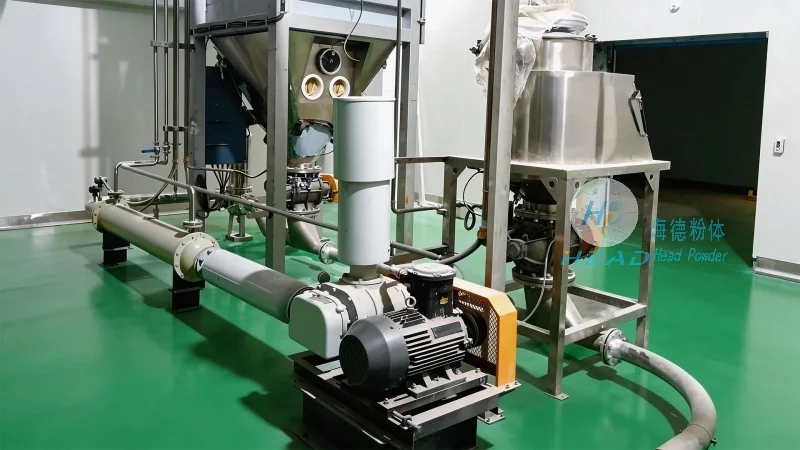
Conclusion and Company Information
Overall, the pneumatic conveying equipment for ammonium sulfate powder represents a sophisticated solution that addresses the unique challenges of handling fine, potentially hazardous materials. Its working principle, based on air-based transport, offers a clean, efficient, and safe method of material handling. The key features, including dust control, high capacity, and durability, make it a preferred choice for industrial applications. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems tailored to the specific needs of clients in the chemical and agricultural industries. With a focus on quality and innovation, the company ensures that its equipment meets the highest standards of performance and safety, supporting the efficient operation of fertilizer production and related processes.