

Working Principle and Features of the Camellia Seed Material Pneumatic Conveying System
Camellia seed material pneumatic conveying systems are advanced industrial solutions designed to efficiently transport camellia seeds and related materials. These systems utilize air pressure or vacuum to move materials through a pipeline network, offering a reliable and flexible method for material handling in processing facilities. The following sections will explore the working principle and key features of such systems, with a focus on their application in camellia seed processing operations.
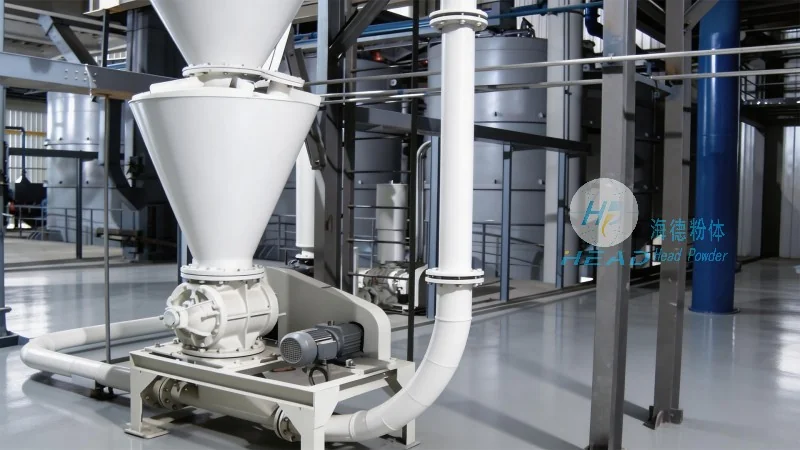
Working Principle of the Camellia Seed Material Pneumatic Conveying System
The core of a camellia seed material pneumatic conveying system is the air flow mechanism that propels the seeds through the system. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into a pipeline. A fan or blower generates the necessary air pressure or vacuum, creating a flow that carries the seeds along the pipeline. The system may employ different conveying modes, such as dilute-phase or dense-phase conveying, depending on the material characteristics and operational requirements. In dilute-phase conveying, the material is suspended in the air stream, while in dense-phase conveying, the material is carried in a more concentrated form. The selection of the conveying mode is critical for optimizing efficiency and minimizing material degradation. The system also includes components like filters, cyclones, and silos to separate the seeds from the air and store the material, ensuring a clean and efficient operation.
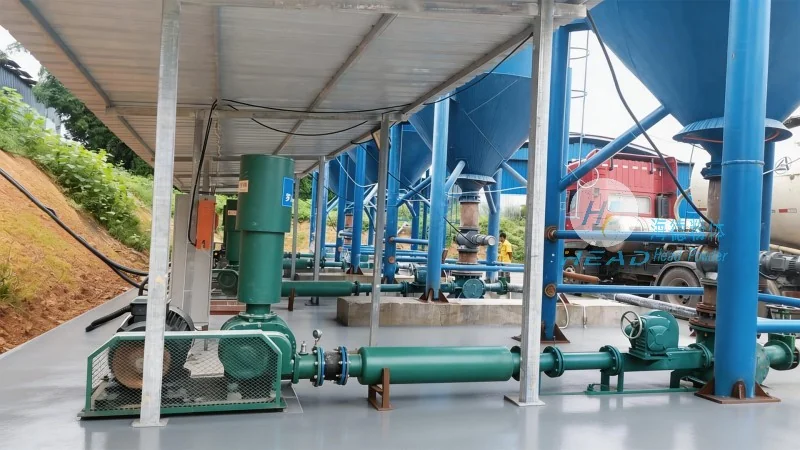
Key Features of the Camellia Seed Material Pneumatic Conveying System
Camellia seed material pneumatic conveying systems offer several advantages that make them ideal for industrial applications. One of the primary features is their ability to handle a wide range of material types, including camellia seeds with varying sizes and moisture content. The systems are designed to minimize material breakage and damage during transport, which is crucial for maintaining the quality of the seeds. Additionally, these systems provide a hygienic and dust-free environment, reducing the risk of contamination and improving safety in processing facilities. The flexibility of the system allows for easy integration with existing processing lines, and the modular design enables scalability to accommodate increased production demands. Another important feature is the energy efficiency of the system, as it can reduce energy consumption compared to traditional mechanical conveying methods. The system also offers high reliability and low maintenance requirements, ensuring consistent performance over time. Furthermore, the pneumatic conveying system can handle both bulk and small quantities of material, making it versatile for different processing stages.
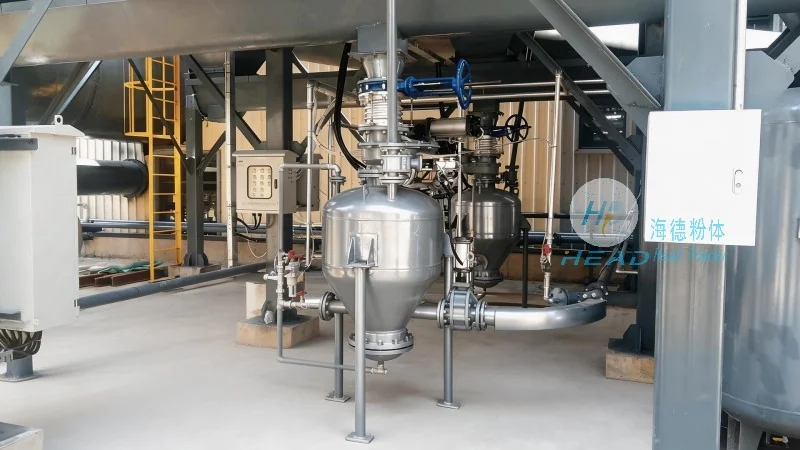
Application and Benefits in Camellia Seed Processing
In the context of camellia seed processing, the pneumatic conveying system plays a vital role in the material handling process. The system efficiently transports camellia seeds from storage areas to processing units, such as cleaning, sorting, and oil extraction equipment. This streamlined material flow enhances overall production efficiency and reduces downtime. The system's ability to maintain seed quality is particularly important, as it prevents damage that could affect the final oil yield and product quality. The hygienic design of the system also aligns with food processing standards, ensuring compliance with regulatory requirements. Moreover, the system's flexibility allows for adjustments in conveying capacity based on production schedules, providing operational flexibility. The reduced need for manual handling of seeds also improves workplace safety and reduces labor costs. Overall, the camellia seed material pneumatic conveying system is a critical component in modern processing facilities, contributing to improved productivity, quality control, and operational efficiency.
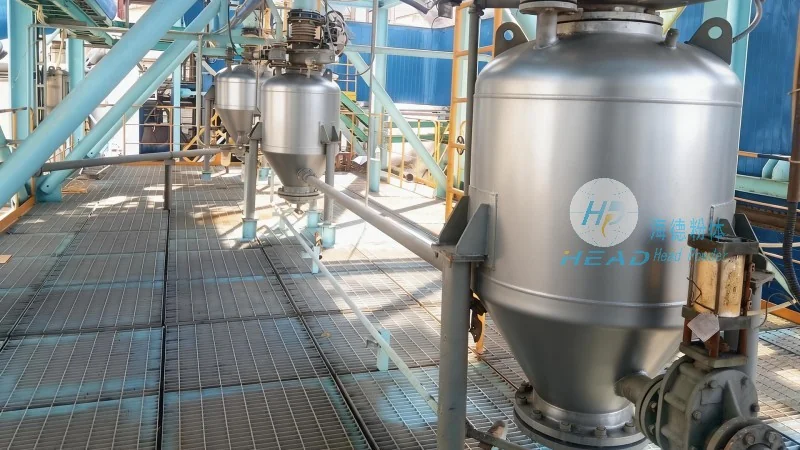
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of various industries, including food processing, pharmaceuticals, and chemical manufacturing. HeadPowder's expertise lies in providing customized solutions that enhance operational efficiency and ensure product quality. The company is committed to delivering reliable and durable equipment, backed by a team of experienced engineers and technicians. HeadPowder's facilities are located in Shandong, China, where the company maintains a strong presence in the industrial equipment market. The company's products are known for their advanced technology, robust construction, and adherence to international standards, making them a trusted choice for businesses seeking efficient material handling solutions.