

Operation Process and Working Principle of Coffee Bean Pneumatic Conveying Equipment
Coffee bean pneumatic conveying equipment plays a crucial role in the coffee processing industry, ensuring efficient and reliable transportation of coffee beans from storage to processing units. As a key component in modern coffee production lines, these systems are designed to handle the unique characteristics of coffee beans, such as their irregular shape, varying sizes, and sensitivity to moisture and pressure changes. The equipment from Shandong HeadPowder Engineering Co., Ltd. (commonly known as headpowder) exemplifies advanced engineering solutions tailored to meet the demands of coffee manufacturers worldwide.
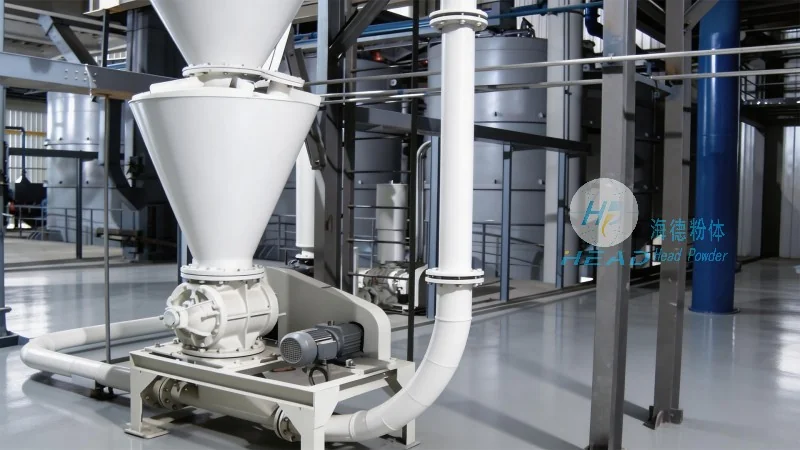
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Headpowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of high-quality pneumatic conveying systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for coffee processing plants seeking efficient and durable equipment. The company's facilities in Shandong are equipped with state-of-the-art technology and skilled professionals who ensure that each product meets stringent quality standards before delivery. By focusing on precision engineering and customer-specific solutions, headpowder delivers systems that enhance productivity and reduce operational costs for coffee producers.
Key Components of Coffee Bean Pneumatic Conveying Systems
The coffee bean pneumatic conveying system typically consists of several essential components that work in harmony to facilitate the transport of beans. These components include the hopper or storage silo, where coffee beans are initially stored; the air supply system, which generates the necessary airflow to move the beans; the conveying line, which may be made of flexible hoses or rigid pipes; and the receiver or discharge unit, where the beans are deposited at the processing location. Each component is carefully selected and engineered to handle the specific properties of coffee beans, ensuring minimal damage and optimal flow rates.
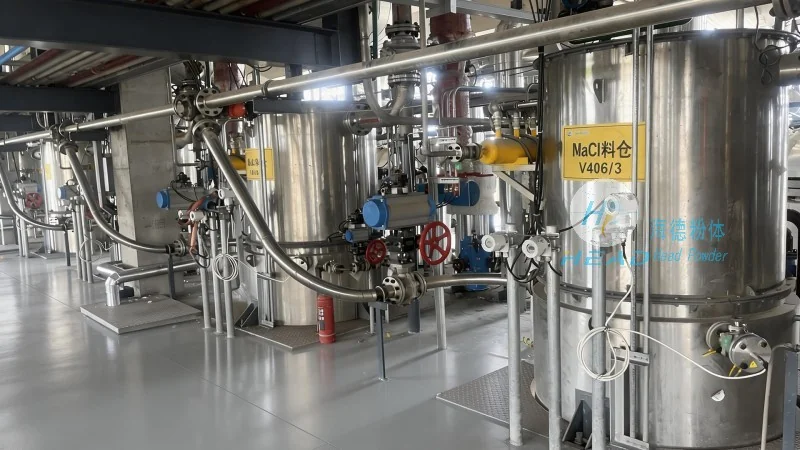
Operation Process of Coffee Bean Pneumatic Conveying Equipment
The operation of coffee bean pneumatic conveying equipment involves a series of steps that ensure the smooth and continuous movement of beans. The process begins with the loading of coffee beans into the hopper. Once the hopper is filled, the air supply system is activated, creating a low-pressure or high-pressure airflow depending on the system design. The coffee beans are then drawn into the conveying line by the airflow, moving from the storage area to the processing unit. The conveying line may include bends, elbows, or other fittings that are designed to maintain the flow without causing blockages or damage to the beans. At the discharge end, the beans are deposited into the receiver, where they are ready for further processing, such as roasting or packaging. The entire process is automated, with sensors and controls monitoring the flow rate, pressure, and other parameters to ensure consistent performance.
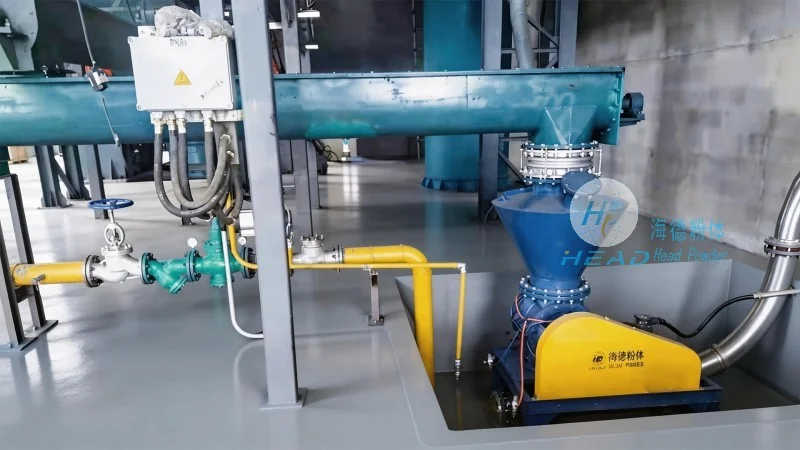
Working Principle of Pneumatic Conveying for Coffee Beans
The working principle of coffee bean pneumatic conveying relies on the fundamental concept of using air to transport solid materials. In a low-pressure system, also known as a suction system, the air is drawn through the conveying line, creating a negative pressure that pulls the coffee beans into the line. The beans are then carried by the airflow to the destination. In a high-pressure system, the air is forced through the line, pushing the beans forward. Both systems utilize the principles of fluidization and drag to move the beans efficiently. The key to successful operation is maintaining the correct air velocity and pressure to prevent clogging and ensure that the beans are transported without excessive friction or impact. The design of the conveying line, including its diameter and length, is critical in determining the optimal air velocity and pressure required for the specific coffee bean characteristics and system layout.
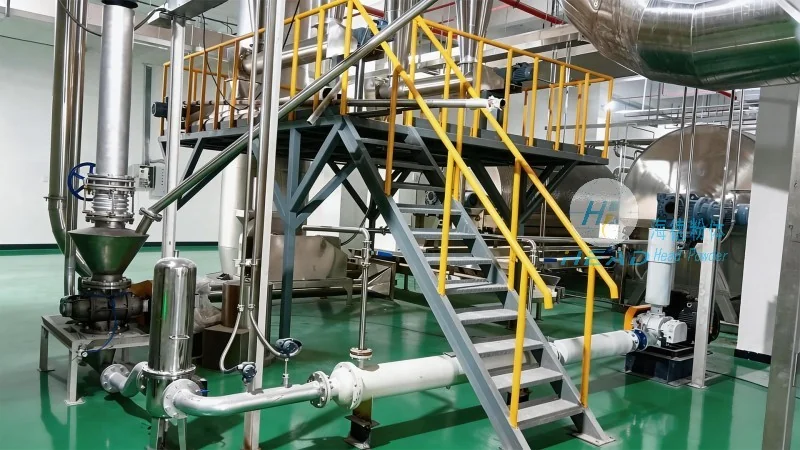
Advantages of Using Pneumatic Conveying for Coffee Beans
Implementing coffee bean pneumatic conveying equipment offers several advantages over traditional methods like belt conveyors or bucket elevators. One of the primary benefits is the ability to transport beans in a closed system, which helps maintain hygiene and prevent contamination from external factors. This is particularly important in food processing environments where cleanliness is paramount. Additionally, pneumatic conveying systems are more flexible in terms of layout, allowing for vertical, horizontal, or mixed-direction transport without the need for complex infrastructure. The equipment also reduces the risk of damage to coffee beans, as the beans are conveyed gently by the airflow rather than being subjected to mechanical friction or impact. Furthermore, these systems can be integrated with other processing equipment, such as roasters or grinders, to create a seamless production line, enhancing overall efficiency and reducing labor costs.
Customization and Application in Coffee Processing
Headpowder provides customized coffee bean pneumatic conveying solutions tailored to the specific needs of each coffee processing plant. The company works closely with clients to understand their production volumes, bean characteristics, and operational requirements, then designs a system that optimizes performance and meets budget constraints. Whether for small-scale artisanal coffee roasters or large industrial coffee processing facilities, headpowder's systems are adaptable and scalable. The company's engineers consider factors such as the type of coffee beans (e.g., Arabica or Robusta), the desired flow rate, and the distance between storage and processing units to develop the most effective conveying system. Customization may include adjustments to the air pressure, conveying line diameter, or the addition of special features like filters or cyclones to enhance separation and cleaning. By offering tailored solutions, headpowder ensures that each client receives a system that is perfectly suited to their unique coffee processing needs.