

Introduction to Straw Ash Pneumatic Conveying System Equipment: Overview and Structural Principles
Straw ash pneumatic conveying systems are critical components in modern agricultural and industrial processing, designed to efficiently transport fine materials like straw ash from one location to another. This equipment is essential for optimizing material handling processes, reducing labor costs, and enhancing operational efficiency in facilities that handle agricultural residues or byproducts. The system's design integrates advanced engineering principles to ensure reliable and consistent performance, making it a valuable asset for companies involved in biomass processing, waste management, or related industries.
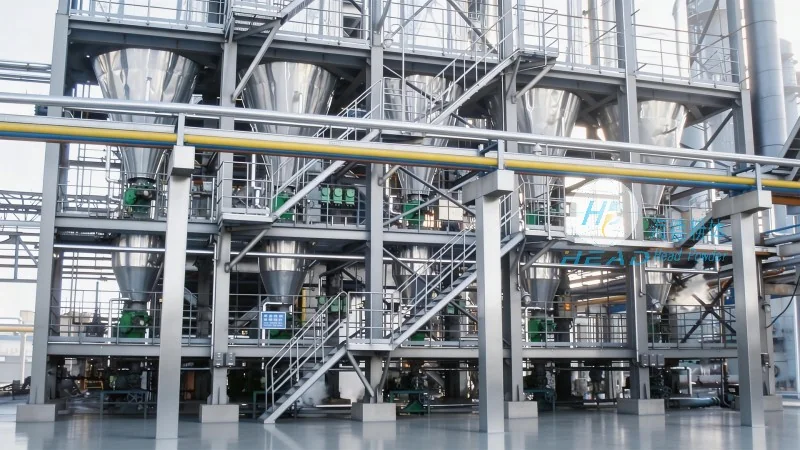
Overview of Straw Ash Pneumatic Conveying System Equipment
Straw ash pneumatic conveying systems are specialized devices engineered to transport dry, fine materials such as straw ash through an air stream. These systems are widely used in agricultural processing facilities, biomass energy plants, and waste management operations due to their ability to handle materials that are difficult to transport using traditional methods like gravity or mechanical conveyors. The primary goal of these systems is to provide a cost-effective and efficient means of moving materials over short to medium distances, often within industrial or agricultural settings. The equipment typically consists of several key components, including a hopper for material storage, a conveyor line, and a control system to regulate the air flow and material movement. By leveraging the force of compressed air, the system can transport materials without the need for physical contact, minimizing wear and tear on equipment and reducing the risk of material degradation.
Structural Principles of the Pneumatic Conveying System
The structural design of a straw ash pneumatic conveying system is based on the fundamental principle of pneumatic transport, where material particles are suspended and carried by an air stream. The system's core components include a material hopper, which holds the straw ash and feeds it into the conveyor line. The hopper is equipped with a feeding mechanism, such as a rotary valve or a screw feeder, that controls the flow rate of the material into the system. The conveyor line itself is a tube or pipe through which compressed air is introduced, creating a pressure differential that propels the material forward. The air flow is regulated by a blower or compressor, which provides the necessary pressure and volume to move the material efficiently. The system may also include a filter or separator to remove any moisture or debris from the air stream, ensuring the material remains dry and free of contaminants. Additionally, the design incorporates safety features such as pressure relief valves and emergency shut-off mechanisms to prevent over-pressurization and ensure safe operation.
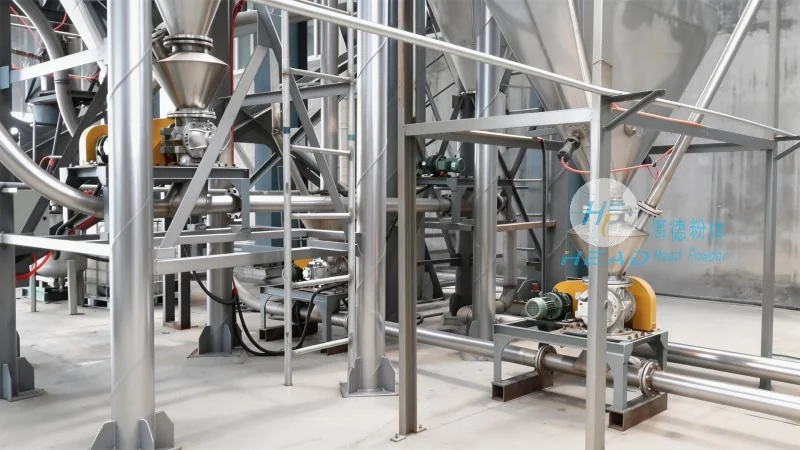
Key Features and Benefits of the System
The straw ash pneumatic conveying system offers several advantages over traditional material handling methods. One of the most significant benefits is its ability to transport materials over long distances with minimal energy consumption. The system's design minimizes friction and material degradation, resulting in higher material recovery rates and lower operational costs. Additionally, the equipment is compact and easy to install, making it suitable for both new and existing facilities. The system's flexibility allows it to handle a wide range of material sizes and types, from fine powders to larger particles, without requiring significant modifications. Another key feature is the system's ability to integrate with other processing equipment, such as grinders or classifiers, to form a complete material handling solution. This integration enhances overall process efficiency and reduces the need for manual intervention. The system also provides real-time monitoring and control capabilities, allowing operators to adjust parameters such as air flow and material feed rate to optimize performance and ensure consistent output.
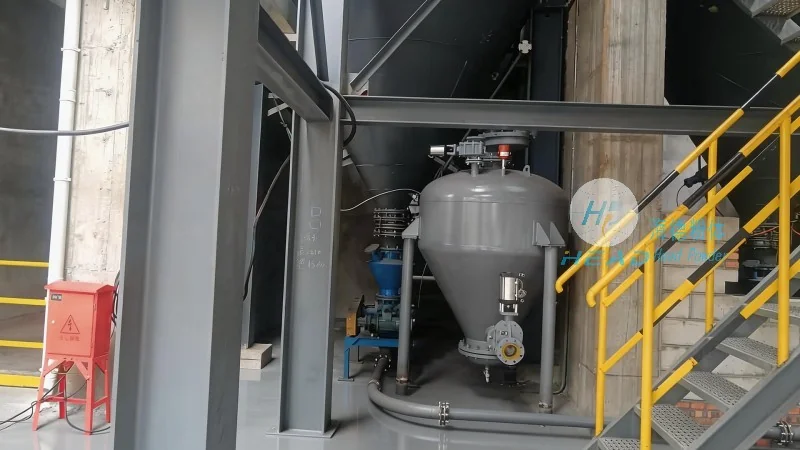
Application Scenarios and Operational Considerations
Straw ash pneumatic conveying systems are commonly used in various applications, including biomass processing plants, agricultural residue handling facilities, and waste management operations. In biomass plants, the system is used to transport straw ash from the combustion chamber to storage or processing areas, ensuring a continuous and efficient supply of material for energy generation. In agricultural facilities, the system can be used to move straw ash from fields or storage silos to processing units, facilitating the conversion of agricultural residues into valuable products. The system's performance is influenced by several factors, including the material's properties (such as particle size, moisture content, and density), the system's design (such as the length and diameter of the conveyor line), and the operating conditions (such as air pressure and flow rate). Proper maintenance and regular inspection of the system are essential to ensure optimal performance and prevent downtime. The system's components, such as the blower and conveyor line, require periodic cleaning and lubrication to maintain efficiency and prevent wear. Additionally, the system should be equipped with appropriate safety features to protect operators from potential hazards, such as high-pressure air or moving parts.
Conclusion and Company Information
Straw ash pneumatic conveying systems are a vital component in modern material handling processes, offering efficient and reliable solutions for transporting fine materials like straw ash. The system's design, based on pneumatic transport principles, provides a cost-effective and environmentally friendly alternative to traditional methods. By integrating advanced engineering and control systems, these systems enhance operational efficiency and reduce labor costs. For companies seeking to optimize their material handling processes, the straw ash pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers a robust and reliable solution. With years of experience in the industry, HeadPowder specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to meet the specific needs of its clients. The company's commitment to quality and innovation ensures that its products meet the highest standards of performance and durability. Whether for agricultural or industrial applications, the straw ash pneumatic conveying system from HeadPowder is an excellent choice for businesses looking to improve their material handling capabilities and enhance overall operational efficiency.