

Introduction to Water-Containing Powder Pneumatic Conveying System Equipment and Its Structural Prin
Headpowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for the efficient handling of water-containing powders. This article provides a comprehensive introduction to the equipment, its structural components, and the underlying principles that enable effective material transport in industrial applications.
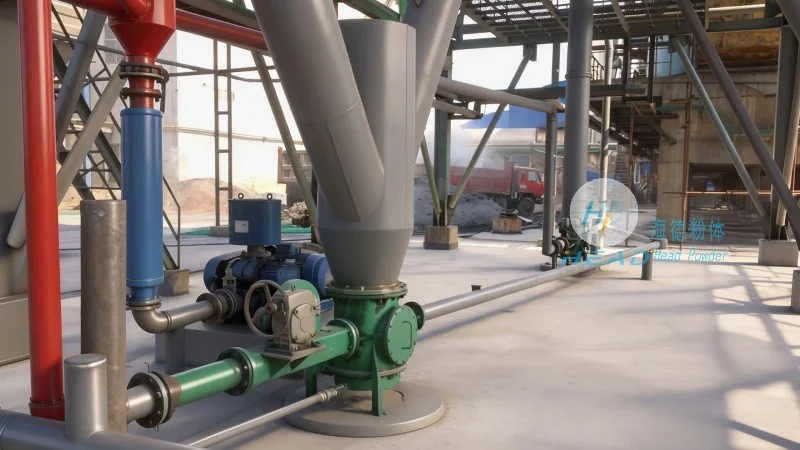
Key Components of the Water-Containing Powder Pneumatic Conveying System
The water-containing powder pneumatic conveying system consists of several critical components that work in tandem to ensure reliable and efficient material transport. The primary elements include a hopper for material storage, a pump or blower to generate the necessary air pressure, a pipeline network for conveying the mixture, and a separation unit to recover the powder from the air stream. Each component is engineered to handle the unique challenges posed by water-containing powders, such as moisture content, agglomeration, and varying particle sizes.
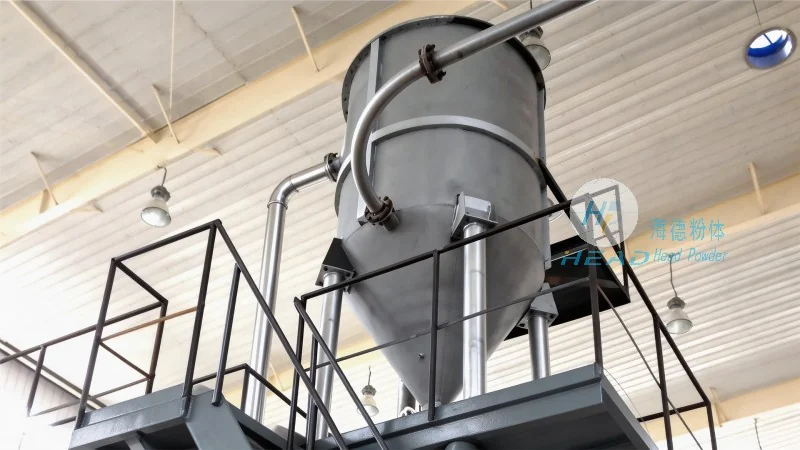
Structural Principles and Working Mechanism
The system operates on the principle of pneumatic transport, where air is used as the medium to move the powder. The water-containing powder is first introduced into the hopper, where it is mixed with a controlled amount of water to form a slurry or paste. The pump then draws this mixture and injects it into the pipeline, where the air pressure propels the slurry forward. As the mixture travels through the pipeline, the air and powder separate at the receiving end, with the powder being collected in a designated container and the air being filtered and discharged. This process minimizes material loss and ensures a clean, efficient transfer of the product.
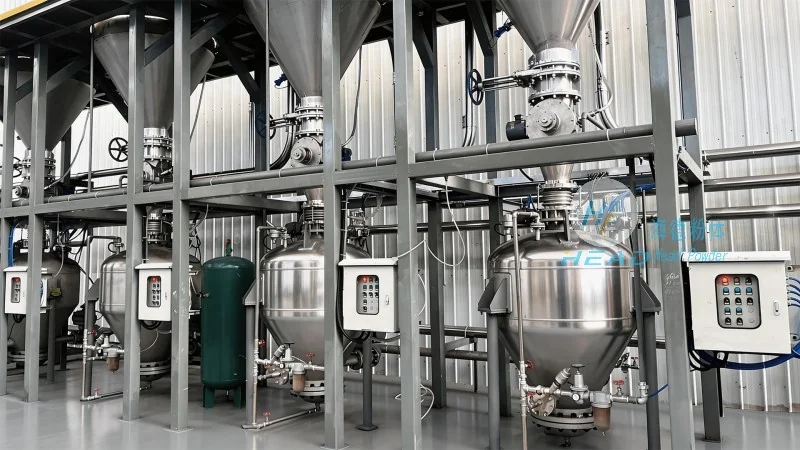
Advantages of the Water-Containing Powder Pneumatic Conveying System
Compared to traditional mechanical conveying methods, the water-containing powder pneumatic conveying system offers several advantages. It eliminates the need for moving parts in the conveying line, reducing maintenance costs and increasing operational reliability. The system also provides better control over the material flow, allowing for precise dosing and consistent product quality. Additionally, the use of water helps to prevent dust generation and improves the handling properties of the powder, making it safer and more environmentally friendly for industrial applications.
Applications in Industrial Settings
The water-containing powder pneumatic conveying system is widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, it is employed to transport ingredients like flour, sugar, and spices that may contain moisture, ensuring hygienic and efficient handling. In pharmaceutical applications, the system helps maintain the purity and sterility of powders by minimizing contamination and cross-contamination. In chemical processing, it facilitates the transport of wet powders, such as those used in cement or fertilizer production, improving production efficiency and reducing downtime.
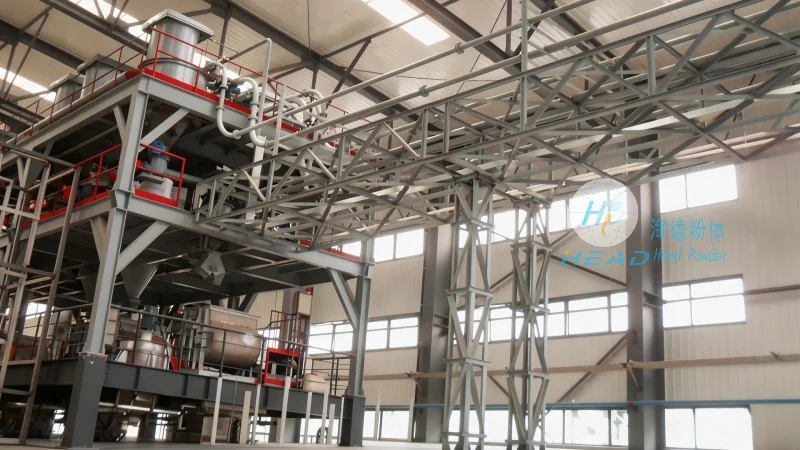
Customization and Installation Services by Headpowder
Headpowder understands that each industrial application has unique requirements, and therefore offers customized solutions tailored to specific needs. The company provides comprehensive installation and commissioning services, ensuring that the system is properly integrated into existing production lines and operates at optimal efficiency. With a team of experienced engineers and technicians, Headpowder ensures that the water-containing powder pneumatic conveying system meets the highest standards of performance and reliability, delivering long-term value to its clients.