

Analysis of Purified Ash Pneumatic Conveying Systems
For industrial applications involving the handling of purified ash, the selection of an efficient and reliable material transport solution is critical to operational efficiency and environmental compliance. Among the various methods available, pneumatic conveying systems have emerged as a preferred choice due to their ability to transport powders and fine particulates with minimal dust generation and reduced maintenance requirements. This article provides an in-depth analysis of a specialized pneumatic conveying system designed for purified ash, highlighting its design principles, operational advantages, and practical applications.
Pneumatic Conveying Systems: Core Principles and Advantages
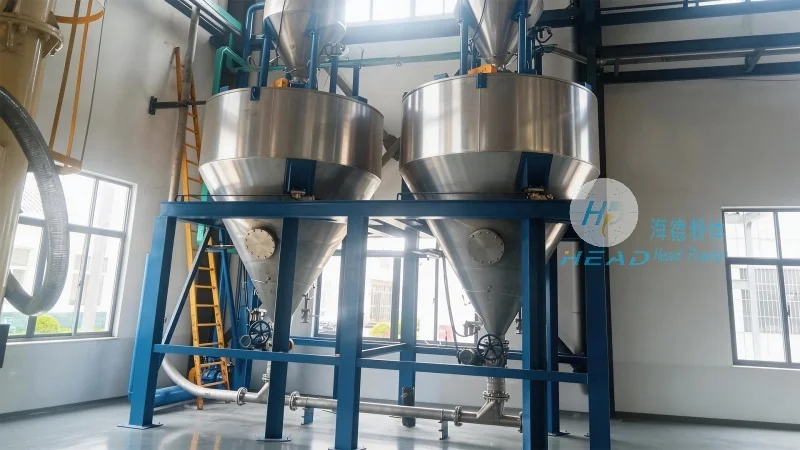
Pneumatic conveying systems utilize air or gas to transport bulk materials through a pipeline network. Unlike mechanical systems such as screw conveyors or belt conveyors, pneumatic systems offer several distinct advantages. They are capable of transporting materials over long distances, often with minimal pressure drops, and can handle a wide range of particle sizes and moisture contents. The primary benefit lies in their ability to minimize dust exposure, which is particularly important when dealing with purified ash, as it often contains fine particles that can be hazardous if released into the environment. Additionally, pneumatic systems are generally more flexible in terms of layout, allowing for changes in the material flow path without major structural modifications.
Design Considerations for Purified Ash Handling
The design of a pneumatic conveying system for purified ash must address several key factors to ensure optimal performance and durability. First, the system must be capable of handling the specific properties of purified ash, including its particle size distribution, bulk density, and moisture content. These characteristics influence the selection of air velocity, pressure, and pipeline diameter. For instance, higher air velocities may be required to prevent particle settling in the pipeline, while lower velocities can reduce energy consumption. The material's abrasiveness is another critical factor, as it can lead to wear on the system components, necessitating the use of high-quality materials such as stainless steel or specialized coatings.
Components and Operational Mechanisms
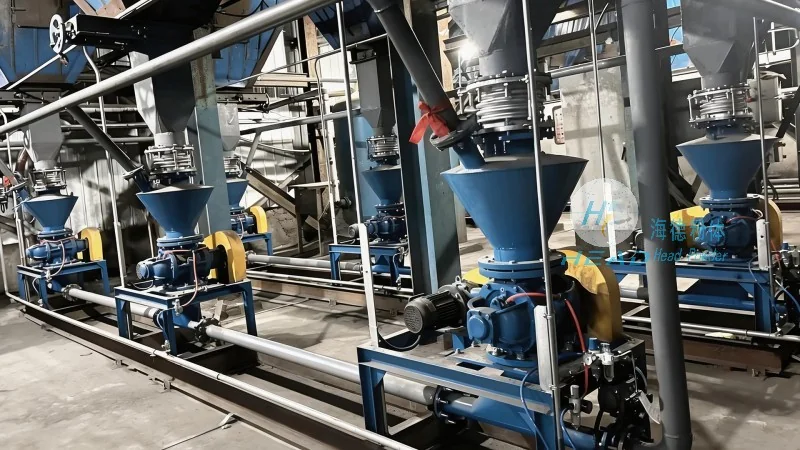
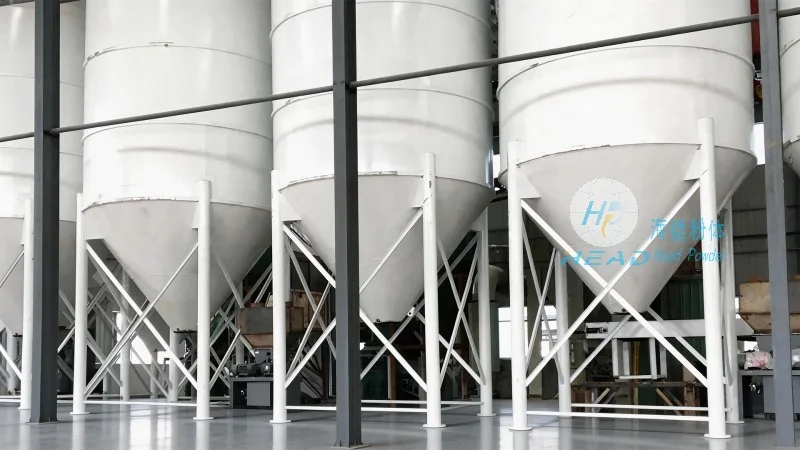
A typical pneumatic conveying system for purified ash consists of several key components, each playing a vital role in the material transport process. The system begins with a feeding unit, which can be a rotary valve or a hopper with a gate mechanism, designed to control the flow of ash into the pipeline. The feeding unit is connected to a blower or compressor that generates the necessary air pressure to move the material. The pipeline itself is usually made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of the ash and prevent contamination. Along the pipeline, there may be in-line mixers or agitators to maintain the material's flow and prevent blockages. At the end of the pipeline, a receiver or silo is used to collect the conveyed ash, which can then be discharged through a discharge valve or further processed.
Advantages of the HeadPowder Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, has developed a specialized pneumatic conveying system tailored for purified ash applications. This system incorporates advanced engineering principles to enhance efficiency and reliability. The system features a high-efficiency blower that minimizes energy consumption while maintaining sufficient air pressure to transport the ash over long distances. The pipeline design includes smooth, internally lined components to reduce friction and prevent material buildup, ensuring consistent flow rates. Additionally, the system incorporates dust collection and filtration systems to meet environmental regulations, ensuring that no ash particles are released into the atmosphere during operation. The modular design of the system allows for easy installation and maintenance, reducing downtime and operational costs.

Applications and Performance Metrics
The HeadPowder pneumatic conveying system for purified ash has been successfully implemented in various industrial settings, including power plants, cement factories, and waste treatment facilities. In these applications, the system has demonstrated superior performance in terms of material transport efficiency, with minimal pressure drops and consistent flow rates. The system's ability to handle fine particles and maintain low dust levels has contributed to improved workplace safety and reduced environmental impact. Performance metrics, such as the system's capacity (typically ranging from 10 to 50 tons per hour depending on the application), energy consumption (approximately 0.5 to 1.2 kW per ton of ash transported), and operational uptime (exceeding 95% in most installations), highlight the system's reliability and cost-effectiveness.
Conclusion and Future Developments
In conclusion, the pneumatic conveying system for purified ash developed by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in material handling technology. By combining advanced design principles with robust construction, the system offers a reliable and efficient solution for transporting purified ash while minimizing environmental impact. As industrial demands for cleaner and more sustainable operations continue to grow, such systems will play an increasingly important role in the future of material handling. Ongoing research and development efforts by HeadPowder focus on further improving energy efficiency, enhancing material compatibility, and expanding the system's capabilities to handle more diverse ash compositions, ensuring that the technology remains at the forefront of industrial material transport solutions.