

Grain Handling Systems: An Overview of Pneumatic Conveying Advantages
Efficient and reliable grain handling is crucial for the modern agricultural and food processing industries. As global food demand continues to grow, the need for advanced grain handling systems has become increasingly important. In this context, pneumatic grain conveying systems have emerged as a preferred solution for many operations, offering a range of advantages that traditional methods cannot match.
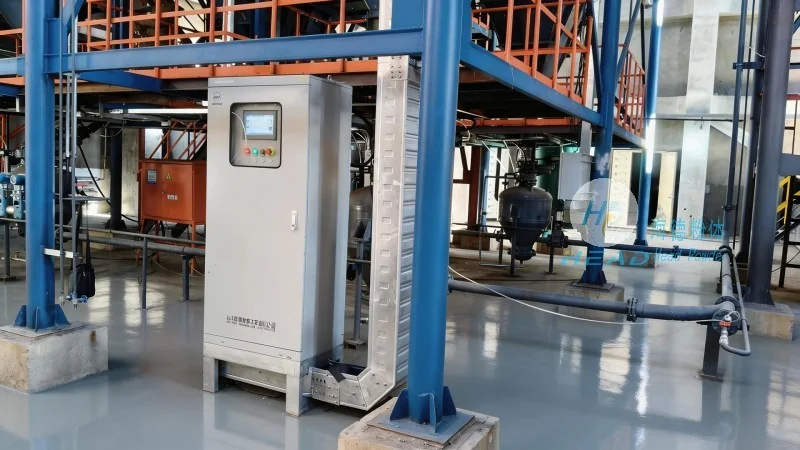
HeadPowder: A Leader in Grain Handling Technology
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer and supplier of grain handling equipment. With a strong presence in China, particularly in Shandong, the company has built a reputation for delivering high-quality, durable, and efficient grain conveying solutions. HeadPowder specializes in designing and manufacturing pneumatic conveying systems tailored to the specific needs of various industries, including grain processing, storage, and distribution.
The Core Advantages of Pneumatic Grain Conveying
Pneumatic grain conveying, also known as air conveying, is a method that uses air pressure to transport bulk materials like grains, seeds, and other dry agricultural products. This technology offers several key advantages over traditional mechanical conveying methods. First, it provides a highly efficient and flexible means of transporting grain over long distances and varying elevations. The ability to move materials vertically and horizontally with minimal equipment makes it ideal for complex processing facilities.
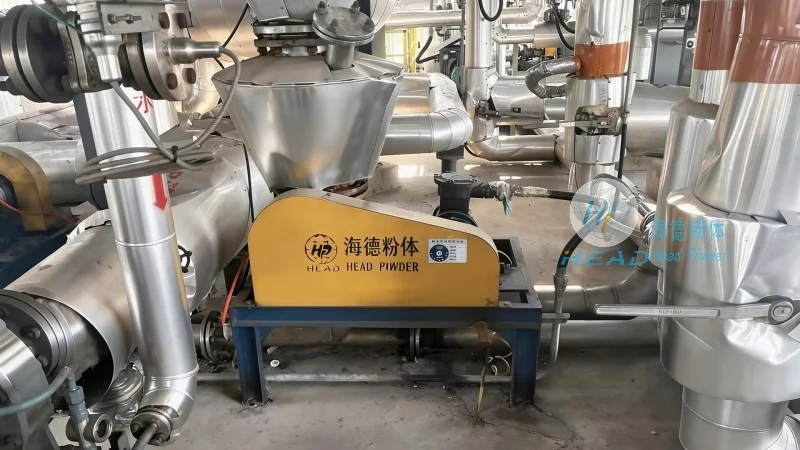
Second, pneumatic conveying systems are known for their low maintenance requirements and reduced operational costs. Unlike mechanical systems that rely on moving parts and bearings, air conveying uses a sealed pipeline system, minimizing wear and tear. This results in lower maintenance expenses and longer equipment lifespan. Additionally, the system operates with lower energy consumption compared to other bulk material handling methods, contributing to cost savings and environmental benefits.
Key Features and Benefits of Pneumatic Grain Conveying
One of the most significant benefits of pneumatic grain conveying is its ability to handle a wide variety of grain types and sizes without causing damage or degradation. The gentle handling of materials ensures that the quality of the grain is preserved throughout the conveying process. This is particularly important for delicate products like wheat, rice, and other cereals, where maintaining grain integrity is essential for quality control and market value.
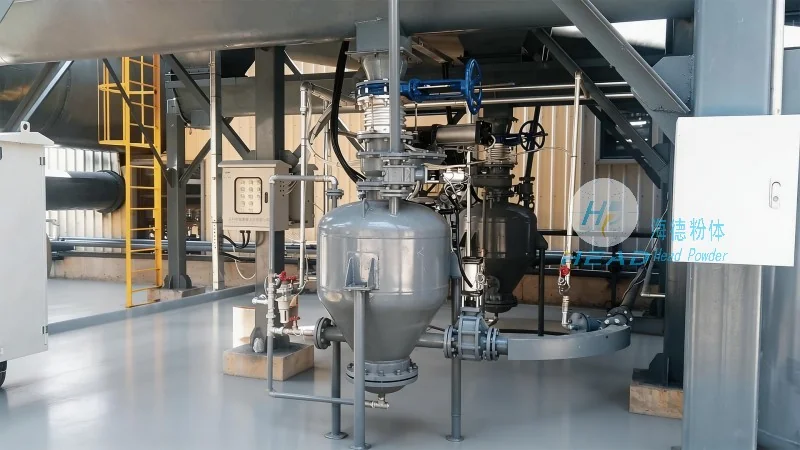
Another advantage is the system's adaptability to different operational conditions. Pneumatic conveyors can be easily integrated into existing processing lines or designed as standalone systems. They can handle both low and high volumes of material, making them suitable for small-scale farms as well as large industrial facilities. The flexibility in design allows for customization to meet specific operational requirements, such as varying conveyor speeds, pressure levels, and material flow rates.
Environmental and Safety Considerations
Pneumatic grain conveying systems also offer environmental and safety advantages. By using a sealed pipeline system, the method minimizes dust emissions and prevents contamination from external sources. This is crucial for maintaining a clean and safe working environment in grain processing facilities. Additionally, the enclosed system reduces the risk of fire hazards associated with open-air handling of flammable grain products.
Application Examples and Industry Impact
HeadPowder's pneumatic grain conveying systems are widely used in various applications across the agricultural and food processing sectors. For instance, in grain mills and processing plants, these systems efficiently transport raw materials from storage silos to processing equipment, such as cleaners, grinders, and sorters. In storage facilities, pneumatic conveyors are used to move grain between different storage bins or to loading docks for distribution. The technology also plays a vital role in the handling of by-products and waste materials, ensuring a smooth and continuous workflow.
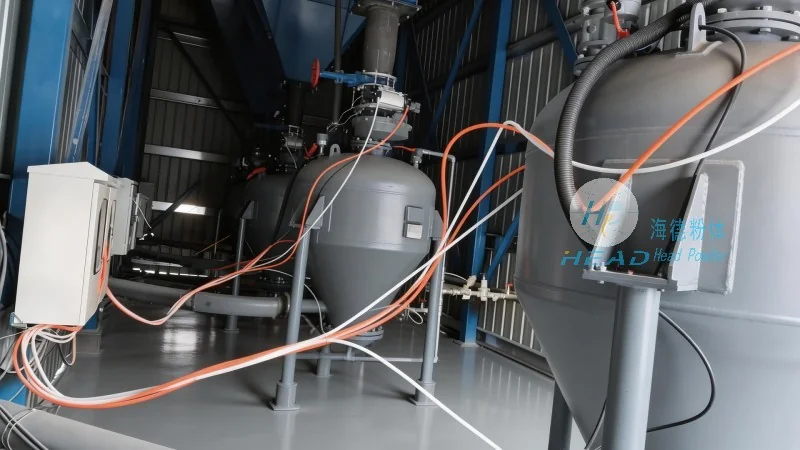
The impact of pneumatic grain conveying on the industry extends beyond efficiency gains. By reducing labor costs and improving product quality, these systems contribute to increased profitability for businesses. The ability to handle large volumes of grain quickly and reliably also supports the overall productivity of processing operations, helping to meet market demands in a timely manner.
Conclusion: The Future of Grain Handling with HeadPowder
As the demand for efficient grain handling solutions continues to rise, pneumatic conveying technology remains a cornerstone of modern agricultural operations. Shandong HeadPowder Engineering Co., Ltd. stands at the forefront of this technology, providing innovative and reliable solutions that address the evolving needs of the industry. By leveraging the advantages of pneumatic grain conveying, businesses can enhance their operational efficiency, reduce costs, and ensure the quality of their products. With a commitment to quality and customer satisfaction, HeadPowder is poised to continue leading the way in grain handling technology, supporting the global food supply chain with advanced and sustainable solutions.