

Introduction to Organic Salt Transport Systems and the Advantages of Organic Salt Pneumatic Conveyin
Organic salt transport systems are critical in industrial applications where efficient and safe material handling is essential. These systems are designed to handle organic salts, which often present unique challenges due to their chemical properties and physical characteristics. The primary goal of such systems is to ensure reliable, low-maintenance operation while minimizing environmental impact and operational costs.
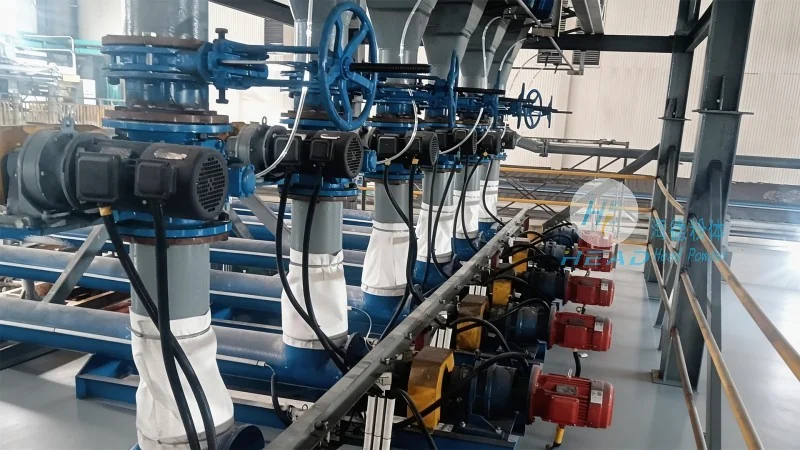
Overview of Organic Salt Transport Systems
Organic salt transport systems typically consist of several key components, including feeders, conveyors, and control systems. The system design is tailored to the specific requirements of the organic salt being handled, such as particle size, moisture content, and chemical reactivity. A well-designed system ensures that the organic salt is transported from its source to the processing or storage location without degradation or contamination.
The Advantages of Organic Salt Pneumatic Conveying
Pneumatic conveying, particularly in the context of organic salt transport, offers several distinct advantages over traditional mechanical conveying methods. One of the most significant benefits is the ability to handle fine or powdery organic salts without the need for additional equipment like hoppers or chutes. This reduces the risk of material buildup and improves overall system efficiency. Additionally, pneumatic conveying systems can be designed to operate in a closed loop, minimizing dust emissions and enhancing workplace safety.
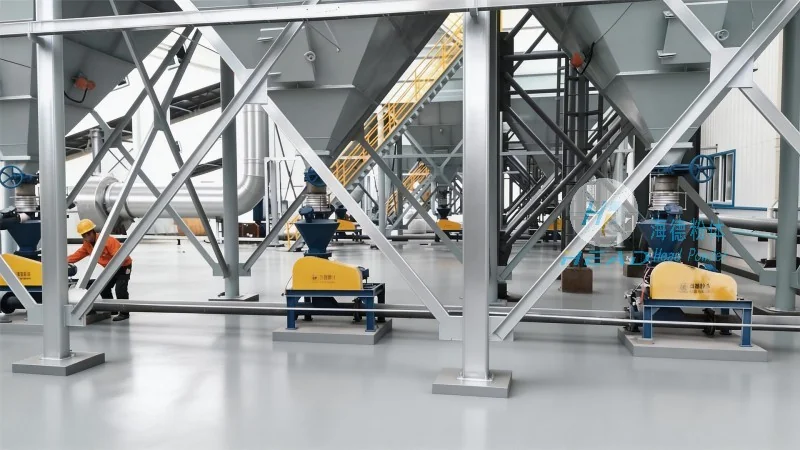
Key Features of Organic Salt Pneumatic Conveying Systems
Organic salt pneumatic conveying systems are equipped with specialized components that address the unique challenges of organic salts. For instance, the use of high-quality materials resistant to corrosion and chemical attack is essential to prevent degradation of the system over time. The control systems are often integrated with sensors to monitor pressure, flow, and temperature, ensuring optimal performance and early detection of any issues. Furthermore, these systems can be configured for both dilute and dense phase conveying, allowing flexibility in handling different organic salt types and throughput requirements.
Applications and Industries Served
The organic salt transport systems developed by Shandong HeadPowder Engineering Co., Ltd. are widely used in various industries, including chemical manufacturing, food processing, and pharmaceuticals. In these sectors, the reliable and efficient transport of organic salts is crucial for maintaining production continuity and product quality. The systems are designed to meet stringent industry standards, ensuring compliance with safety and environmental regulations.
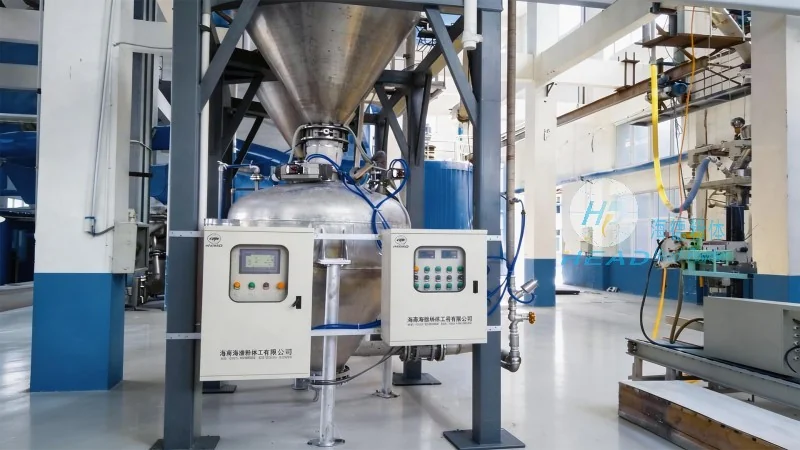
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced material handling solutions. With a focus on innovation and customer-centric design, the company specializes in the development and manufacturing of organic salt transport systems and pneumatic conveying equipment. HeadPowder's expertise lies in creating customized solutions that address the specific needs of each client, ensuring long-term operational efficiency and cost-effectiveness.
Location and Service Area
HeadPowder is headquartered in Shandong, China, where the company leverages its local resources and expertise to serve clients both domestically and internationally. The company's facilities are equipped with state-of-the-art technology and a skilled workforce, enabling the production of high-quality organic salt transport systems that meet global standards. By maintaining a strong presence in the region, HeadPowder ensures timely support and service for its clients, reinforcing its position as a trusted partner in the material handling industry.