

Introduction to Cement Granule Conveying Systems: Advantages and Features of Cement Granule Pneumati
HeadPowder, a leading provider of industrial conveying solutions, specializes in cement granule conveying systems. With a strong presence in Shandong, China, the company has established itself as a trusted partner for businesses seeking efficient and reliable methods to transport cement granules. This article explores the cement granule conveying system, highlighting its key features and the advantages of pneumatic conveying technology.
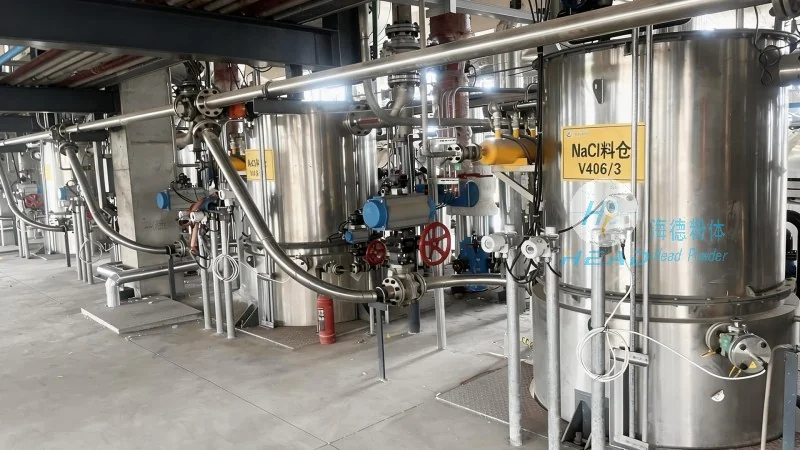
HeadPowder: Pioneering Cement Granule Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. is dedicated to delivering high-quality, customized conveying systems tailored to the unique needs of the cement industry. HeadPowder's expertise lies in designing and manufacturing efficient cement granule conveying systems that ensure smooth operation, minimal downtime, and optimal performance. The company's commitment to innovation and customer satisfaction has made it a preferred choice for clients across various sectors.
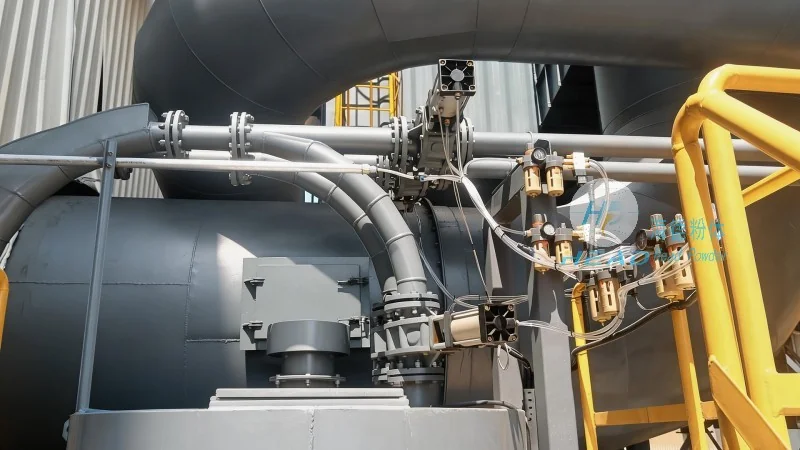
Cement Granule Conveying Systems: An Overview
Cement granule conveying systems are critical infrastructure in the cement manufacturing process, responsible for the efficient movement of bulk cement from storage silos to various processing stages. These systems are designed to handle the specific characteristics of cement granules, such as their fine particle size, abrasive nature, and tendency to generate dust. The primary goal of a cement granule conveying system is to transport the material with minimal loss, contamination, and operational disruption. A typical system consists of a hopper that collects the cement from the silo, a feeder that regulates the flow of material, a pneumatic conveying line that uses compressed air to move the granules, and a discharge unit that delivers the cement to the next stage of production. The entire system is engineered to operate smoothly, with each component working in tandem to ensure consistent and reliable performance.
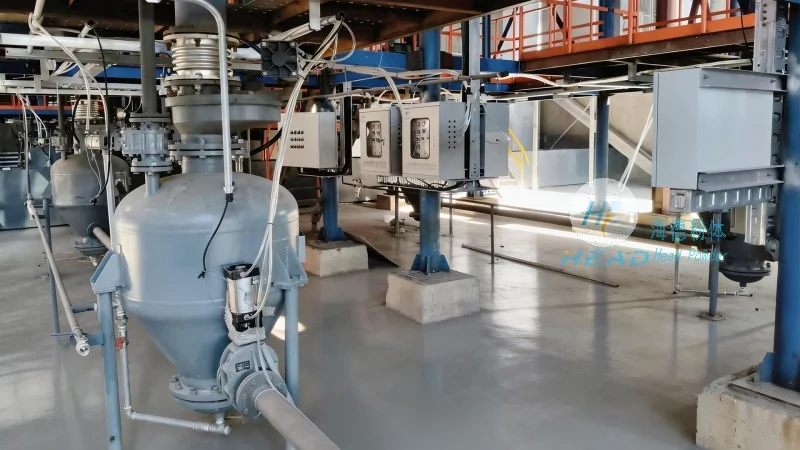
Advantages of Cement Granule Pneumatic Conveying
Pneumatic conveying is a preferred method for cement granule transport due to its numerous advantages over traditional mechanical systems. One of the key benefits is the ability to handle fine and abrasive materials without causing wear and tear on equipment. The system operates under low pressure, reducing energy consumption and operational costs. Additionally, pneumatic conveying allows for the integration of multiple conveying lines, enabling the simultaneous transport of different materials or the transfer of cement from multiple silos to a central processing unit. The enclosed nature of the system also prevents dust contamination, ensuring a cleaner working environment and compliance with environmental regulations. Furthermore, pneumatic conveying systems are less prone to blockages compared to mechanical systems, as the air flow helps to keep the material moving continuously.
Key Features of Cement Granule Conveying Systems
Modern cement granule conveying systems are equipped with several features that enhance their performance and efficiency. Advanced control systems enable real-time monitoring and adjustment of conveying parameters, ensuring optimal operation. The use of high-quality materials, such as stainless steel and corrosion-resistant components, prolongs the lifespan of the equipment and maintains the purity of the cement granules. Additionally, the systems are designed for easy maintenance, with accessible components that can be serviced quickly, minimizing downtime. HeadPowder's systems also incorporate safety features, such as pressure relief valves and emergency shut-off mechanisms, to protect both the equipment and personnel. The integration of sensors and alarms allows for early detection of issues, preventing potential failures and ensuring continuous operation.
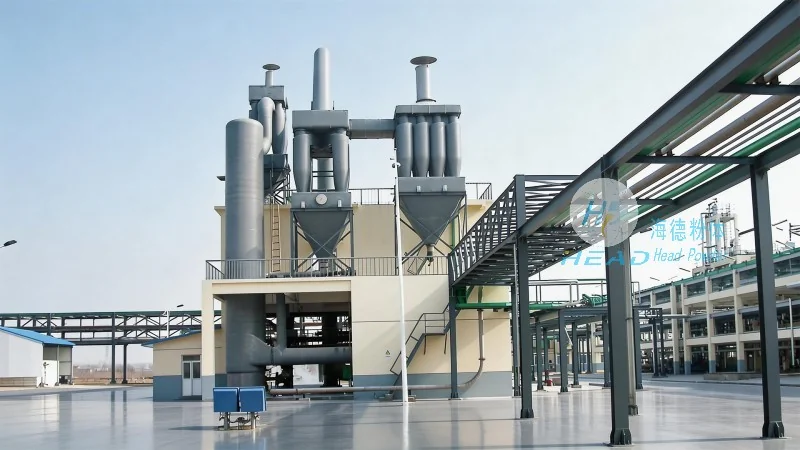
Customization and Application in Cement Industry
HeadPowder understands that each cement production facility has unique requirements. Therefore, the company offers customized cement granule conveying solutions that can be tailored to specific production capacities, material characteristics, and operational conditions. Whether it's a small-scale operation or a large industrial plant, HeadPowder's systems are designed to meet the demands of the cement industry. The company's experienced engineers work closely with clients to assess their needs and develop a conveying system that maximizes efficiency and reduces operational costs. From initial design and installation to ongoing maintenance and support, HeadPowder provides comprehensive services to ensure the long-term success of its clients' operations. The company's systems are widely used in cement plants, precast concrete facilities, and construction material distribution centers, demonstrating their versatility and reliability in various applications.