

Types and Applications of Coffee Powder Pneumatic Conveying Systems
Coffee powder handling is a critical process in the coffee production and distribution chain. Efficient and reliable transportation of coffee powder from production sites to processing facilities or packaging areas is essential for maintaining product quality and operational efficiency. Pneumatic conveying systems have emerged as a preferred solution for this task, offering advantages such as minimal product contamination, reduced risk of dust explosions, and the ability to handle fine powders like coffee powder effectively. This article explores the different types of coffee powder pneumatic conveying systems, their key features, and the various applications where they are commonly used.
Types of Coffee Powder Pneumatic Conveying Systems
There are primarily two main categories of pneumatic conveying systems used for coffee powder: positive pressure systems and negative pressure systems. Each type has distinct characteristics and is suitable for different operational requirements.
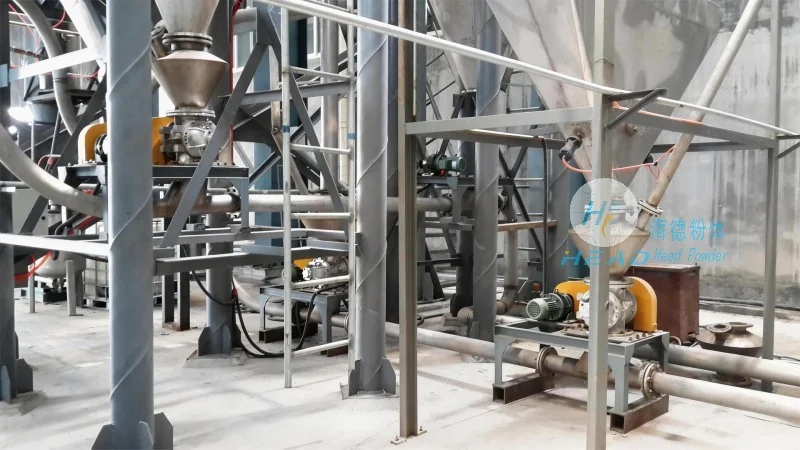
Positive pressure systems, also known as pressure conveying systems, operate by blowing air or a carrier gas into the conveying line, pushing the coffee powder forward. These systems are typically used for short to medium-distance conveying and are effective for handling dry, free-flowing powders. The headpowder company, Shandong HeadPowder Engineering Co., Ltd., specializes in designing and manufacturing such systems tailored to coffee processing needs. Positive pressure systems often feature high-pressure blowers and robust piping to ensure consistent flow and prevent blockages.
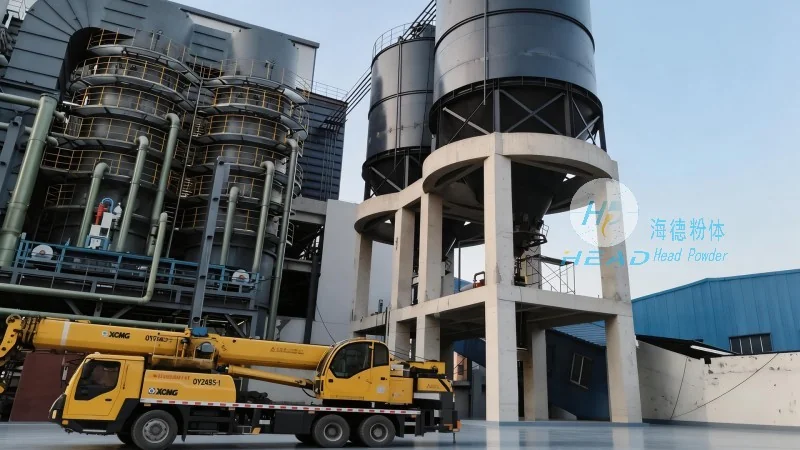
Negative pressure systems, or vacuum conveying systems, work by creating a vacuum in the conveying line, drawing the coffee powder into the system. This method is ideal for longer distances and for handling powders that are more prone to dust or require a more gentle handling process. Negative pressure systems are commonly used in applications where product containment and dust control are paramount. The engineering expertise of Shandong HeadPowder Engineering Co., Ltd. enables the design of vacuum systems that maintain low pressure differentials while ensuring efficient material transport.
Key Features of Coffee Powder Pneumatic Conveying Systems
Regardless of the type, modern coffee powder pneumatic conveying systems share several key features that enhance performance and reliability. One of the most important features is the ability to handle fine, abrasive powders without causing excessive wear on system components. Coffee powder, being a fine and sometimes sticky material, requires systems with smooth, corrosion-resistant internal surfaces and durable materials of construction. The systems from Shandong HeadPowder Engineering Co., Ltd. utilize high-quality materials such as stainless steel and specialized coatings to minimize wear and maintain product purity.
Another critical feature is the system's ability to control and regulate flow rates precisely. This is essential for maintaining consistent product quality and preventing overloading or underloading of downstream equipment. Advanced control systems, often integrated with the conveying equipment, allow operators to adjust air pressure, flow rate, and conveying distance in real-time. The company's engineering solutions include sophisticated control panels and sensors that provide feedback on system performance, ensuring optimal operation.
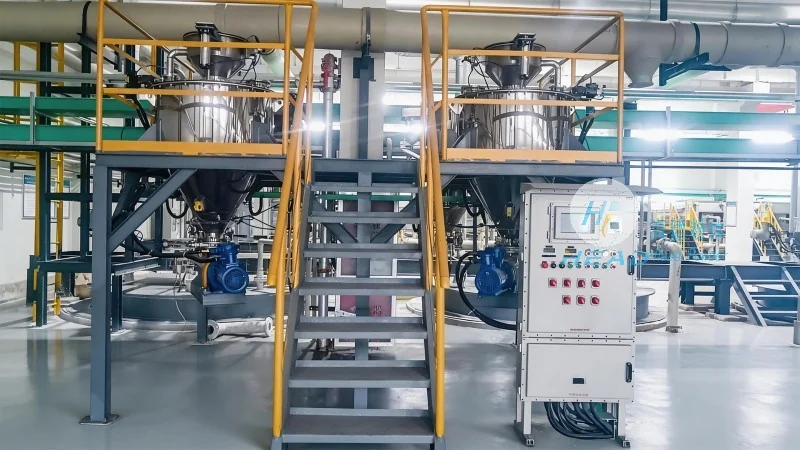
Additionally, modern coffee powder pneumatic conveying systems are designed with safety and environmental considerations in mind. Features such as explosion-proof components, dust collection systems, and leak detection mechanisms are standard in many designs. These safety measures are particularly important in coffee processing facilities where dust accumulation can pose fire hazards. The systems from Shandong HeadPowder Engineering Co., Ltd. comply with international safety standards and are engineered to minimize environmental impact while maximizing operational efficiency.
Applications of Coffee Powder Pneumatic Conveying Systems
Coffee powder pneumatic conveying systems are widely used across various stages of the coffee supply chain. In the production phase, these systems are used to transport freshly ground coffee from roasting machines to storage silos or packaging lines. The gentle handling provided by pneumatic systems helps preserve the aroma and flavor of the coffee, which is crucial for maintaining product quality. The headpowder company's systems are specifically designed to handle the high volumes and varying moisture content of freshly roasted coffee powder.
In the processing and blending stages, pneumatic conveying is used to move coffee powder between different processing units, such as decaffeination or flavoring equipment. This allows for seamless integration of various processing steps and ensures that the coffee powder is mixed uniformly. The systems are also used to transport blended coffee powders to packaging facilities, where they are loaded into bags or containers for distribution.
Furthermore, coffee powder pneumatic conveying systems are utilized in quality control and testing processes. For example, small quantities of coffee powder can be conveyed to laboratory equipment for analysis, ensuring that product specifications are met. The precision and reliability of these systems make them ideal for such applications, where accuracy is paramount.
Finally, in the distribution and storage stages, pneumatic conveying systems are used to transport coffee powder from storage silos to loading areas or to other processing facilities. This allows for efficient inventory management and reduces the need for manual handling, which can be labor-intensive and risky. The systems from Shandong HeadPowder Engineering Co., Ltd. are designed to handle large volumes of coffee powder, ensuring that supply chains remain smooth and uninterrupted.