

Activated Carbon Pneumatic Conveying Turnkey Project
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, installation, and commissioning of turnkey activated carbon pneumatic conveying systems. These systems are engineered to efficiently transport activated carbon, a critical material in various industrial applications such as air purification, water treatment, and chemical processing.
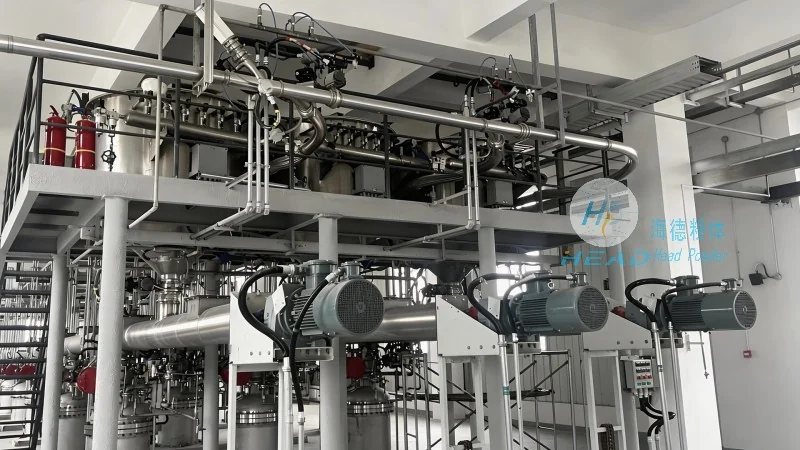
Understanding Activated Carbon Pneumatic Conveying
Activated carbon is widely used for its adsorption properties, making it indispensable in processes that require removal of impurities or contaminants. Traditional methods of handling activated carbon, such as manual handling or bulk handling with conveyors, often present challenges like dust generation, material loss, and operational inefficiencies. Pneumatic conveying systems offer a solution by using air to transport the material in a closed system, minimizing dust exposure and ensuring a cleaner, more controlled process.
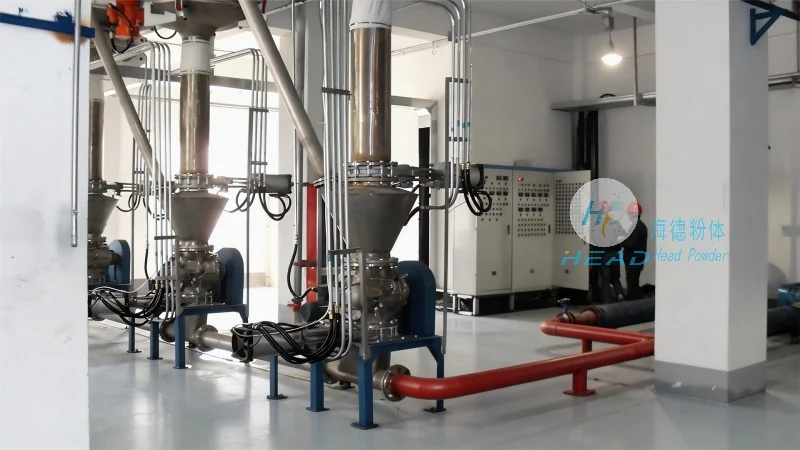
Key Features of Our Turnkey Activated Carbon Conveying Solutions
Our turnkey projects are tailored to meet the specific needs of clients, ensuring optimal performance and reliability. The systems are designed with high-quality components, including specialized pumps, airlocks, and material handling equipment, all selected to handle the unique characteristics of activated carbon. The engineering process involves thorough analysis of the client's operational requirements, material flow rates, and environmental considerations to develop a customized solution.
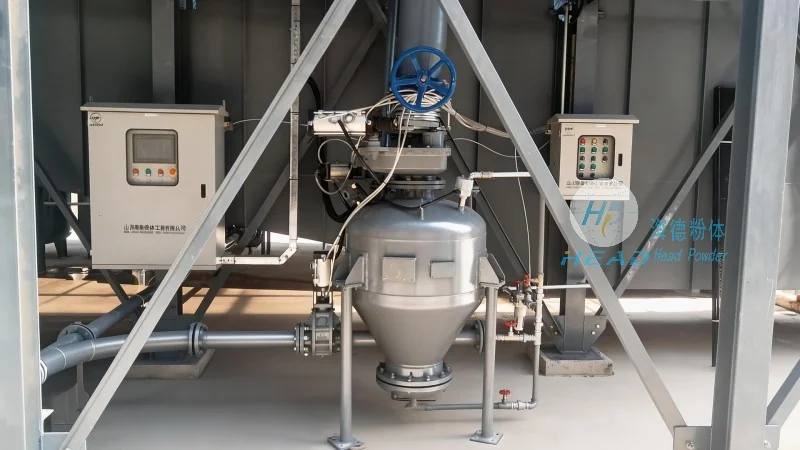
Technical Advantages and Operational Benefits
The pneumatic conveying systems developed by HeadPowder offer several advantages over conventional methods. These include reduced labor costs due to automated handling, improved safety by minimizing direct contact with the material, and enhanced product quality through controlled transport. The closed system design also helps in maintaining the integrity of the activated carbon, preventing contamination and ensuring consistent performance in downstream processes.
Customization and Scalability
Recognizing that each industrial application has unique demands, HeadPowder provides flexible and scalable solutions. Whether for small-scale laboratory use or large-scale industrial production, our systems can be adapted to accommodate varying flow rates and material volumes. The modular design allows for easy expansion or integration with existing infrastructure, ensuring a seamless transition for clients.
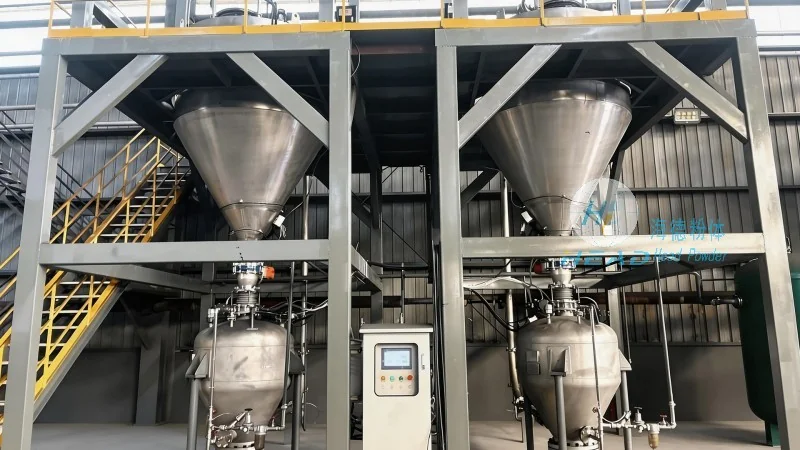
Quality Assurance and After-Sales Support
From initial design and manufacturing to on-site installation and commissioning, HeadPowder adheres to stringent quality standards. Our team of experienced engineers and technicians ensures that every component is tested rigorously to meet performance specifications. Post-installation, we provide comprehensive after-sales support, including maintenance services, technical assistance, and system optimization to ensure long-term operational efficiency and reliability.