

What is an Intelligent Tonne Bag Loading Station Material Pneumatic Conveying System? And What Are I
For industrial operations that require efficient handling of bulk materials, the intelligent tonne bag loading station with material pneumatic conveying system represents a sophisticated solution. This system is engineered to streamline the process of receiving, storing, and transporting bulk materials from large tonne bags into processing units, ensuring high efficiency and minimal downtime. The design principles behind such a system are rooted in optimizing material flow, maintaining product integrity, and enhancing operational safety.
Key Components and Functional Aspects
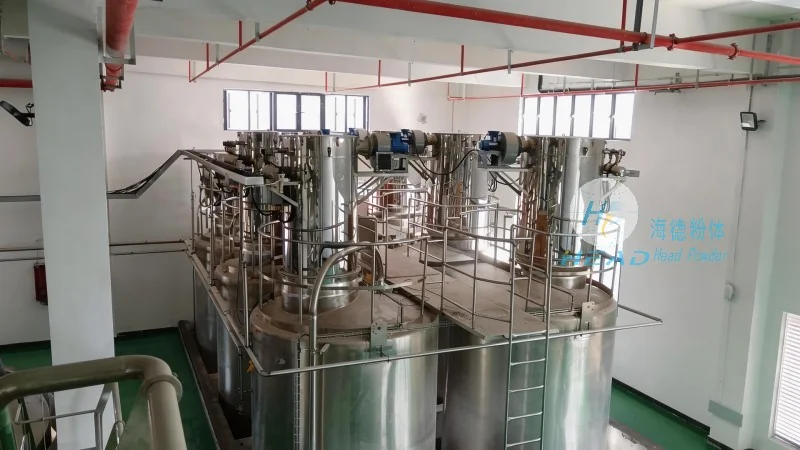
The intelligent tonne bag loading station typically integrates several core components that work in tandem to achieve seamless material handling. At the heart of the system is the pneumatic conveying equipment, which utilizes air pressure to move bulk materials from the tonne bags to the processing plant. This includes components like the hopper, which collects material from the bags, and the conveyor ducts that transport the material through the system. Additionally, the system may incorporate advanced sensors and control systems to monitor flow rates, pressure, and material levels in real-time, ensuring optimal performance and preventing operational issues.
Design Principles for Optimal Performance
The design of a material pneumatic conveying system for a tonne bag loading station is guided by several key principles aimed at maximizing efficiency and reliability. One of the primary principles is the selection of appropriate conveying technology based on the characteristics of the material being handled—such as particle size, moisture content, and bulk density. This ensures that the system can handle a wide range of materials without compromising performance. Another critical principle is the optimization of air flow and pressure to minimize energy consumption while maintaining sufficient material transport capacity. The system is also designed with considerations for material separation and cleaning, as well as the prevention of blockages and system downtime.
Advantages of the Intelligent Tonne Bag Loading Station
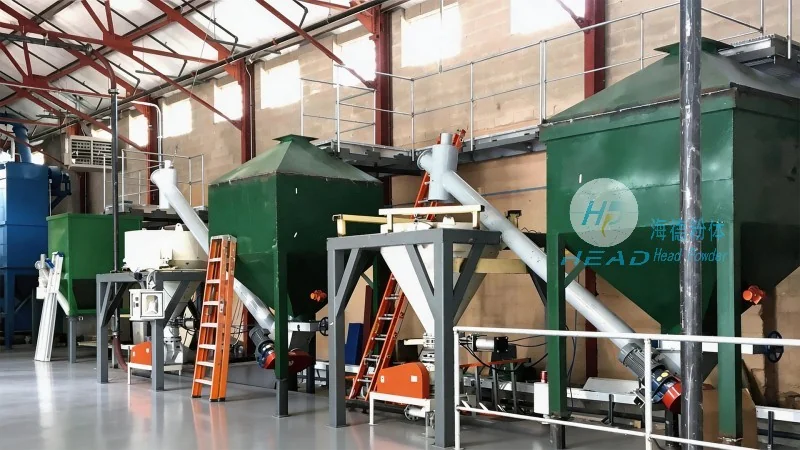
Implementing an intelligent tonne bag loading station with a pneumatic conveying system offers numerous advantages for industrial operations. Firstly, it significantly improves material handling efficiency by automating the process of loading and transporting bulk materials, reducing the need for manual labor and associated risks. Secondly, the system enhances product quality by minimizing material contamination and degradation during handling. Thirdly, it improves operational safety by eliminating the need for workers to handle heavy tonne bags and by controlling dust and air emissions. Additionally, the intelligent control systems provide real-time monitoring and data analysis, enabling operators to identify and address potential issues promptly, thereby reducing maintenance costs and increasing system uptime.
Application Scenarios and Industries
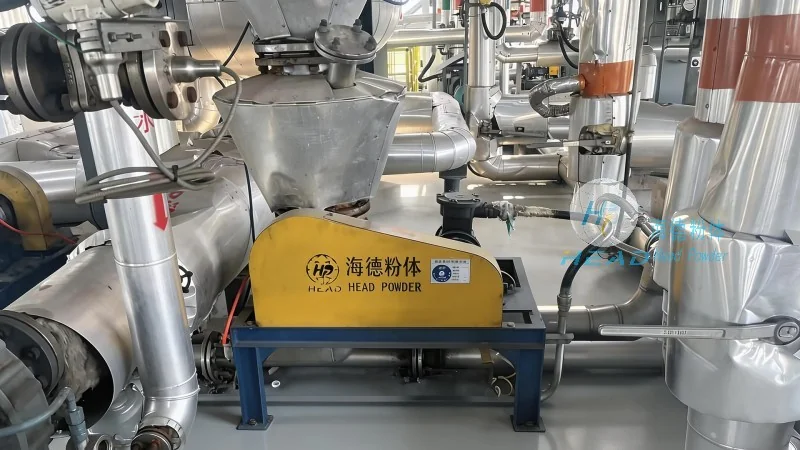
The intelligent tonne bag loading station material pneumatic conveying system is widely applicable across various industries that deal with bulk materials, including chemical, pharmaceutical, food, and mining sectors. In the chemical industry, for example, such systems are used to handle powders and granules, ensuring safe and efficient transport to reactors and processing units. In the pharmaceutical industry, the system's ability to maintain product purity and prevent contamination is crucial for meeting regulatory standards. Similarly, in the food industry, the system's hygienic design and ability to handle food-grade materials make it suitable for processing facilities. The mining industry also benefits from the system's robust design, which can handle abrasive and heavy materials without compromising performance.
Conclusion and Company Overview
Overall, the intelligent tonne bag loading station material pneumatic conveying system is a critical component in modern industrial material handling, offering enhanced efficiency, safety, and product quality. The design principles behind this system, including optimized material flow, advanced control systems, and robust construction, ensure that it can meet the demands of various industrial applications. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems, leveraging years of experience to deliver solutions tailored to the specific needs of industrial clients. With a focus on innovation and quality, the company continues to advance the technology of material handling systems, supporting the growth and efficiency of industrial operations worldwide.