

Working Principle and Characteristics of Mine Pneumatic Conveying
HeadPowder, a leading provider in the field of pneumatic conveying systems, specializes in delivering efficient and reliable solutions for material handling in mining operations. With a strong presence in Shandong, China, the company has established itself as a trusted partner for businesses seeking advanced technology in mine material transport. This article explores the fundamental working principle and key characteristics of mine pneumatic conveying, highlighting how these systems enhance operational efficiency and safety in industrial settings.
Working Principle of Mine Pneumatic Conveying
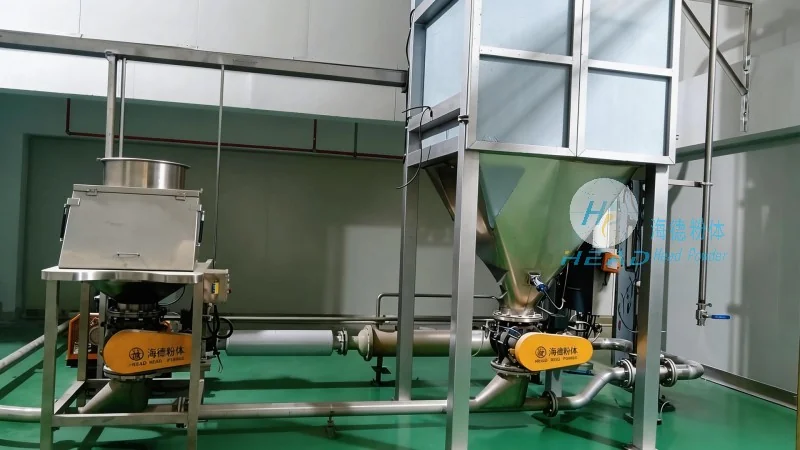
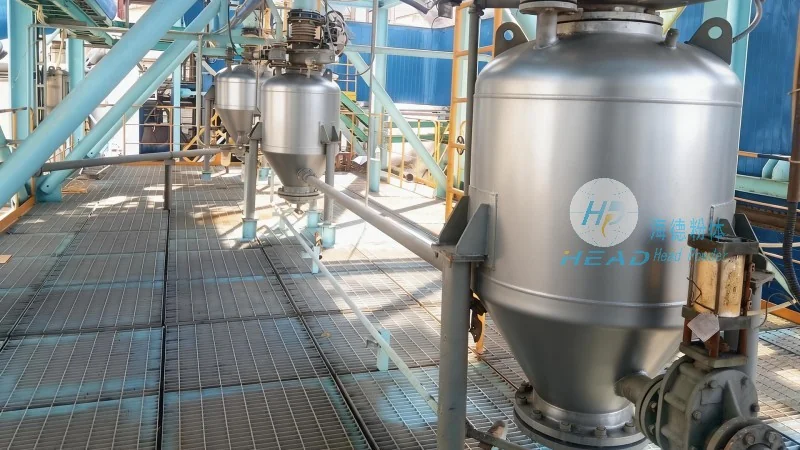
Mine pneumatic conveying operates on the principle of transporting bulk materials through a pipeline using a gas stream, typically air or other gases. The process involves several key components and steps that ensure smooth material movement from the source to the destination. First, the material is introduced into the system, often through a hopper or feeder, where it is then mixed with the conveying medium. The gas stream, generated by a blower or compressor, creates a pressure differential that propels the material along the pipeline. As the material travels, it is suspended and carried by the gas flow, allowing for continuous and unobstructed transport. The system typically includes a series of pipelines, bends, and control valves that regulate the flow and direction of both the material and the gas. At the receiving end, the material is separated from the gas through a separator or cyclone, and the gas is either recirculated or vented, depending on the system design. This method eliminates the need for mechanical components like belts or buckets, reducing wear and maintenance costs while improving safety by minimizing direct human contact with the material.
Key Characteristics of Mine Pneumatic Conveying Systems
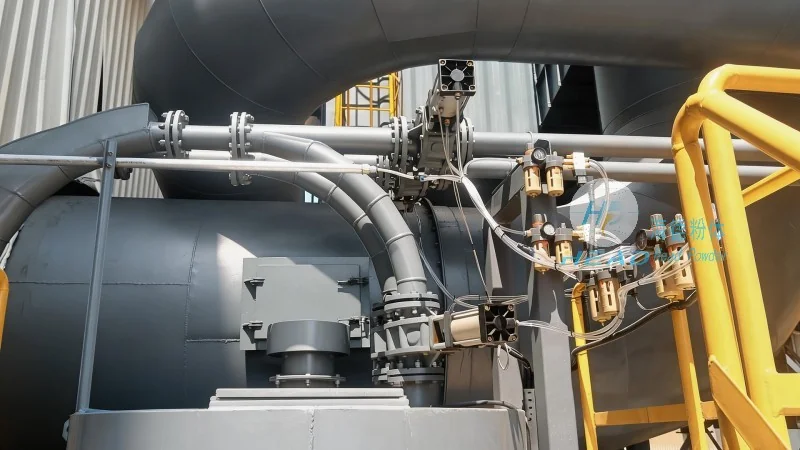
HeadPowder's mine pneumatic conveying systems are designed with several distinct characteristics that make them ideal for demanding mining environments. One of the primary features is their ability to handle a wide range of materials, from fine powders to large granules, with consistent performance. The systems are also highly flexible, allowing for changes in material type or flow rate without significant modifications. Another important characteristic is the low maintenance requirement, as the absence of moving parts reduces the risk of breakdowns and extends the service life of the equipment. Additionally, these systems offer excellent dust control, which is crucial for maintaining a safe and healthy work environment in mines. The compact design of the equipment also contributes to space efficiency, making it suitable for both new and existing mining facilities. Furthermore, the systems are equipped with advanced control systems that allow for real-time monitoring and adjustment, ensuring optimal performance and minimizing downtime. These characteristics collectively contribute to increased productivity, reduced operational costs, and enhanced safety in mine operations.
Advantages and Applications in Mining
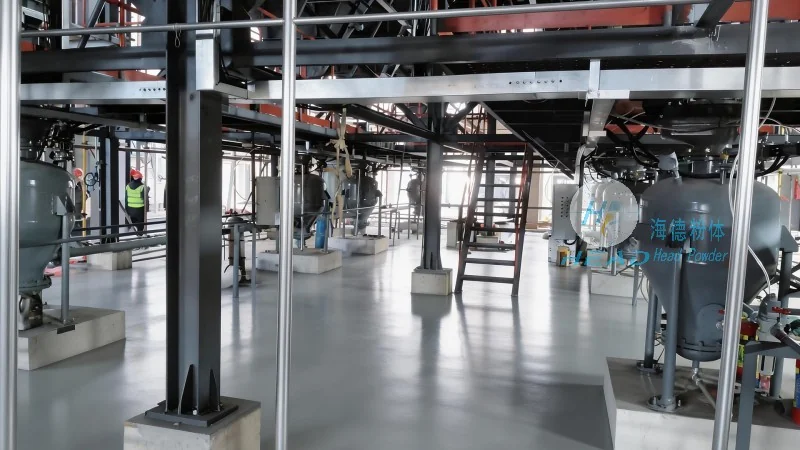
The application of mine pneumatic conveying systems brings numerous advantages to mining operations. By eliminating the need for traditional conveyor belts or bucket elevators, these systems reduce the risk of material spillage and contamination, which is particularly important for handling hazardous or valuable materials. The systems also improve operational efficiency by enabling continuous material flow, which can lead to higher throughput and reduced production delays. Another significant advantage is the improved safety aspect, as the enclosed pipeline system minimizes exposure to dust and fumes, reducing the risk of respiratory illnesses and other health hazards. The systems are widely used in various mining applications, including the transport of coal, ore, and other bulk materials from mines to processing plants or storage facilities. They are also suitable for handling materials in underground mines, where space is limited and the need for safe, efficient transport is critical. Overall, mine pneumatic conveying systems offer a reliable and cost-effective solution for modern mining operations, aligning with the industry's demand for advanced technology and sustainable practices.